

[WTTLE]Working Principle and Characteristics of Beer Brewery Pellet Conveying
Beer brewery pellet conveying is a critical process in the production and management of by-products from brewing operations. The efficient handling of spent grain, also known as beer brewery pellet, is essential for maintaining operational efficiency and sustainability in modern breweries. This article explores the working principle and key characteristics of the pellet conveying systems used in such applications, with a focus on the expertise of Shandong HeadPowder Engineering Co., Ltd., a leading provider in this field based in Shandong, China.
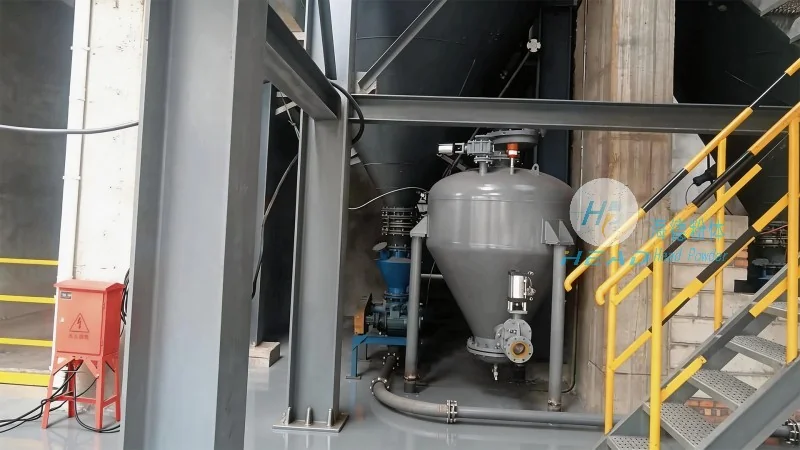
Company Background and Expertise
Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and implementation of advanced material handling solutions for various industries, including the brewing sector. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for breweries seeking reliable and efficient pellet conveying systems. HeadPowder's team of engineers and technicians possesses extensive experience in understanding the unique challenges of handling beer brewery pellet, ensuring that their solutions are tailored to meet the specific needs of each client. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art research and development center dedicated to improving material handling technologies.
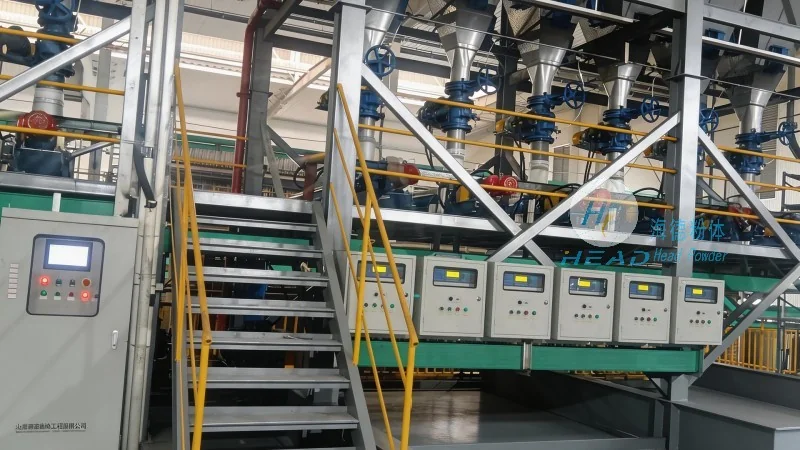
The Working Principle of Beer Brewery Pellet Conveying
The core of beer brewery pellet conveying systems lies in the integration of several mechanical components that work in tandem to transport the material from one location to another. Typically, these systems employ a combination of conveyor types, such as screw conveyors, pneumatic conveyors, or belt conveyors, depending on the specific requirements of the brewery. The working principle involves the initial collection of spent grain from the brewing process, followed by processing to achieve the desired pellet form. Once processed, the pellets are fed into the conveying system, where they are moved through a series of components including feed hoppers, conveyors, and discharge points. The system is designed to maintain consistent flow rates and minimize material degradation, ensuring that the pellets are transported safely and efficiently. For example, in pneumatic conveying systems, air is used to create a pressure differential that propels the pellets through a pipeline, while screw conveyors utilize rotating screws to push the material forward. The choice of conveying method depends on factors such as the material's moisture content, bulk density, and the distance to be covered. HeadPowder's engineers carefully select the most appropriate technology for each project, considering these variables to optimize performance and reduce operational costs.
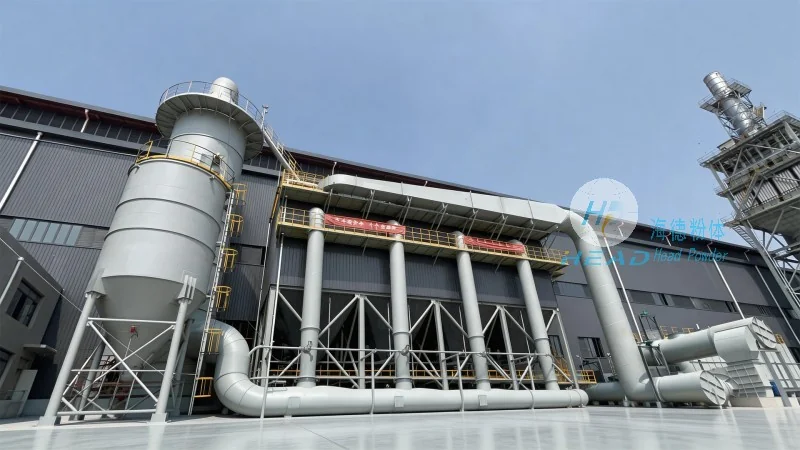
Key Characteristics of Beer Brewery Pellet Conveying Systems
Beer brewery pellet conveying systems exhibit several notable characteristics that distinguish them from other material handling solutions. One of the primary characteristics is their ability to handle abrasive and high-volume materials without significant wear and tear on the equipment. The systems are constructed with durable materials, such as stainless steel or high-grade alloys, to withstand the harsh conditions associated with spent grain. Additionally, these systems are designed for high efficiency, with minimal energy consumption and low maintenance requirements. The integration of advanced control systems allows for precise regulation of flow rates and operational parameters, ensuring consistent performance over time. Another key characteristic is the flexibility of the conveying systems, which can be adapted to different production scales and layouts. Whether a small-scale brewery or a large industrial facility, HeadPowder can provide customized solutions that fit the specific needs of the client. The systems also prioritize safety, incorporating features such as emergency stop mechanisms and dust suppression systems to protect both the equipment and personnel. Furthermore, the design of these systems promotes hygiene and compliance with industry standards, which is crucial for maintaining the quality of the final product and meeting regulatory requirements. The combination of these characteristics makes beer brewery pellet conveying systems an essential component of modern brewing operations, enabling breweries to optimize their processes and reduce waste.
Benefits of Implementing Advanced Pellet Conveying Solutions
Adopting advanced beer brewery pellet conveying solutions offers numerous benefits to breweries. Firstly, it enhances operational efficiency by reducing the time and labor required for material handling. By automating the process, breweries can allocate their resources to other critical tasks, such as production and quality control. Secondly, these systems improve product quality by minimizing material degradation and contamination. The consistent flow and controlled environment prevent the pellets from becoming compacted or damaged, which can affect their nutritional value and usability. Thirdly, the use of advanced conveying systems contributes to sustainability by reducing waste and improving resource utilization. By efficiently handling spent grain, breweries can reduce the amount of waste sent to landfills and potentially repurpose the material for other applications, such as animal feed or biofuel production. Additionally, the energy-efficient design of these systems helps lower operational costs and environmental impact. HeadPowder's solutions are designed to maximize these benefits, providing clients with a reliable and cost-effective approach to pellet conveying. The company's expertise in material handling ensures that each system is optimized for the specific brewery's needs, resulting in long-term performance and satisfaction.
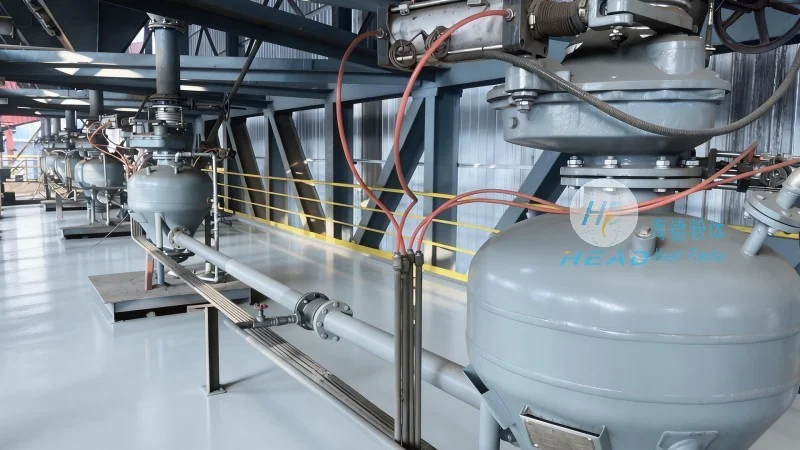
Conclusion and Future Trends
In conclusion, beer brewery pellet conveying systems play a vital role in the efficient and sustainable operation of breweries. The working principle, which involves the integration of various mechanical components, ensures that spent grain is transported safely and efficiently. The key characteristics of these systems, including durability, efficiency, flexibility, and safety, make them an ideal choice for breweries of all sizes. By implementing advanced pellet conveying solutions, breweries can enhance their operational efficiency, improve product quality, and contribute to sustainability. Shandong HeadPowder Engineering Co., Ltd. stands as a leading provider in this field, offering customized solutions that meet the unique needs of each client. As the brewing industry continues to evolve, the demand for advanced material handling technologies will likely increase, and companies like HeadPowder will remain at the forefront of innovation, providing the solutions necessary to meet these challenges.