

Working Principle and Features of Sodium Dithionite Material Pneumatic Conveyor
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for handling sodium dithionite material. This article delves into the working principle and key features of their specialized pneumatic conveyor, providing insights into its operational efficiency and practical applications.
Working Principle of the Pneumatic Conveyor
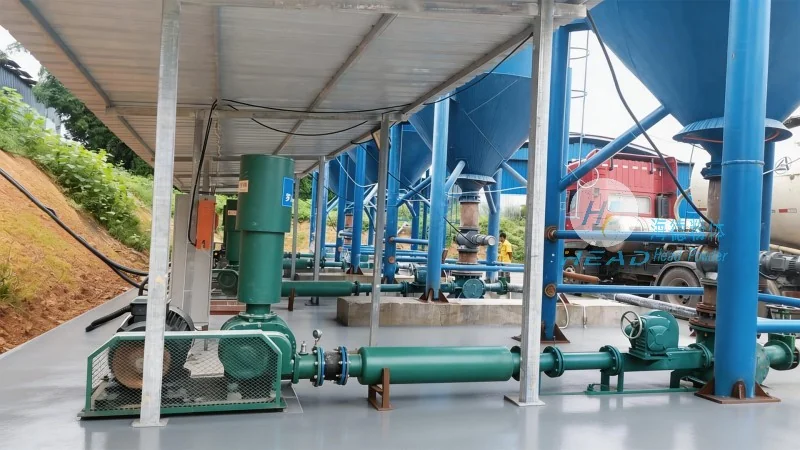
The pneumatic conveyor for sodium dithionite material operates on the principle of air flow to transport bulk material. At its core, the system utilizes a combination of positive and negative pressure or vacuum to move the material from the source to the destination. The process typically involves several key components: a feeding hopper, a conveyor line (often a flexible hose or rigid pipe), a blower or fan to generate airflow, and a control system to regulate the flow rate. The material is fed into the conveyor line, where it is entrained by the high-velocity air stream. This air-material mixture is then transported through the pipeline to the discharge point. The system may include additional features such as filters to remove dust, pressure relief valves for safety, and sensors to monitor the flow and pressure, ensuring smooth and reliable operation.
Key Features and Advantages
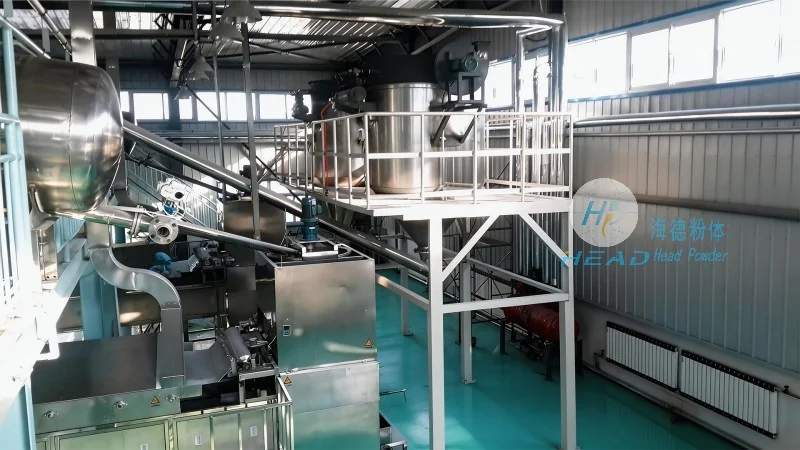
HeadPowder's pneumatic conveyor for sodium dithionite material is engineered with several distinct features that enhance its performance and suitability for industrial applications. One of the primary advantages is its ability to handle the material's characteristics, such as its hygroscopic nature and potential for dust generation, with minimal degradation. The system is designed to maintain the material's quality by controlling moisture and preventing contamination during transport. Additionally, the conveyor offers high efficiency in terms of material throughput, with the ability to transport large volumes of sodium dithionite over considerable distances without the need for intermediate storage or handling. The design also emphasizes safety, incorporating features like overpressure protection and emergency shut-off mechanisms to prevent accidents. Another notable feature is the flexibility in system configuration, allowing customization based on the specific requirements of the application, including different pipe sizes, material feed rates, and discharge options. The system's compact footprint and ease of integration into existing production lines make it a practical choice for various industrial settings.
Application-Specific Benefits
The pneumatic conveyor is particularly well-suited for industries that rely on sodium dithionite as a key chemical, such as the textile, paper, and food processing sectors. In these applications, the conveyor ensures a continuous and controlled supply of the material, reducing downtime and improving production efficiency. The system's ability to handle the material's sensitivity to moisture and air exposure is crucial, as it helps maintain the material's reactivity and effectiveness. Furthermore, the conveyor's low maintenance requirements and long service life contribute to cost savings over time. The system's design also allows for easy cleaning and maintenance, which is essential for maintaining hygiene standards in industries like food processing. The reliability of the pneumatic conveyor in handling bulk materials without the need for mechanical contact reduces wear and tear on the material, preserving its quality and extending its shelf life.
Conclusion
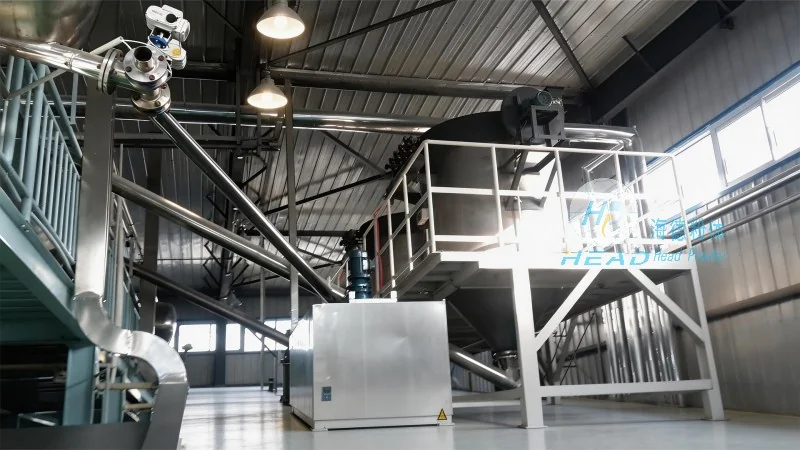
HeadPowder's pneumatic conveyor for sodium dithionite material represents a sophisticated solution for efficient and safe material handling in industrial settings. By leveraging advanced pneumatic technology, the system combines operational efficiency with robust features that address the unique challenges of handling sodium dithionite. With its ability to maintain material quality, ensure high throughput, and provide flexible customization options, this conveyor is an ideal choice for businesses seeking reliable and cost-effective solutions for transporting sodium dithionite. Based in Shandong, China, HeadPowder continues to innovate in the field of material handling equipment, delivering products that meet the evolving needs of modern industry.