

Principle and Working Scene Characteristics of Rare Earth Crystal Powder Pneumatic Conveying Lines
Rare earth crystal powders are critical components in modern industrial applications, and efficient material handling is essential for maintaining production efficiency and product quality. Pneumatic conveying lines offer a sophisticated solution for transporting these fine powders, leveraging air pressure to move materials through a network of pipes and equipment. This article explores the fundamental principles behind rare earth crystal powder pneumatic conveying systems, as well as the key working scene characteristics that define their effectiveness in industrial settings.
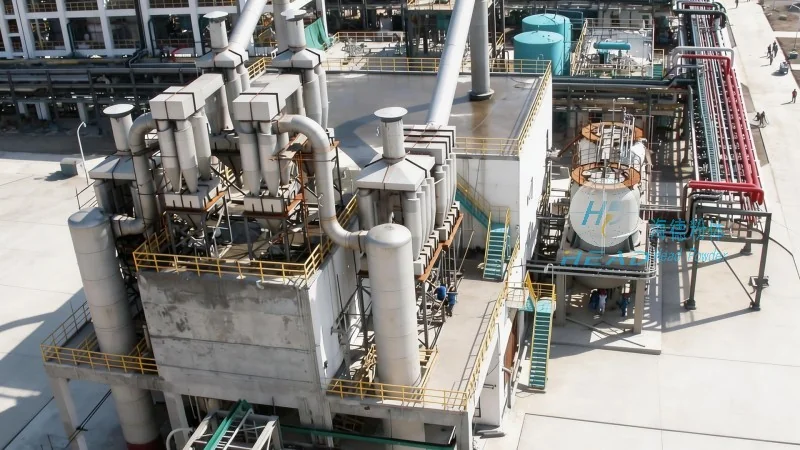
The Core Principle of Pneumatic Conveying for Rare Earth Powders
The principle of pneumatic conveying involves using compressed air to create a flow that transports particulate materials through a closed system. For rare earth crystal powders, which are often sensitive to moisture and contamination, the design of the conveying line must prioritize cleanliness and control. The system typically consists of a material feed hopper, a pressure or vacuum pump, and a series of pipes that guide the powder from the source to the destination. The air flow is carefully regulated to ensure that the powder particles are suspended and moved without causing blockages or degradation. This method is particularly advantageous for rare earth powders due to their fine particle size and potential for agglomeration, as the air flow helps to break up clumps and maintain a consistent flow rate.
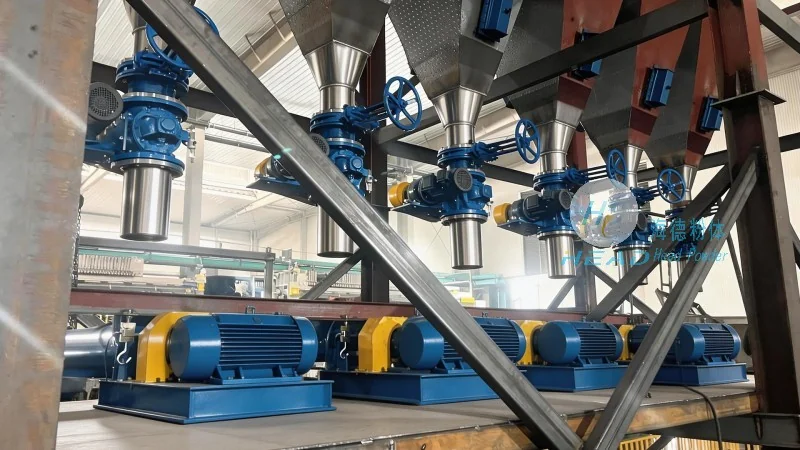
Key Working Scene Characteristics of Rare Earth Crystal Powder Conveying Lines
The effectiveness of a rare earth crystal powder pneumatic conveying line is determined by several key characteristics that are tailored to the specific demands of industrial applications. These include:
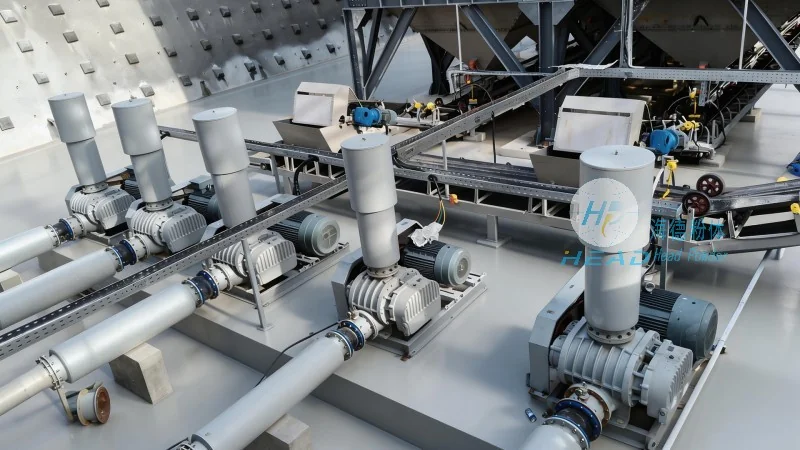
- Material Handling Efficiency: The system must be capable of handling high volumes of fine powders with minimal loss or degradation. This is achieved through optimized air velocity and pipe diameter, ensuring that the powder particles remain suspended and transported smoothly.
- Contamination Control: Given the high purity requirements of rare earth crystals, the conveying line must be designed to prevent cross-contamination and exposure to external elements. This involves using sealed systems, high-quality filters, and materials that do not react with the powder.
- Energy Efficiency: Modern pneumatic conveying systems are designed to minimize energy consumption while maintaining performance. This is achieved through efficient pump selection, optimized pipe layout, and the use of variable speed drives to adjust air flow as needed.
- Flexibility and Scalability: The system should be adaptable to different production scales and can be expanded or reconfigured as production needs change. This includes the ability to integrate with existing equipment and processes without significant disruption.
Application Scenarios in Industrial Settings
Rare earth crystal powder pneumatic conveying lines are widely used in various industrial sectors, including:
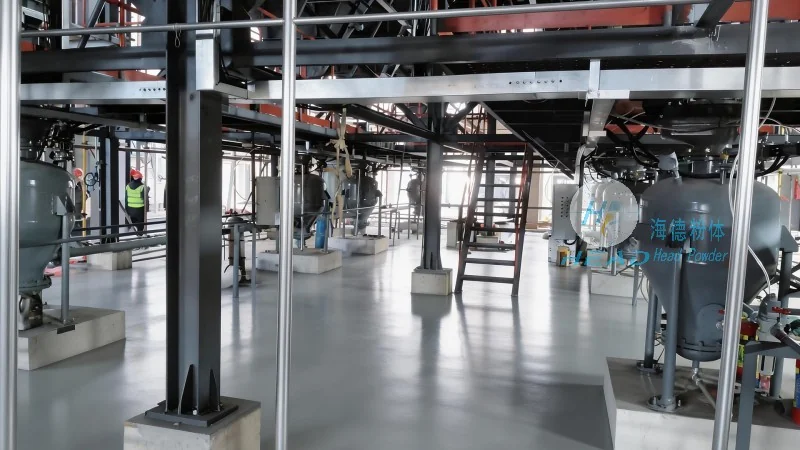
- Electronics Manufacturing: In the production of rare earth magnets and other electronic components, precise handling of fine powders is critical to ensure the quality and performance of the final products. The conveying line helps to deliver the powder to mixing and compounding equipment with minimal variability.
- Pharmaceutical and Chemical Industries: For applications involving rare earth-based catalysts or additives, the conveying line must meet stringent regulatory requirements for purity and contamination control. The sealed system and filtration capabilities of the line ensure compliance with industry standards.
- Energy and Renewable Technologies: In the production of rare earth-based batteries and solar panels, the efficient transport of powders is essential for maintaining production throughput and reducing downtime. The system's ability to handle high volumes and maintain consistent flow rates supports continuous production processes.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of specialized material handling solutions for rare earth and other fine powders. With a focus on innovation and customer-centric design, the company develops and manufactures pneumatic conveying systems tailored to the unique challenges of handling sensitive materials. Headpowder's expertise lies in creating customized solutions that balance efficiency, purity, and reliability, ensuring that clients can meet their production goals while maintaining the highest standards of material quality. The company's facilities are located in Shandong, China, where it leverages local manufacturing capabilities and industry expertise to deliver superior products and services to global markets.