

Principle and Working Scene Characteristics of Ammonium Bicarbonate Material Conveying Lines
Ammonium bicarbonate, a critical chemical compound widely utilized in the fertilizer and chemical sectors, demands specialized material handling solutions to facilitate efficient production processes. The material conveying line, engineered by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer headquartered in Shandong, China, is specifically designed to address the unique challenges associated with transporting this substance. This article delves into the fundamental principles of such conveying systems and highlights the key characteristics of their operational environments.
Understanding the Material Conveying Line Principle
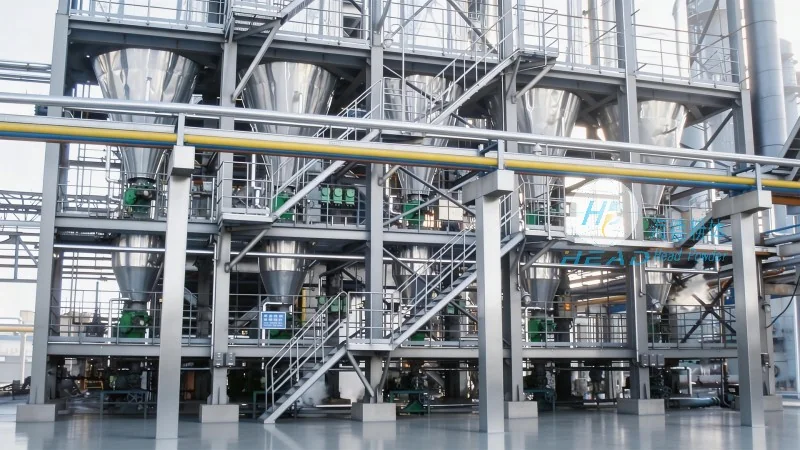
The core principle of an ammonium bicarbonate material conveying line centers on the efficient and safe movement of the material from its source to the processing or storage destination. Shandong HeadPowder Engineering Co., Ltd. develops these systems to integrate seamlessly with existing production workflows, ensuring minimal downtime and maximizing productivity. The system typically comprises several critical components, including feeders, conveyors, control panels, and safety mechanisms. Feeders are responsible for uniformly feeding the ammonium bicarbonate into the conveyor, while the conveyor itself transports the material through a series of stages. Control systems monitor and regulate the flow rate, ensuring consistent performance. Safety features, such as dust suppression and overfill protection, are integrated to prevent accidents and maintain compliance with industrial standards.
Key Working Scene Characteristics
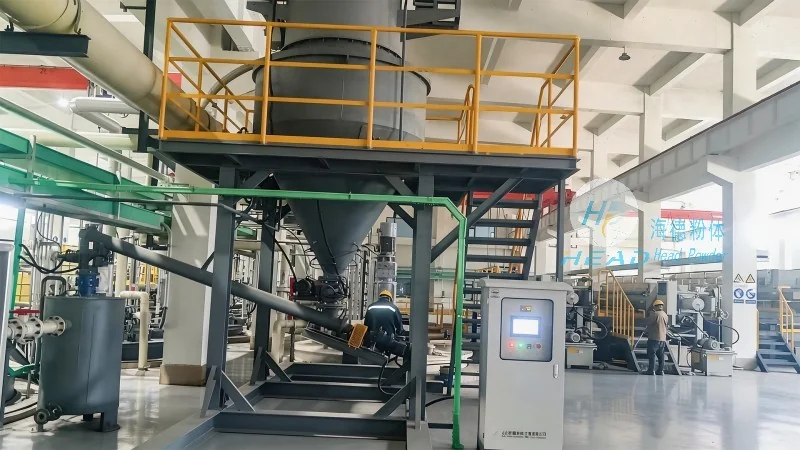
The operational characteristics of the ammonium bicarbonate material conveying line are closely tied to the specific industrial applications and environmental conditions. In fertilizer manufacturing facilities, for example, the line must handle large volumes of the material while maintaining product purity. The design of the conveying system considers factors like temperature control, as ammonium bicarbonate can be sensitive to heat, and dust suppression, as the material is fine and can create airborne particles. The working environment may also involve high humidity or exposure to other chemicals, requiring the equipment to be constructed from corrosion-resistant materials. Additionally, the line is often integrated with other production equipment, such as reactors or mixers, necessitating precise synchronization to avoid interruptions in the production cycle.
Advantages and Practical Applications
The ammonium bicarbonate material conveying line offers several advantages that make it a preferred choice for industrial applications. Firstly, it provides a continuous and automated method of material transport, reducing the need for manual handling and associated risks. This not only enhances safety but also improves operational efficiency. Secondly, the system is designed to minimize material loss and contamination, which is crucial for maintaining product quality in sensitive industries like fertilizer production. The flexibility of the conveying line allows it to adapt to varying production demands, whether it's a steady flow or intermittent batches. Shandong HeadPowder Engineering Co., Ltd. tailors each system to meet the specific needs of their clients, ensuring optimal performance and reliability.
Conclusion
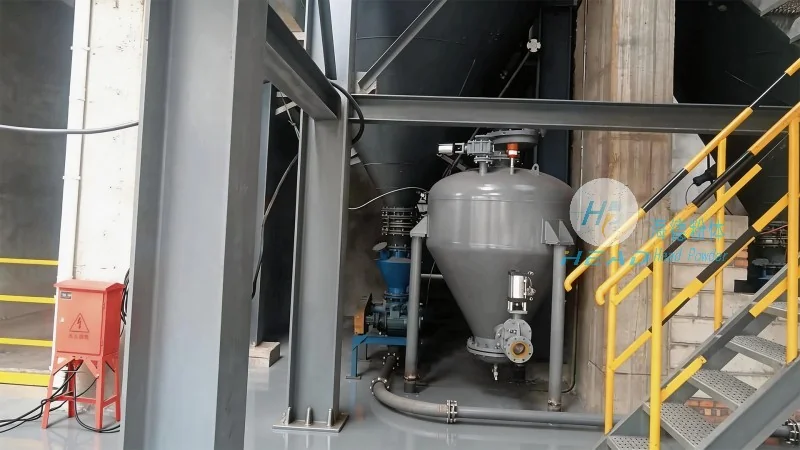
In summary, the ammonium bicarbonate material conveying line, as designed by Shandong HeadPowder Engineering Co., Ltd., is a sophisticated solution that combines advanced engineering principles with practical operational considerations. By understanding the material's properties and the specific requirements of the working environment, the system ensures efficient, safe, and reliable transport of ammonium bicarbonate. This contributes to improved productivity and product quality in the chemical and fertilizer industries, making it an essential component of modern industrial operations.