

Principles and Working Scene Characteristics of Desulfurization Fly Ash Material Handling System Equ
The desulfurization fly ash material handling system equipment is a critical component in modern industrial processes, particularly in power plants and chemical facilities. HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in providing efficient and reliable solutions for transporting fly ash generated during flue gas desulfurization. This article explores the underlying principles of these systems and highlights the key characteristics of their operational environments.
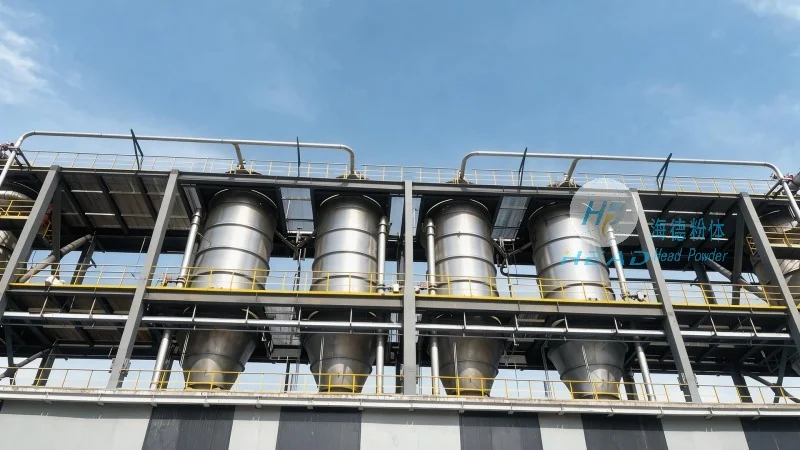
Principles of Desulfurization Fly Ash Material Handling Systems
The core principle of desulfurization fly ash material handling systems revolves around the efficient transport of fine, dry, or slightly moist fly ash from the desulfurization unit to storage or disposal sites. The equipment typically includes components such as conveyor belts, screw conveyors, pneumatic conveying systems, and hopper structures. These systems are designed to handle the unique properties of fly ash, which often includes high moisture content, abrasive particles, and potential agglomeration. The mechanical design ensures minimal material loss, low maintenance requirements, and compliance with environmental regulations. For instance, HeadPowder’s systems utilize advanced material handling technologies to maintain consistent flow rates and prevent blockages, which are common challenges in fly ash transport.
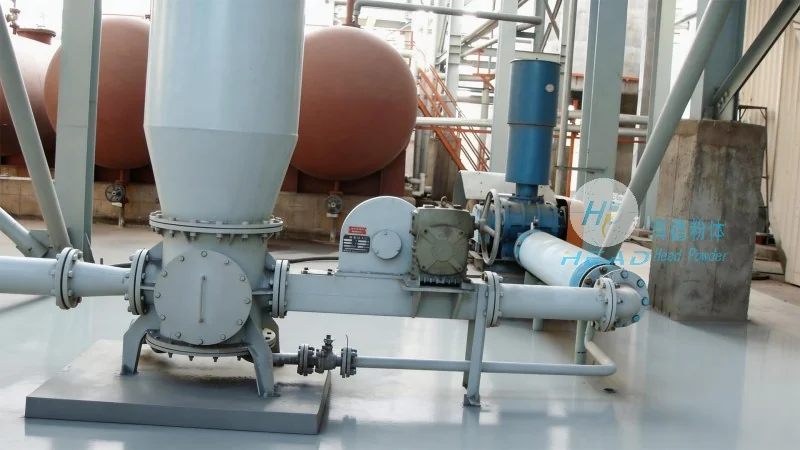
Working Scene Characteristics of Desulfurization Fly Ash Handling Equipment
The operational environments for desulfurization fly ash material handling systems vary significantly based on the industrial application. In thermal power plants, the system must handle large volumes of fly ash generated from coal combustion, often at high temperatures and under continuous operation. The equipment is engineered to withstand high temperatures and corrosive conditions, ensuring durability and longevity. In contrast, in chemical processing facilities, the fly ash may have different chemical compositions, requiring specialized materials for the conveyor components to prevent wear and tear. The working scene characteristics also include the need for integration with existing plant infrastructure, ensuring seamless operation without disrupting the main production processes. HeadPowder’s solutions are tailored to these diverse scenarios, offering customized designs that meet specific site requirements and operational constraints.
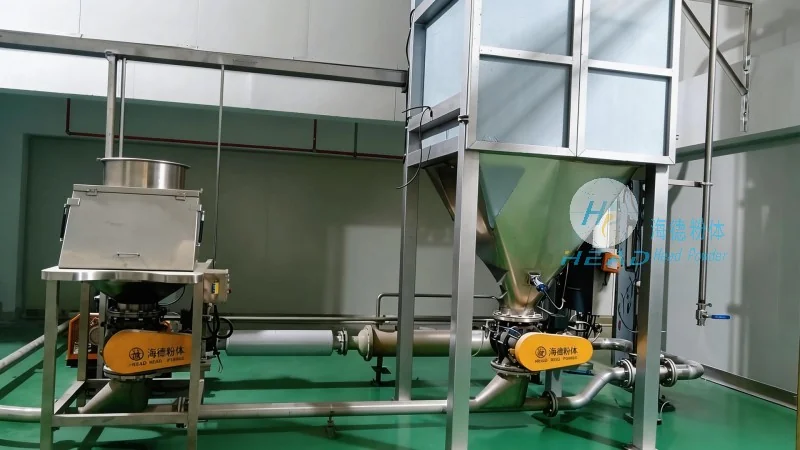
Key Features and Advantages of HeadPowder’s Systems
The effectiveness of desulfurization fly ash material handling systems is enhanced by several key features. First, the systems are designed with energy efficiency in mind, reducing operational costs while minimizing environmental impact. Advanced control systems allow for real-time monitoring of flow rates and system performance, enabling quick adjustments to maintain optimal operation. Second, the equipment is built for durability, using high-quality materials that resist abrasion and corrosion, which are common issues with fly ash particles. This longevity reduces the need for frequent replacements and maintenance, contributing to overall cost savings. Third, the systems are designed for safety, incorporating features such as emergency stop mechanisms and dust suppression systems to protect both personnel and the environment. These features align with global safety standards and regulatory requirements, ensuring compliance in various jurisdictions.
Real-World Applications and Case Studies
In practical applications, HeadPowder’s desulfurization fly ash material handling systems have been successfully implemented in numerous power plants and industrial facilities across China. For example, a large thermal power plant in Shandong utilized HeadPowder’s conveyor system to transport fly ash from the desulfurization unit to a storage silo. The system demonstrated high efficiency in handling large volumes of fly ash, with minimal downtime and low maintenance costs. Another case involved a chemical processing plant where the system was adapted to handle fly ash with higher moisture content, utilizing a combination of screw and pneumatic conveying components to achieve consistent flow. These real-world applications highlight the versatility and reliability of HeadPowder’s solutions in diverse operational environments.
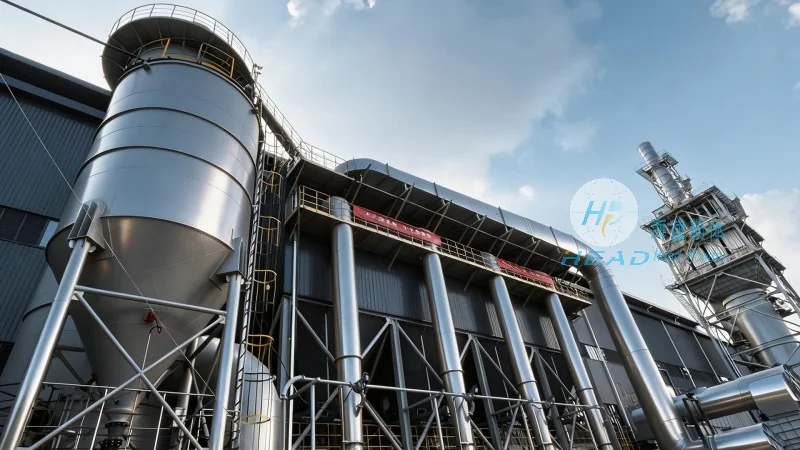
Conclusion: Tailored Solutions for Fly Ash Handling
In conclusion, the desulfurization fly ash material handling system equipment from HeadPowder Engineering Co., Ltd. combines advanced engineering principles with practical application knowledge to deliver efficient and reliable solutions. The systems are designed to address the unique challenges of fly ash transport, including material properties, operational conditions, and environmental regulations. By focusing on durability, energy efficiency, and safety, HeadPowder’s products ensure long-term performance and cost-effectiveness for industrial clients. The company’s commitment to tailored solutions and adherence to industry standards makes it a trusted partner for facilities seeking to optimize their fly ash handling processes.