

Principle and Working Scene Characteristics of Wood Chip Material Handling System Equipment
Shandong HeadPowder Engineering Co., Ltd., a prominent engineering firm headquartered in Shandong, China, specializes in the design and manufacturing of advanced wood chip material handling systems. These systems are engineered to efficiently transport wood chips, sawdust, and other wood processing byproducts, ensuring optimal performance in diverse industrial settings. The company's commitment to innovation and quality has positioned it as a leading provider in the wood processing industry, with systems that meet the demands of modern manufacturing processes.
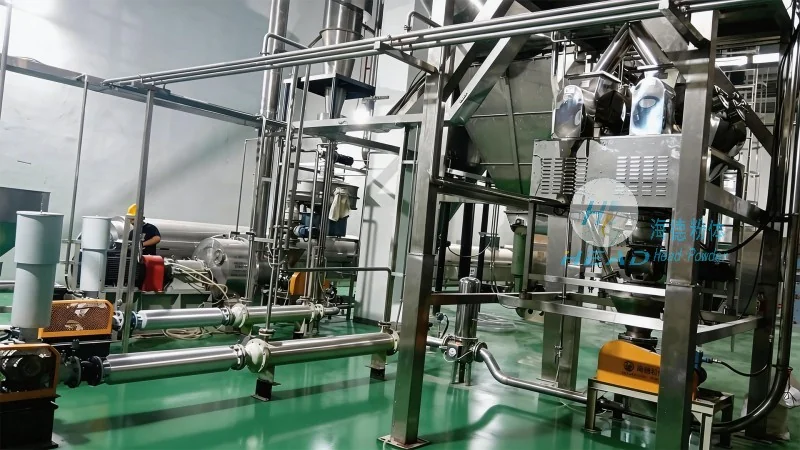
Principle of Operation for Wood Chip Material Handling Equipment
The wood chip material handling system operates on a sophisticated combination of mechanical and pneumatic principles, utilizing conveyor belts, screw conveyors, and air transport mechanisms. The process begins with the intake of raw wood chips, which are fed into the system via a hopper or intake chute. The initial stage involves size reduction and sorting, where larger or non-compliant chips are separated and redirected for further processing. The conveyor belts, typically made of rubber or reinforced plastic, are designed to handle the abrasive nature of wood chips, with smooth surfaces to minimize friction and wear. The screw conveyors, or augers, provide a continuous, low-maintenance method of moving materials horizontally or vertically, with variable speed controls to adjust the flow rate based on production needs. Pneumatic transport systems are integrated for long-distance or high-precision transport, where air pressure is used to move fine wood particles through pipes or ducts. The control system, equipped with sensors and programmable logic controllers (PLCs), monitors critical parameters such as flow rate, pressure, and temperature, ensuring consistent performance and preventing equipment damage. This integrated approach ensures that the system operates efficiently and reliably, even under high-volume production conditions.
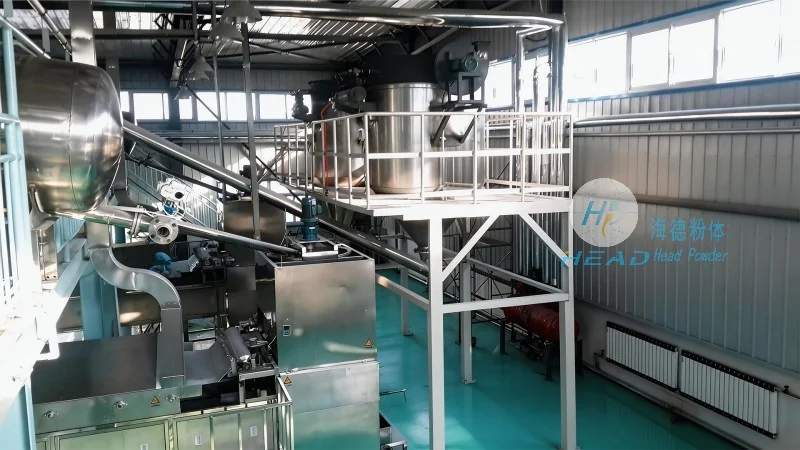
Key Working Scene Characteristics
The working scene characteristics of wood chip material handling systems are tailored to the specific requirements of wood processing facilities, adapting to different production stages and environmental conditions. In sawmills, the systems operate in high-volume environments where continuous material flow is essential for maintaining production efficiency. The compact design of some models allows for installation in confined spaces, such as between cutting machines and storage areas, while others are built for heavy-duty industrial applications with high throughput capabilities. Environmental considerations, such as dust control and noise reduction, are integrated into the design to comply with industrial safety standards and maintain a clean working environment. The systems are also designed to handle varying chip sizes and moisture content, ensuring consistent performance regardless of raw material variations. For example, in a wood pellet plant, the system must feed raw wood chips to the pelletizer with precise control, while in a biomass energy facility, it needs to transport wood chips to the combustion unit with minimal loss. The adaptability of these systems makes them suitable for a wide range of applications, from small-scale wood processing operations to large industrial facilities.
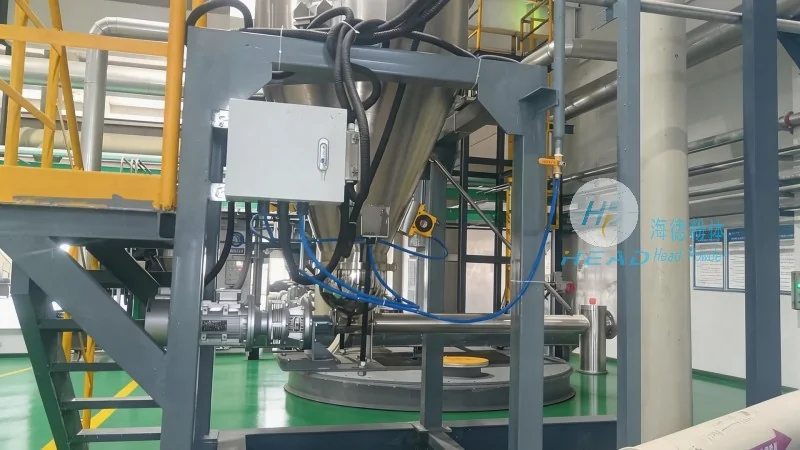
Application Scenarios and Industry Integration
Wood chip material handling systems are widely utilized in various wood processing applications, including sawmills, wood pellet production plants, and biomass energy facilities. In sawmills, the systems are critical for transporting sawdust and wood chips from cutting operations to storage or further processing, where they may be used as fuel or raw material for other products. The systems are designed to handle large volumes of material, often processing several tons per hour, and are integrated with the sawmill's production line to ensure a continuous supply of chips. In wood pellet plants, the focus is on precise and consistent feeding to the pelletizing machinery, where the quality of the input material directly impacts the final product's quality. The systems are equipped with sensors that monitor the moisture content and particle size of the wood chips, adjusting the feed rate to maintain optimal conditions. In biomass energy facilities, the systems transport wood chips to combustion or gasification units, where they are used as a renewable energy source. The integration of these systems with the overall production process ensures that the energy generation is efficient and sustainable. Additionally, the systems are used in recycling centers and waste management facilities, where wood waste is processed into reusable materials, contributing to environmental sustainability.
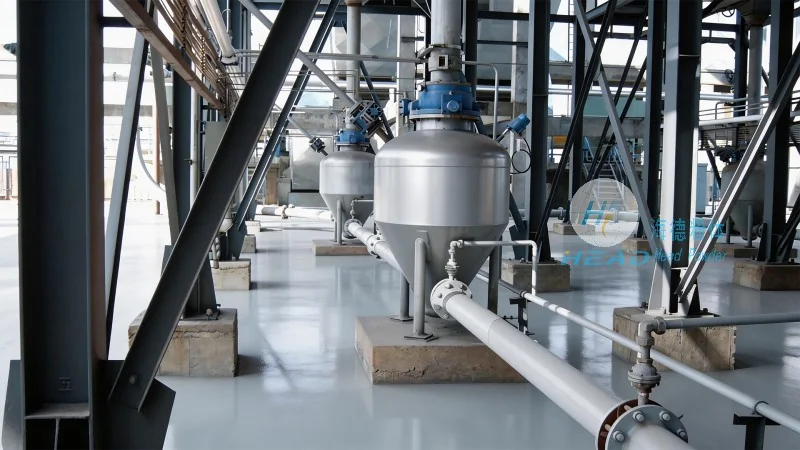
Advantages and Technical Specifications
Shandong HeadPowder Engineering Co., Ltd.'s wood chip material handling systems offer several key advantages, including high efficiency, low maintenance costs, and durability. The systems are constructed using high-quality materials, such as stainless steel and heavy-duty plastics, which resist corrosion and wear from wood chips, ensuring long service life. The modular design allows for easy installation and maintenance, with components that can be replaced without disrupting the entire system. Technical specifications vary based on the model, but common features include adjustable speed controls, overload protection, and emergency stop functions. The systems are also equipped with safety features, such as guards and interlocks, to prevent accidents and ensure operator safety. The integration of advanced sensors and monitoring systems provides real-time data on system performance, enabling predictive maintenance and reducing downtime. For instance, the PLC-based control system can detect a blockage in the conveyor and automatically shut down the system to prevent damage, while also alerting maintenance personnel. The systems are designed to meet international safety and environmental standards, making them suitable for global markets. The company's commitment to quality and customer satisfaction is reflected in the robust design and reliable performance of its wood chip material handling systems.