

Principle and Working Scene Characteristics of Soap Granule Material Handling System Equipment
The soap granule material handling system represents a sophisticated piece of industrial equipment engineered to facilitate the efficient transport and processing of soap granules. As a critical component within the soap manufacturing sector, this system is instrumental in ensuring seamless production workflows and upholding the quality of the final product. The system's design incorporates advanced engineering principles tailored to address the unique physical and chemical properties of soap granules, such as their density, moisture content, and flow characteristics. By delving into the core principles and typical operational scenarios, stakeholders can gain a comprehensive understanding of its functionality and practical applications in diverse industrial settings.
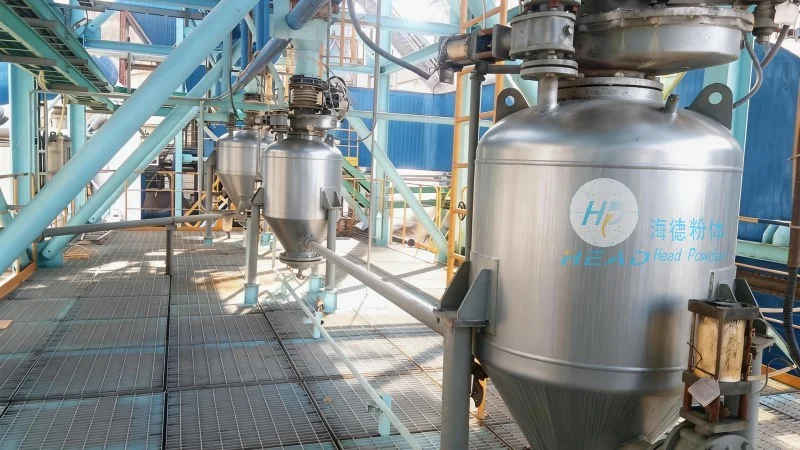
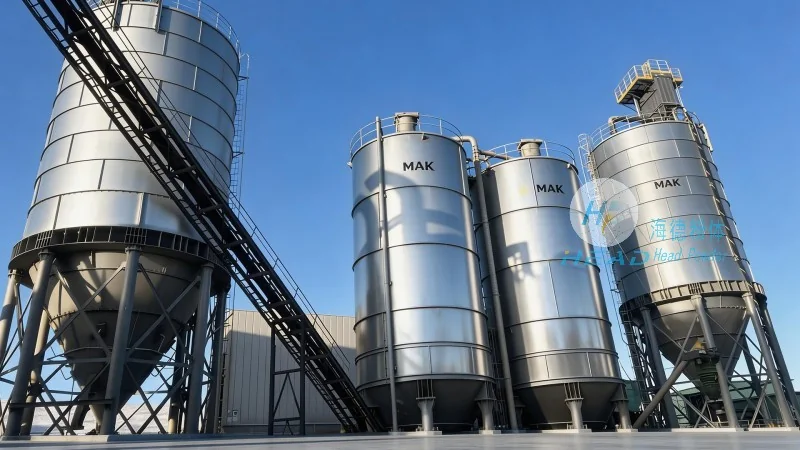
Core Principles Underpinning the System's Operation
The functionality of the soap granule material handling system is grounded in several fundamental principles that ensure reliable and efficient performance. Primarily, the system employs a combination of mechanical and pneumatic components to manage the movement of soap granules. This includes conveyor belts, screw conveyors, and air slides, each selected based on the specific handling requirements of the material. The system's control mechanisms, often integrated with programmable logic controllers (PLCs), enable precise regulation of speed, direction, and pressure, allowing for adaptability to varying production volumes and material conditions. Furthermore, the design incorporates features aimed at minimizing material degradation, such as gentle handling and controlled temperature environments, which are essential for preserving the integrity of soap granules during transport. The integration of sensors and feedback loops enhances the system's responsiveness, ensuring real-time adjustments to maintain optimal performance.
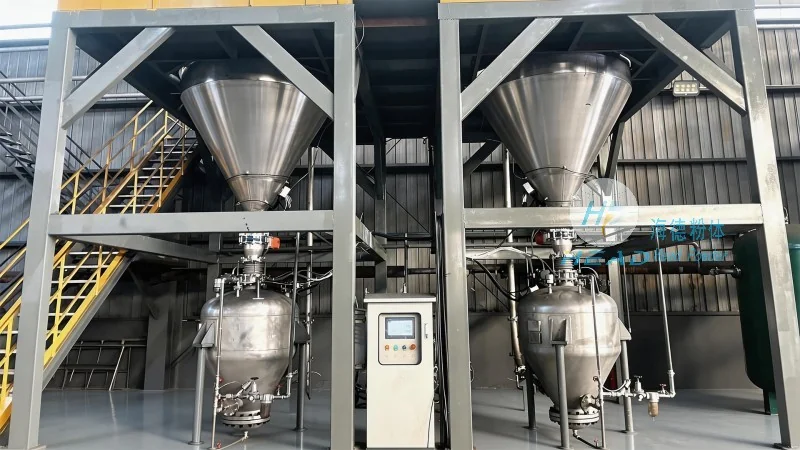
Working Scene Characteristics and Typical Applications
The soap granule material handling system is widely deployed across various industrial environments, each with distinct characteristics that influence its application. In soap manufacturing plants, the system is typically integrated into the production line to transport soap granules from mixing and drying stages to packaging or further processing units. This scenario often involves high-volume production, requiring the system to handle large quantities of material with minimal downtime, thereby supporting continuous production cycles. Another common scenario is in chemical processing facilities where soap granules serve as raw materials for other products, necessitating a system that can handle different material types and maintain consistent quality. The system's adaptability to different working conditions, including varying temperatures and humidity levels, makes it suitable for both indoor and outdoor applications, though most installations are indoors to protect the material from environmental factors. Additionally, the system's modular design allows for easy integration with existing production lines, reducing the need for extensive modifications and minimizing operational disruptions.
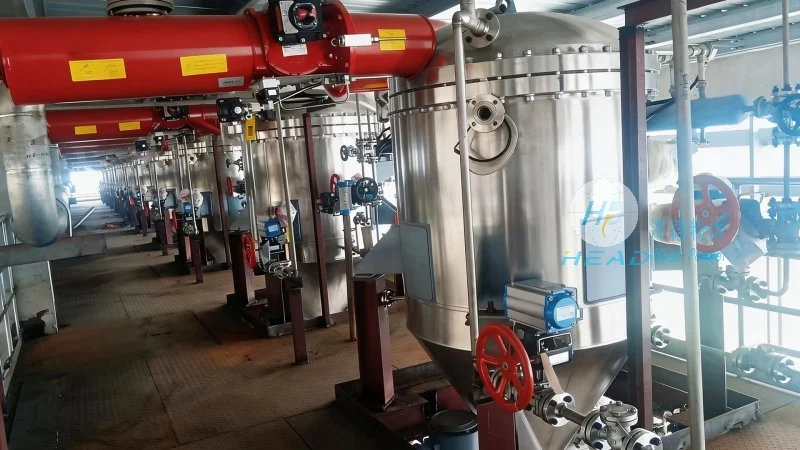
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a prominent manufacturer in the material handling equipment sector, specializes in developing customized solutions for the soap and chemical industries. With a strong commitment to innovation and quality, the company has built a reputation as a trusted partner for businesses seeking reliable and efficient material handling systems. HeadPowder's team of experienced engineers and technicians collaborates closely with clients to understand their specific operational needs, providing tailored solutions that align with industry standards and enhance overall efficiency. The company's manufacturing facilities, located in Shandong, China, are equipped with state-of-the-art technologies and rigorous quality control processes to ensure that every product meets the highest performance and safety benchmarks. By leveraging years of industry expertise and a customer-centric approach, HeadPowder continues to deliver cutting-edge solutions that support the growth and success of its clients in the competitive global market. The company's dedication to research and development ensures that its products remain at the forefront of technological advancements, addressing evolving industry demands and challenges.