

Principle and Application Scenarios of Intelligent Tonne Bag Feeding Station for Powder Pneumatic Co
Shandong HeadPowder Engineering Co., Ltd. is a professional manufacturer specializing in powder handling and conveying solutions. The company is headquartered in Shandong, China, and focuses on providing advanced equipment for industrial powder processing. The intelligent tonne bag feeding station is a key product designed to enhance the efficiency and safety of bulk powder handling in various industrial applications.
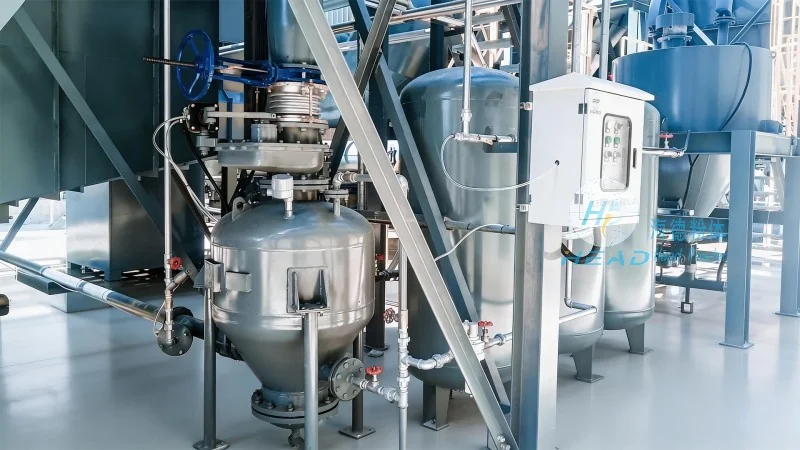
Overview of the Intelligent Tonne Bag Feeding Station
The intelligent tonne bag feeding station is engineered to automate the process of transferring powders from tonne bags into storage silos or processing lines. It integrates pneumatic conveying technology with advanced control systems to ensure precise, reliable, and safe material transfer. The system is designed for high-volume operations, reducing manual labor and minimizing the risk of contamination or material loss.
Core Principle of Powder Pneumatic Conveying
The fundamental principle of the powder pneumatic conveying system involves creating a pressure differential to move powder particles through a pipeline using compressed air. The intelligent feeding station utilizes this principle by generating a vacuum or pressure in the conveying line to draw or push the powder. Key components include the bag opening mechanism, rotary valve, air filter, and control panel, which work in concert to manage the flow rate, pressure, and air consumption. The system can handle a wide range of powder types, from fine powders like flour to coarse powders like cement, with adjustable parameters to match different material properties.
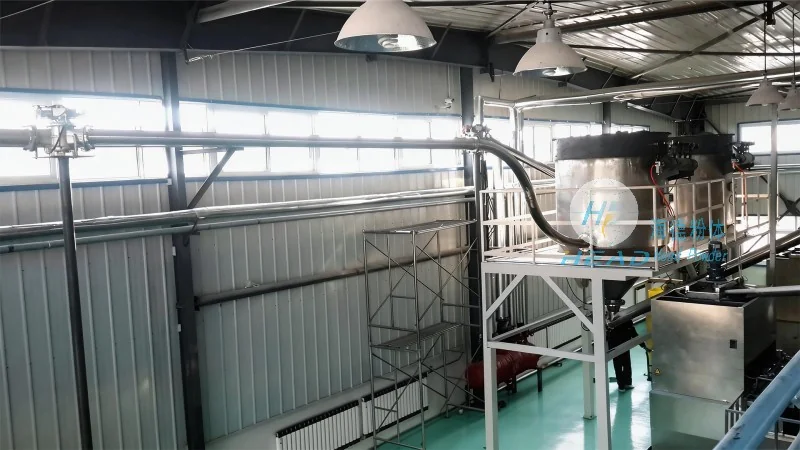
Key Features and Advantages
One of the primary advantages of the intelligent tonne bag feeding station is its high level of automation. The system can automatically open the tonne bag, discharge the material, and seal the bag, reducing the need for manual intervention. This not only improves operational efficiency but also enhances safety by minimizing exposure to dust and hazardous materials. The integrated air filtration system ensures that the air discharged from the process is clean, meeting environmental and occupational health standards.
Application Scenarios and Industry Use Cases
The intelligent tonne bag feeding station is widely used across multiple industries due to its versatility and reliability. In the food and beverage industry, it is commonly employed to feed raw materials such as sugar, flour, or cocoa into mixing lines, ensuring consistent product quality and preventing cross-contamination. In the pharmaceutical sector, the system maintains strict hygiene standards, with sealed components and HEPA filters to prevent contamination of sensitive powders. In chemical manufacturing, the equipment handles hazardous powders safely, with integrated safety features that shut down the system in case of abnormal conditions.
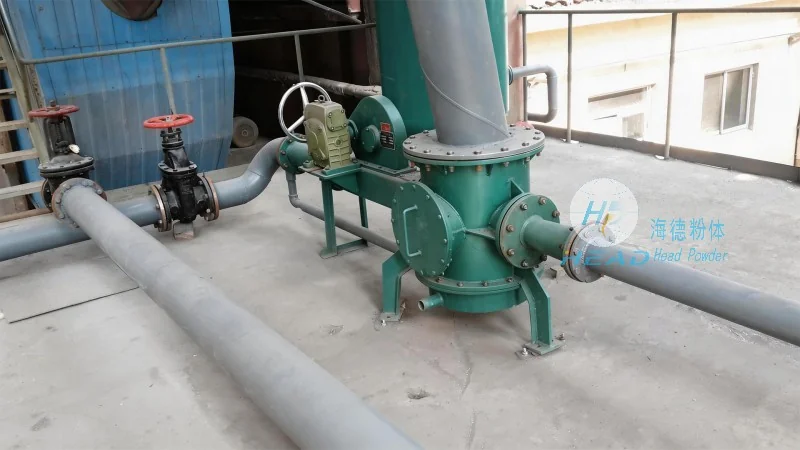
Technical Specifications and Customization Options
Shandong HeadPowder Engineering Co., Ltd. offers customizable solutions to meet the specific needs of different clients. The system can be configured with different conveying capacities, from small-scale operations to large industrial plants. The control panel provides real-time monitoring of the conveying process, with alerts for pressure drops, air leaks, or material blockages. The modular design allows for easy integration with existing production lines, and maintenance-friendly components reduce downtime and maintenance costs. The energy-efficient design optimizes air flow, reducing operational costs and environmental impact.
Conclusion and Service Support
Shandong HeadPowder Engineering Co., Ltd. provides comprehensive support for its intelligent tonne bag feeding station, including installation, training, and after-sales service. The company's expertise in powder handling technology ensures that clients receive reliable and efficient solutions tailored to their specific requirements. By combining advanced technology with professional service, HeadPowder helps industries enhance productivity, improve safety, and reduce operational costs in their powder handling processes.