

Detailed Explanation of Manganese Carbonate Pneumatic Conveying Systems
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems for manganese carbonate. This article provides a comprehensive overview of such systems, highlighting their technical aspects, operational benefits, and practical applications.
Company Overview
HeadPowder Engineering Co., Ltd. is a professional manufacturer and supplier dedicated to providing high-quality pneumatic conveying solutions. With a strong presence in the industrial sector, the company leverages its expertise to deliver reliable systems tailored to the unique needs of clients in the manganese carbonate industry. HeadPowder's commitment to innovation and precision ensures that each system is engineered to meet stringent performance standards and operational requirements.
Pneumatic Conveying Systems for Manganese Carbonate
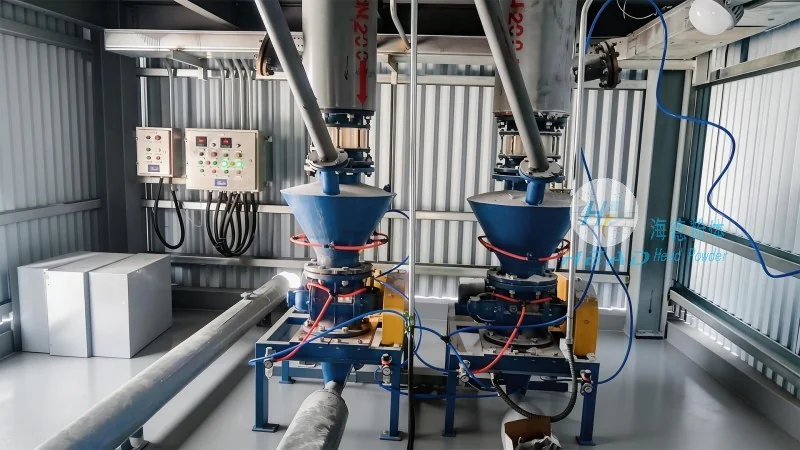
The pneumatic conveying system for manganese carbonate is a sophisticated technology that enables the efficient transport of powdered materials like manganese carbonate through a pressurized air stream. This method offers several advantages over traditional mechanical conveying, including reduced equipment wear, lower maintenance costs, and enhanced safety in handling potentially dusty or hazardous materials. The system typically consists of key components such as a hopper for material storage, a rotary valve for controlled discharge, a conveying line, and a receiver for material deposition. Each component is carefully designed to optimize the flow and pressure conditions required for effective material transport.
Technical Advantages and Operational Benefits
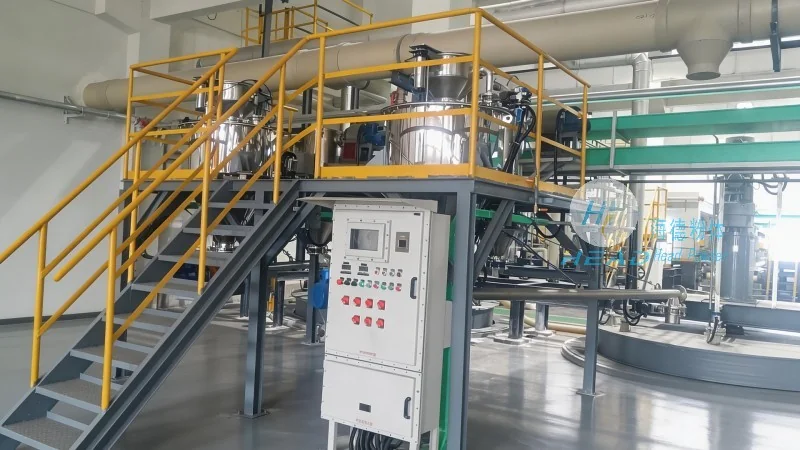
One of the primary benefits of pneumatic conveying systems for manganese carbonate is their ability to handle materials with high moisture content or varying particle sizes without clogging or degradation. The pressurized air stream ensures consistent material movement, minimizing the risk of blockages and ensuring a steady flow rate. Additionally, these systems are highly adaptable, allowing for integration with existing production lines or expansion as operational needs evolve. From small-scale laboratory applications to large industrial facilities, the flexibility of pneumatic conveying makes it a preferred choice for many manganese carbonate processing operations. The technology also contributes to improved safety by eliminating the need for manual handling of powders, reducing exposure to dust and potential health hazards.
System Components and Design Considerations
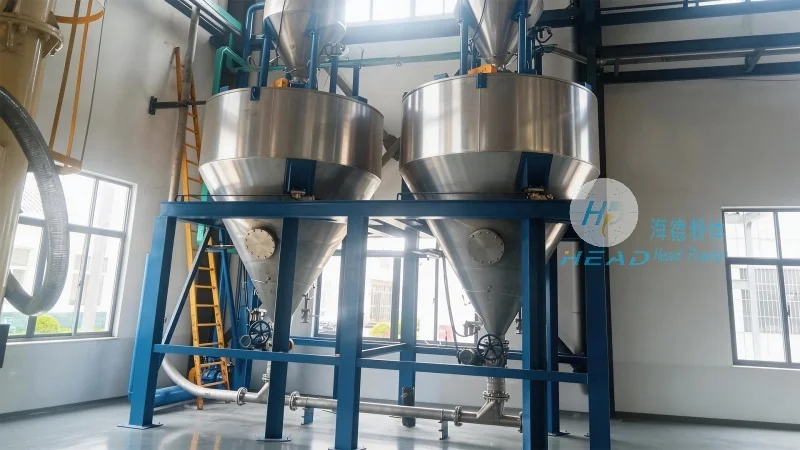
The design of a pneumatic conveying system for manganese carbonate involves careful consideration of several factors to ensure optimal performance. Material properties, such as density, moisture content, and particle size distribution, play a crucial role in determining the appropriate conveying velocity and pressure. The system's layout, including the length and diameter of the conveying line, the placement of the hopper and receiver, and the selection of components like the rotary valve and air compressor, are all critical to achieving efficient material transport. HeadPowder engineers employ advanced computational fluid dynamics (CFD) and material flow analysis to simulate and optimize system performance before implementation. This approach ensures that the final system meets the client's specific requirements while minimizing energy consumption and operational costs.
Applications and Industry Impact
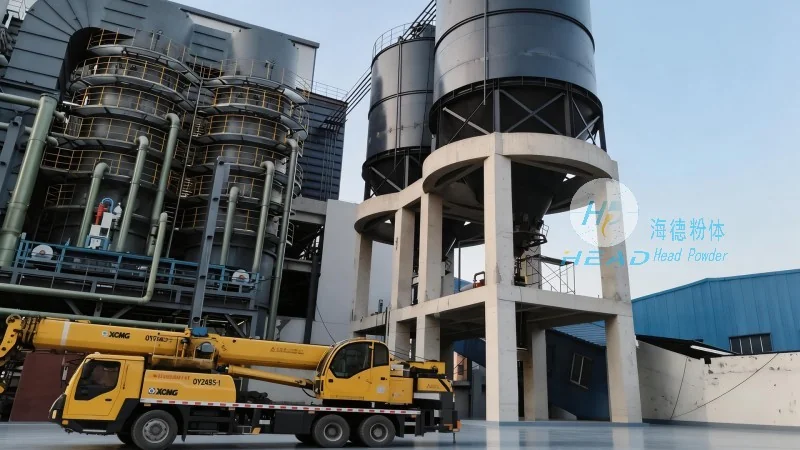
Pneumatic conveying systems for manganese carbonate are widely used in various industrial applications, including mining, chemical processing, and material handling. In mining operations, these systems facilitate the transport of manganese carbonate from extraction sites to processing facilities, improving operational efficiency and reducing transportation costs. In chemical processing plants, the technology is employed to move raw materials to reactors or storage areas, supporting continuous production processes. The systems also find applications in environmental remediation projects, where they help in the removal and transport of contaminated materials. By enhancing the efficiency and safety of material handling, pneumatic conveying systems contribute to the overall productivity and sustainability of industrial operations.
Conclusion and Future Outlook
HeadPowder Engineering Co., Ltd. continues to lead the development of advanced pneumatic conveying systems for manganese carbonate, combining technical expertise with customer-centric solutions. The company's commitment to innovation ensures that its systems remain at the forefront of industrial material handling technology. As the demand for efficient and sustainable processing solutions grows, pneumatic conveying systems will likely play an increasingly important role in the manganese carbonate industry. With its strong foundation in engineering and a focus on client satisfaction, HeadPowder is well-positioned to meet the evolving needs of the market and provide reliable, high-performance solutions for years to come.