

[Rare Earth Crystal Powder Pneumatic Conveying Systems: A Detailed Explanation]
For industries dealing with rare earth crystal powders, efficient and reliable material handling is crucial. The pneumatic conveying system represents a sophisticated solution that ensures seamless transport of these valuable materials. This article provides an in-depth look at the rare earth crystal powder pneumatic conveying system, highlighting its components, operational principles, and the benefits it offers to manufacturers.
Understanding the Core Components of the System
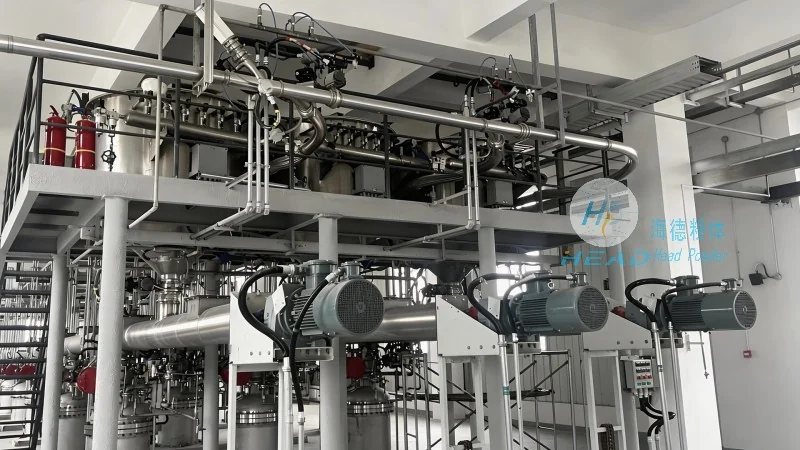
The rare earth crystal powder pneumatic conveying system is composed of several key components that work in tandem to achieve effective material transport. The primary elements include the material hopper, which serves as the storage and feeding unit for the powder. This hopper is designed to maintain the integrity of the rare earth crystals, preventing agglomeration or degradation during storage. The feeding mechanism, typically a rotary valve or a star feeder, regulates the flow of powder from the hopper into the conveying line. This controlled feeding is essential to maintain consistent air-powder ratios and prevent system blockages.
At the heart of the system is the conveying line, which can be either a positive or negative pressure system. Positive pressure systems use a blower to push air and powder through the pipeline, while negative pressure systems employ a vacuum pump to draw the material. The choice between these systems depends on factors such as the distance of transport, the material's properties, and the desired flow rate. The pipeline itself is constructed from materials resistant to corrosion and wear, often stainless steel or specialized polymers, to ensure durability and prevent contamination of the rare earth crystals.
Operational Principles and Flow Dynamics
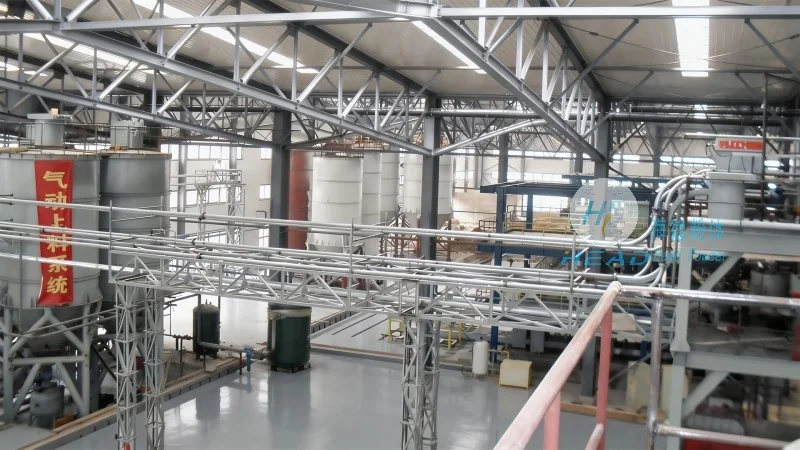
The pneumatic conveying system operates on the principle of air movement to transport solid particles. In a positive pressure system, the blower generates a high-pressure air stream that carries the rare earth crystal powder through the pipeline. The air-powder mixture travels at a velocity sufficient to keep the particles suspended, preventing settling or clogging. The flow dynamics are carefully controlled to maintain optimal velocity and pressure, which directly impacts the system's efficiency and the condition of the material. For negative pressure systems, the vacuum pump creates a low-pressure environment that draws the powder from the source and transports it to the destination. This method is particularly useful for applications requiring dust control and minimal environmental impact.
The system also incorporates control valves and filters to regulate the flow and maintain air quality. Control valves, such as butterfly or gate valves, allow operators to adjust the flow rate and pressure as needed. Filters, including cyclone separators and bag filters, are used to separate the powder from the air stream, ensuring that the material is delivered to the destination without contamination. The collected powder is then returned to the system or stored for further processing. This closed-loop system minimizes waste and enhances overall efficiency.
Benefits and Applications in Rare Earth Processing
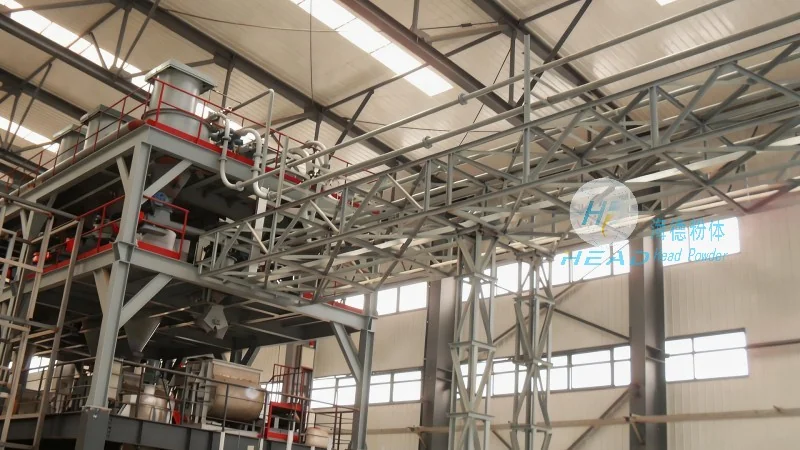
The rare earth crystal powder pneumatic conveying system offers numerous advantages for industries involved in rare earth processing. One of the key benefits is the ability to handle delicate materials without causing damage or degradation. The gentle handling reduces the risk of agglomeration, which can affect the material's properties and performance. Additionally, the system provides a dust-free environment, which is critical for maintaining product quality and ensuring compliance with environmental regulations. The enclosed nature of the system also minimizes exposure to hazardous materials, enhancing workplace safety.
These systems are widely used in various applications, including the transport of rare earth oxides, metals, and alloys from production facilities to processing plants or storage areas. They are particularly suitable for long-distance transport, as the pneumatic system can cover significant distances without the need for intermediate transfer points. The flexibility of the system allows it to be integrated into existing production lines, making it a cost-effective solution for upgrading material handling capabilities. Furthermore, the system's ability to handle varying flow rates and material compositions makes it adaptable to different production scenarios.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of specialized engineering solutions for material handling systems. With a focus on innovation and quality, the company has established itself as a trusted partner in the rare earth processing industry. HeadPowder specializes in designing and manufacturing pneumatic conveying systems tailored to the unique needs of their clients. The company's team of experts works closely with customers to understand their specific requirements and develop customized solutions that enhance operational efficiency and product quality.
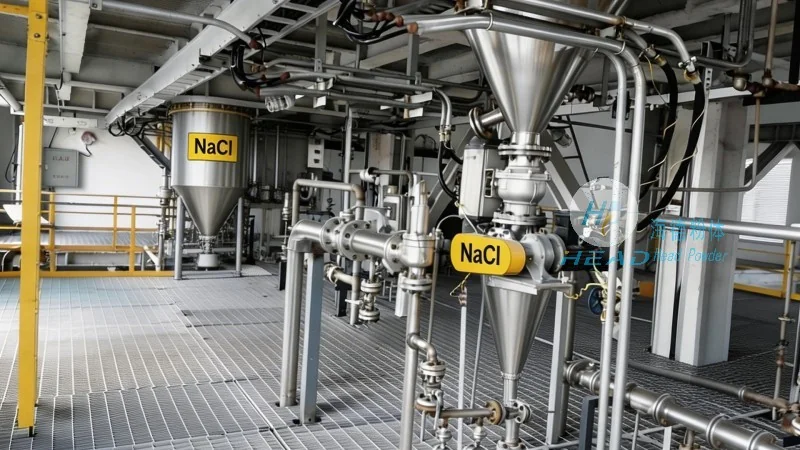
HeadPowder's commitment to excellence is reflected in their use of advanced technology and rigorous quality control processes. The company adheres to international standards and continuously invests in research and development to improve their products and services. With a strong presence in China, particularly in Shandong, HeadPowder leverages its local expertise and resources to deliver reliable and efficient solutions to clients worldwide. The company's dedication to customer satisfaction and sustainable practices has earned it a reputation as a leading supplier in the material handling sector.
Conclusion and Future Outlook
The rare earth crystal powder pneumatic conveying system is a vital component in modern rare earth processing, offering efficient, reliable, and safe material transport. As the demand for rare earth materials continues to grow, the importance of advanced material handling systems becomes increasingly evident. Companies like Shandong HeadPowder Engineering Co., Ltd. play a crucial role in providing these solutions, helping manufacturers optimize their operations and meet the evolving needs of the industry. With ongoing advancements in technology, the future of pneumatic conveying systems looks promising, with potential for further improvements in efficiency, scalability, and environmental sustainability.