

Application and Optimization of Pneumatic Conveying Technology in Carbonate Manganese Transport Desi
Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in the field of powder handling and material transport, specializes in providing advanced solutions for the efficient and reliable movement of bulk materials. With a focus on innovation and precision engineering, the company has developed and refined pneumatic conveying systems tailored to the unique requirements of industries dealing with carbonate manganese, a critical mineral used in various industrial applications.
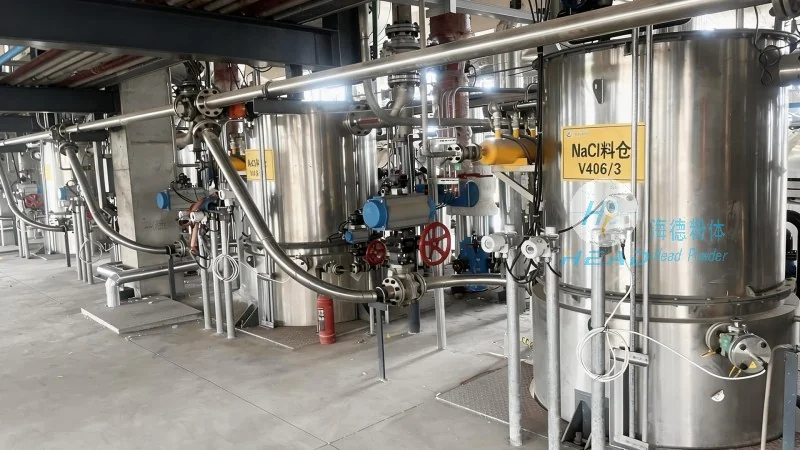
Pneumatic Conveying Technology: An Overview
Pneumatic conveying, also known as air conveying, is a method of transporting bulk materials through a pipeline using a stream of air. This technology offers several advantages over traditional mechanical conveying systems, including reduced equipment wear, lower maintenance costs, and the ability to handle materials that are difficult to transport by other means. For carbonate manganese, which is often a fine or powdery substance, pneumatic conveying provides a gentle and efficient way to move the material from one location to another without causing degradation or contamination.
Characteristics of Carbonate Manganese and Its Transport Challenges
Carbonate manganese, typically found in the form of manganese carbonate (MnCO₃), is a light-colored, crystalline powder with specific physical properties that impact its handling. The material is often hygroscopic, meaning it can absorb moisture from the air, which can affect its flowability and stability during transport. Additionally, carbonate manganese may have varying particle sizes and densities, leading to challenges in achieving consistent flow rates and preventing blockages in conveying systems. These characteristics make it essential to design a pneumatic conveying system that addresses these specific material properties to ensure optimal performance.
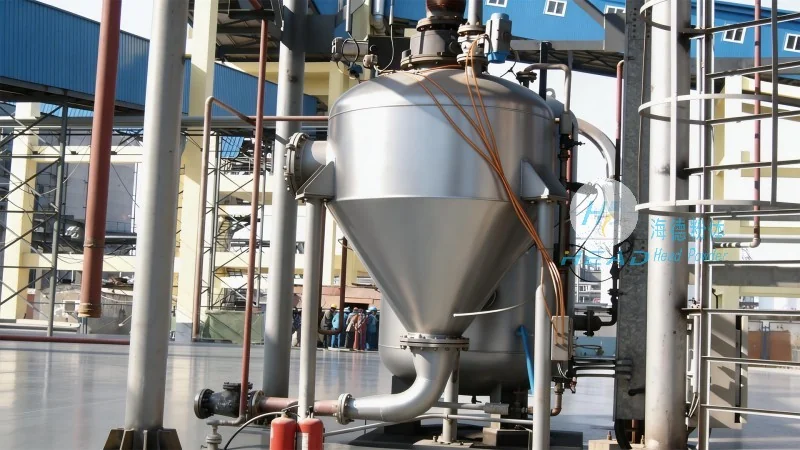
Application of Pneumatic Conveying in Carbonate Manganese Transport
HeadPowder Engineering has extensive experience in designing and implementing pneumatic conveying systems for carbonate manganese transport in industrial settings. The company's solutions are customized to meet the specific needs of clients, including the selection of appropriate air velocities, pipeline configurations, and material handling equipment. For example, in mining and processing facilities, the system may be designed to transport carbonate manganese from storage silos to processing units, or from processing areas to packaging stations. The use of pneumatic conveying allows for a continuous, closed-loop system that minimizes material exposure to the environment and reduces the risk of dust emissions.
Optimization Strategies for Pneumatic Conveying Systems
To maximize the efficiency and reliability of pneumatic conveying systems for carbonate manganese, several optimization strategies are employed. These include the selection of the right type of air compressor and control system, which ensures consistent air pressure and flow rates. The design of the pipeline system, including the use of appropriate bends, elbows, and valves, is critical to maintaining smooth material flow and preventing pressure drops that could lead to blockages. Additionally, the use of air filtration and dust collection systems helps to maintain the purity of the material and comply with environmental regulations. HeadPowder Engineering employs advanced simulation tools and field testing to optimize these parameters, ensuring that the system operates at peak performance with minimal downtime.
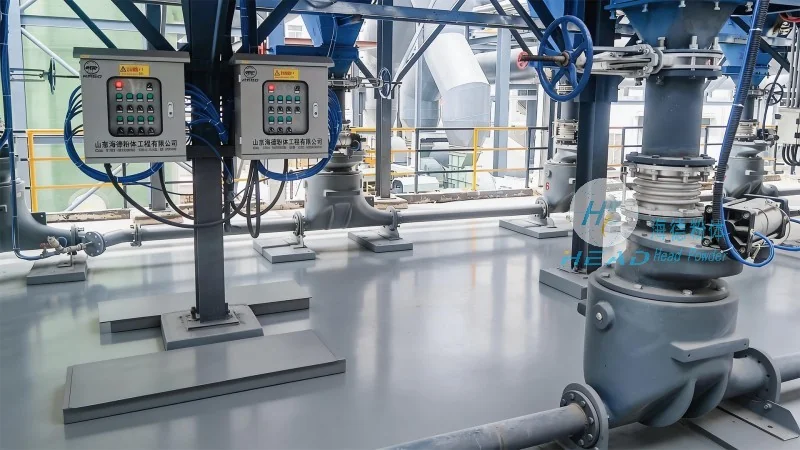
Benefits of Optimized Pneumatic Conveying for Carbonate Manganese
The application of optimized pneumatic conveying technology in carbonate manganese transport offers numerous benefits for industrial operations. These include increased productivity through continuous material flow, reduced labor costs due to automated systems, and improved material quality by minimizing handling-related degradation. Additionally, the closed-loop system reduces environmental impact by controlling dust emissions and preventing material loss. For clients in the mining, chemical, or manufacturing sectors, these benefits translate into enhanced operational efficiency and cost savings over the long term.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. continues to lead the way in the application and optimization of pneumatic conveying technology for carbonate manganese transport. By leveraging advanced engineering, customized system design, and rigorous optimization strategies, the company provides reliable and efficient solutions that meet the evolving needs of industries relying on this critical mineral. With a strong commitment to quality and customer satisfaction, HeadPowder Engineering remains a trusted partner for businesses seeking to enhance their material handling processes and achieve operational excellence.