

Application and Optimization of Pneumatic Conveying Technology in Rare Earth Crystal Powder Handling
For industries dealing with rare earth crystal powders, efficient and reliable material handling is critical to maintaining production efficiency and product quality. Pneumatic conveying technology has emerged as a key solution, offering a non-contact, low-cost method to transport these sensitive materials. This article explores how Shandong HeadPowder Engineering Co., Ltd. leverages advanced pneumatic conveying systems to optimize the design and operation of rare earth crystal powder handling processes.
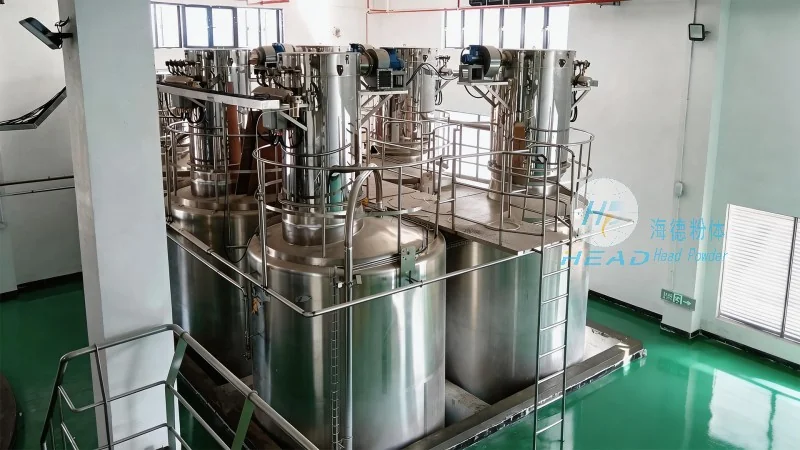
Understanding the Challenges of Rare Earth Crystal Powder Handling
Rare earth crystal powders are known for their fine particle size, high reactivity, and tendency to agglomerate. Traditional handling methods, such as bucket elevators or belt conveyors, often face challenges like material degradation, equipment wear, and contamination risks. These issues can lead to increased operational costs and reduced product purity. The need for a more sophisticated approach to material transport has driven the adoption of pneumatic conveying systems in the rare earth industry.
HeadPowder's Pneumatic Conveying Solutions for Rare Earth Powders
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and implementing customized pneumatic conveying solutions tailored to the unique characteristics of rare earth crystal powders. The company's approach focuses on optimizing system performance through careful selection of components, including high-efficiency blowers, flexible hoses, and specialized cyclone separators. By integrating these elements, HeadPowder ensures that the conveying process minimizes particle degradation, maintains product integrity, and reduces energy consumption.
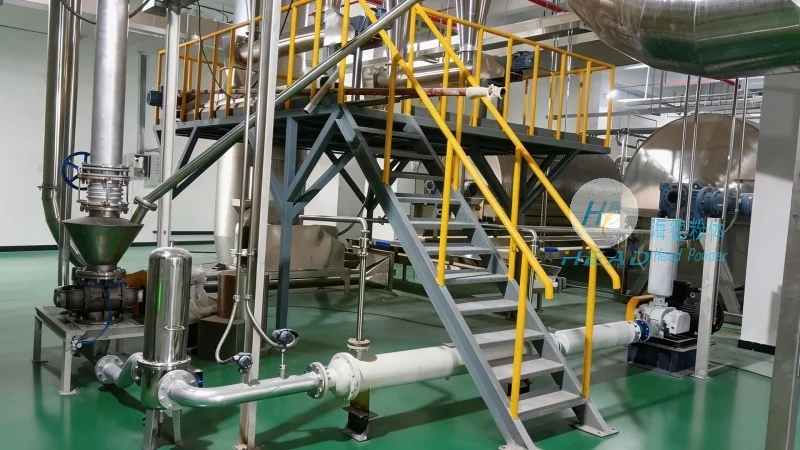
Key Features of the Optimized Pneumatic Conveying System
The optimized system developed by HeadPowder incorporates several advanced features that address the specific challenges of rare earth crystal powder handling. One of the primary components is the high-pressure blower, which provides the necessary air pressure to move the fine particles through the system without causing excessive friction or heat. The flexible, abrasion-resistant hoses are designed to withstand the abrasive nature of the powder, ensuring long service life and minimal maintenance. Additionally, the cyclone separator efficiently separates the powder from the air stream, allowing for clean material recovery and reduced environmental impact.
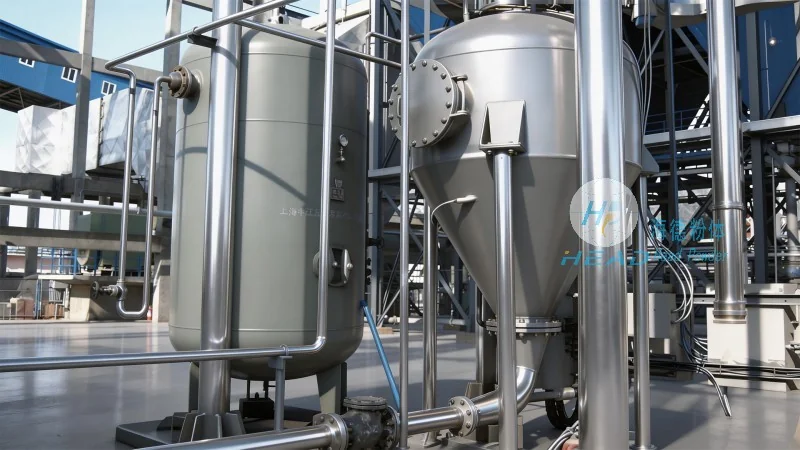
Benefits of Implementing HeadPowder's Pneumatic Conveying Technology
The adoption of HeadPowder's optimized pneumatic conveying system offers several significant benefits for rare earth processing facilities. First, the non-contact transport method prevents contamination and product degradation, preserving the purity and quality of the rare earth crystals. Second, the system's energy efficiency reduces operational costs, making it a cost-effective solution for long-term use. Third, the customized design allows for seamless integration with existing production lines, minimizing downtime during installation and operation. Finally, the reduced maintenance requirements and extended equipment life contribute to overall operational reliability and lower total cost of ownership.
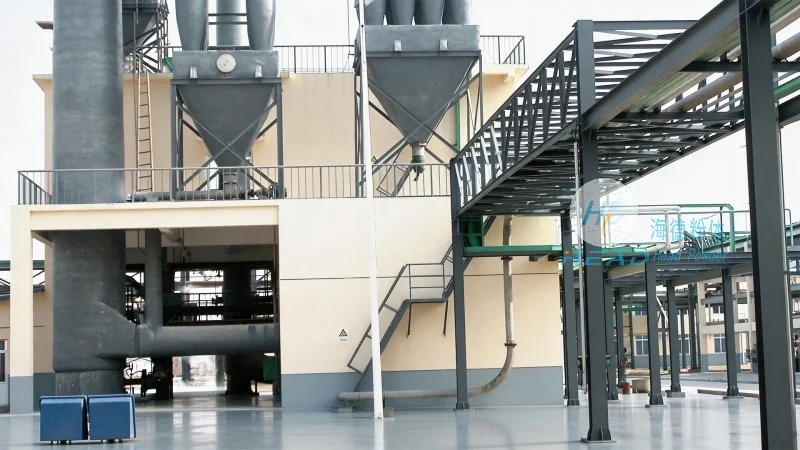
Case Study: Enhancing Production Efficiency at a Leading Rare Earth Plant
A leading rare earth processing plant in China recently implemented HeadPowder's pneumatic conveying system to replace an outdated bucket elevator. The new system was designed to handle a high volume of fine crystal powders while maintaining strict quality control standards. The results were immediate and substantial: production throughput increased by 25%, and product purity improved by 10% compared to the previous method. The plant also reported a 30% reduction in energy consumption and a 40% decrease in maintenance costs over the first year of operation. This case study highlights the effectiveness of HeadPowder's technology in addressing real-world challenges and delivering measurable improvements in industrial performance.
Conclusion: The Future of Rare Earth Powder Handling with Pneumatic Conveying
As the demand for rare earth materials continues to grow, the importance of efficient material handling cannot be overstated. Shandong HeadPowder Engineering Co., Ltd. remains at the forefront of developing advanced pneumatic conveying solutions that meet the evolving needs of the industry. By focusing on innovation, customization, and performance optimization, HeadPowder ensures that its clients can achieve higher productivity, better product quality, and lower operational costs. The application and optimization of pneumatic conveying technology represent a significant advancement in rare earth crystal powder handling, and HeadPowder's expertise positions the company as a trusted partner for businesses seeking to enhance their material transport processes.