

Application and Optimization of Pneumatic Conveying Technology in Glucose Powder Conveying Design
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced material handling solutions. With a focus on optimizing industrial processes, the company has developed expertise in pneumatic conveying systems, particularly for handling glucose powder—a critical component in various food and pharmaceutical applications.
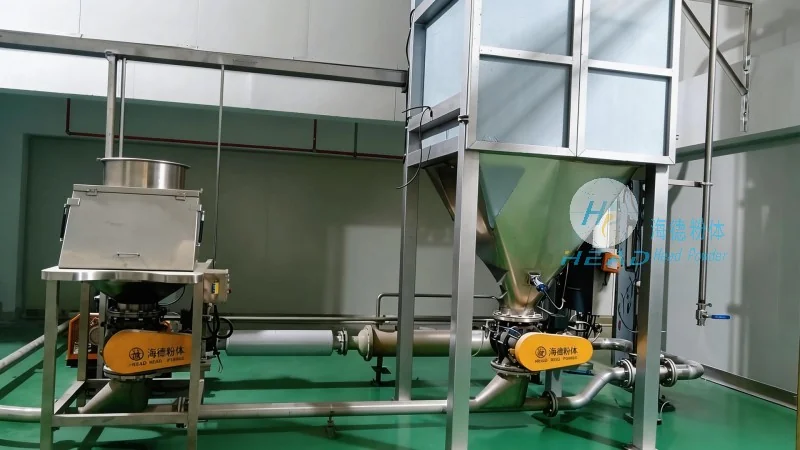
Pneumatic Conveying: A Solution for Glucose Powder Handling
Glucose powder, known for its fine particle size and hygroscopic properties, poses unique challenges during transportation. Traditional methods such as belt conveyors or bucket elevators often lead to material degradation, dust generation, and operational inefficiencies. Pneumatic conveying technology offers a more efficient and controlled approach to move glucose powder from storage to processing units. This method uses compressed air to transport the material through a pipeline, ensuring minimal product contact with external elements and reducing the risk of contamination.
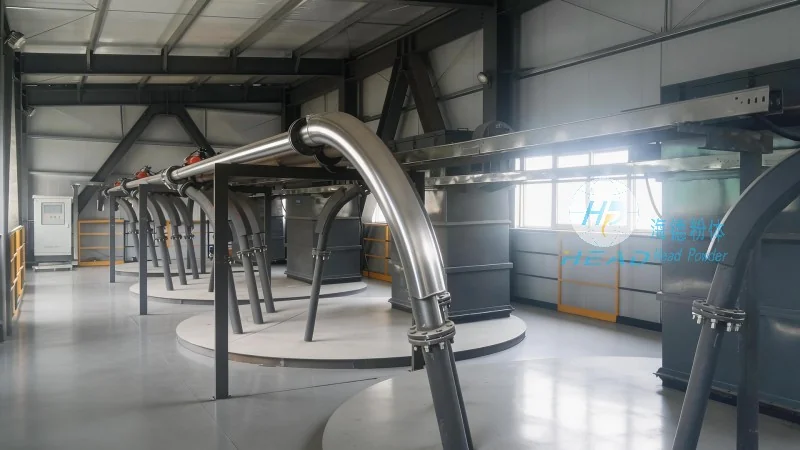
Design Considerations for Optimal Glucose Powder Conveying
The success of a pneumatic conveying system for glucose powder hinges on meticulous design. Key factors include the selection of appropriate air velocity, pipeline diameter, and the integration of features like cyclone separators and filter systems. HeadPowder engineers consider the specific characteristics of glucose powder—such as its flowability and tendency to agglomerate—to tailor the system. For instance, the use of airlocks and rotary valves at the discharge point helps maintain consistent flow rates and prevents blockages. Additionally, the system is designed to minimize pressure drops, ensuring energy efficiency and reducing operational costs over time.
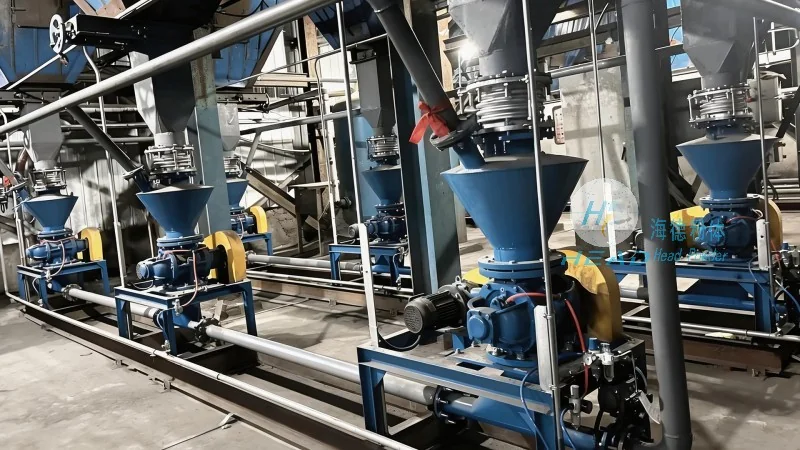
Enhancing Process Efficiency with Pneumatic Conveying
By implementing optimized pneumatic conveying systems, industries dealing with glucose powder can achieve significant improvements in operational efficiency. The technology allows for continuous, dust-free transfer of material, which is essential for maintaining product quality in food and pharmaceutical sectors. Moreover, the reduced need for manual handling and the elimination of manual transfer points enhance workplace safety. HeadPowder’s expertise in customizing these systems ensures that clients receive solutions tailored to their specific production volumes and operational requirements, maximizing both productivity and cost-effectiveness.
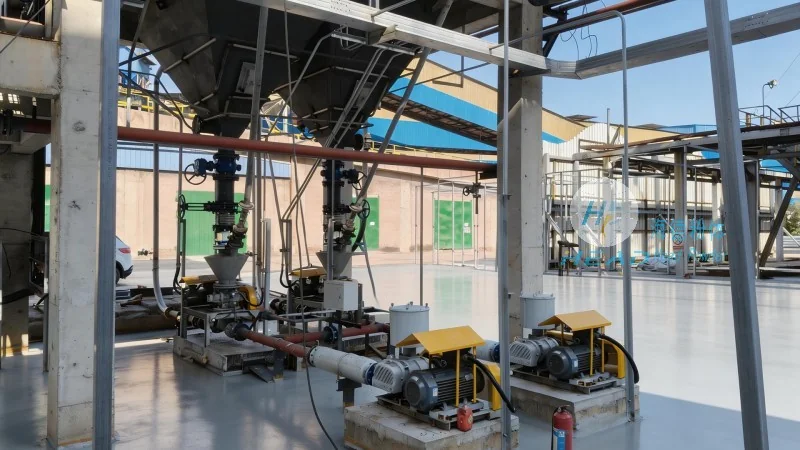
Conclusion: The Role of HeadPowder in Advancing Glucose Powder Handling
HeadPowder Engineering Co., Ltd., located in Shandong, China, continues to lead the way in providing innovative and efficient material handling solutions for glucose powder. Through the application of advanced pneumatic conveying technology and rigorous design optimization, the company helps industries streamline their processes, improve product quality, and enhance overall operational performance. As a trusted partner in the field, HeadPowder remains committed to delivering solutions that meet the evolving needs of the food and pharmaceutical industries.