

What is a Glucose Powder Pneumatic Conveying Machine? What is its Design Principle?
Glucose powder pneumatic conveying machines are specialized equipment designed to transport granular or powdered materials, such as glucose, through a pipeline using air or other gas as the conveying medium. This technology offers an efficient and hygienic solution for handling fine powders in various industrial applications. HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of such equipment, ensuring that glucose powder is handled with precision and care.
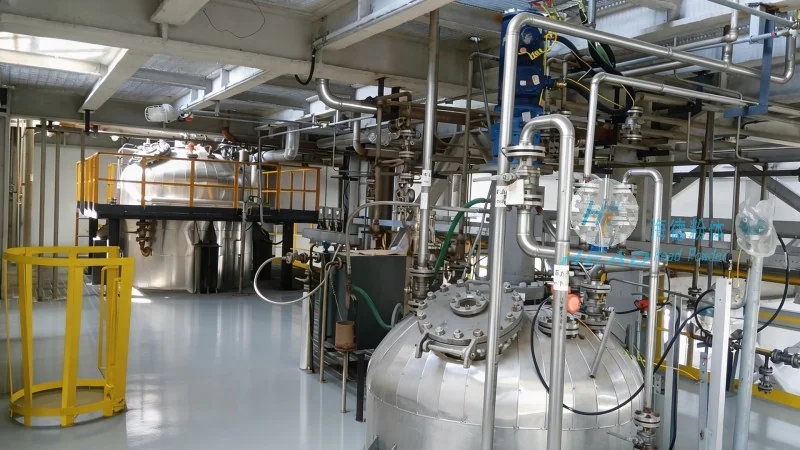
Understanding the Core Function of Glucose Powder Pneumatic Conveying Machines
At the heart of a glucose powder pneumatic conveying system lies the ability to move glucose powder from a storage or processing point to a destination like a silo, reactor, or packaging line. The process relies on creating a pressure differential or using vacuum to draw the powder into the conveying line. This method is particularly advantageous for glucose powder due to its fine particle size and potential for dust generation, as it minimizes product contamination and loss compared to traditional mechanical conveying methods.
The Design Principle Behind Glucose Powder Pneumatic Conveying Machines
The design principle of these machines centers on the interaction between the powder and the conveying air. Key components include a hopper for material storage, a rotary valve or feeder to control the powder flow, a conveying pipe, and a receiver or discharge unit. The system operates by introducing air into the conveying line, either by pressurizing the line (positive pressure) or creating a vacuum (negative pressure). For glucose powder, which is hygroscopic and sensitive to moisture, the design must ensure that the conveying air is dry and filtered to prevent clumping or degradation of the powder. The velocity of the air in the pipe is critical; it must be sufficient to keep the powder particles suspended and prevent deposition, while also avoiding excessive wear on the pipe and components.
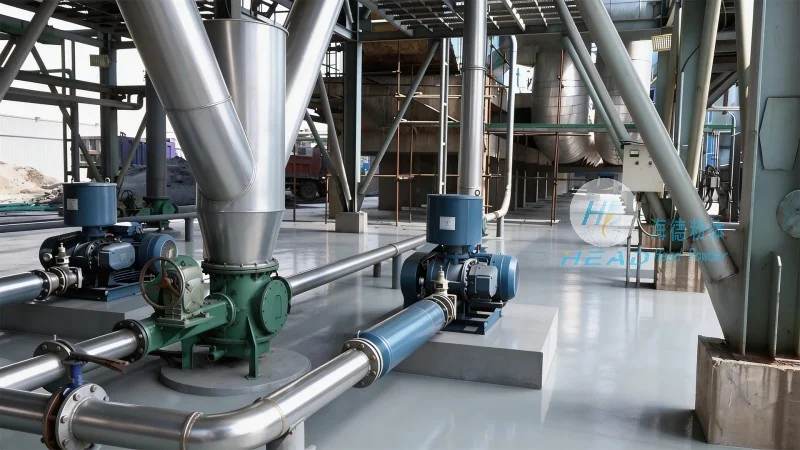
Key Features and Benefits for Glucose Powder Handling
When selecting a glucose powder pneumatic conveying machine, several features are essential for optimal performance. These include a robust hopper design to prevent material bridging or caking, which is common in hygroscopic powders like glucose. The feeder mechanism, often a rotary valve or a star feeder, must be capable of handling fine powders without blockages. The conveying line material, typically stainless steel or food-grade plastic, is chosen to maintain the purity and quality of the glucose powder. Additionally, the system may incorporate filters and moisture control units to ensure the powder remains in optimal condition throughout the conveying process. The benefits of using such a machine include improved process efficiency, reduced labor costs, enhanced product quality by minimizing exposure to contaminants, and better safety due to enclosed systems that prevent dust dispersion.
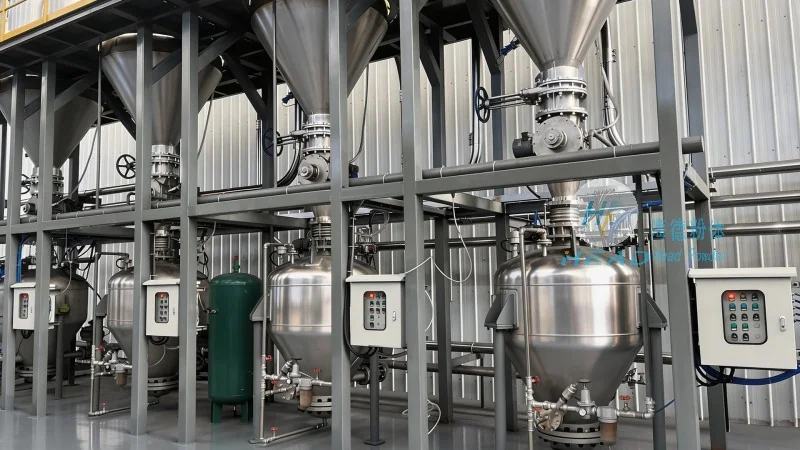
Application Examples in the Glucose Industry
Glucose powder pneumatic conveying machines are widely used in the food and pharmaceutical industries for transporting glucose from storage silos to processing lines. For instance, in a glucose manufacturing plant, the machine can efficiently move glucose powder from a bulk storage tank to a mixing or drying unit. This ensures a continuous and clean flow of material, which is crucial for maintaining production schedules and product consistency. The design of the machine, with its enclosed and sanitary construction, aligns with industry standards for food processing, where hygiene and product purity are paramount. By using a pneumatic conveying system, manufacturers can avoid the issues associated with mechanical conveyors, such as product degradation, contamination, or the need for frequent cleaning and maintenance.
Conclusion: The Importance of Proper Design and Implementation
In conclusion, glucose powder pneumatic conveying machines are a vital piece of equipment for industries handling fine, hygroscopic powders like glucose. The design principle, which focuses on efficient air-powder interaction and material handling, ensures that the powder is transported safely and effectively. By incorporating features such as dry air filtration, robust feeding mechanisms, and sanitary construction, these machines provide significant benefits in terms of efficiency, product quality, and operational safety. For companies like Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, the development and implementation of these machines reflect a commitment to providing high-quality, reliable equipment tailored to the specific needs of the glucose industry, supporting the smooth operation of production lines and the maintenance of product standards.