

What is a Cereal Pneumatic Conveying System Equipment? And What Are Its Design Principles?
A cereal pneumatic conveying system is a specialized industrial equipment designed to transport bulk materials, particularly cereals and similar dry granular products, from one location to another using air as the conveying medium. This system is widely utilized in the food processing industry, agricultural sectors, and other applications where the efficient and hygienic movement of bulk materials is essential. The core function of such a system is to move materials through a pipeline by creating a flow of air that propels the material particles, ensuring a continuous and controlled transfer process. These systems are crucial for optimizing material handling in production lines, reducing labor costs, and maintaining product quality by minimizing exposure to contaminants and handling damage.
Design Principles of Cereal Pneumatic Conveying Systems
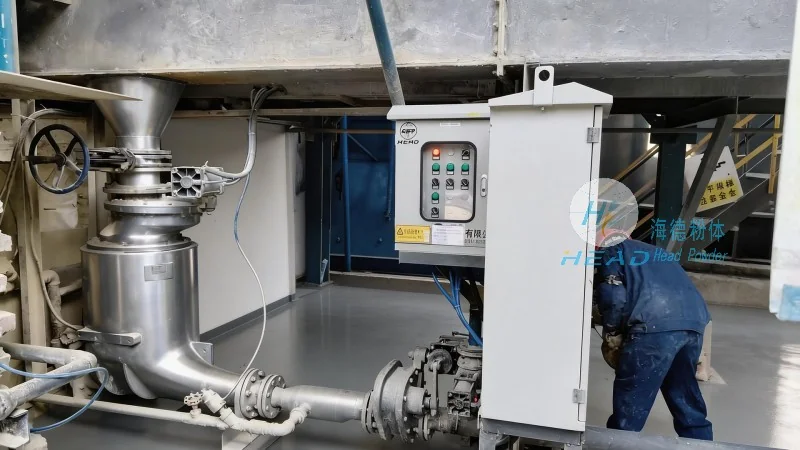
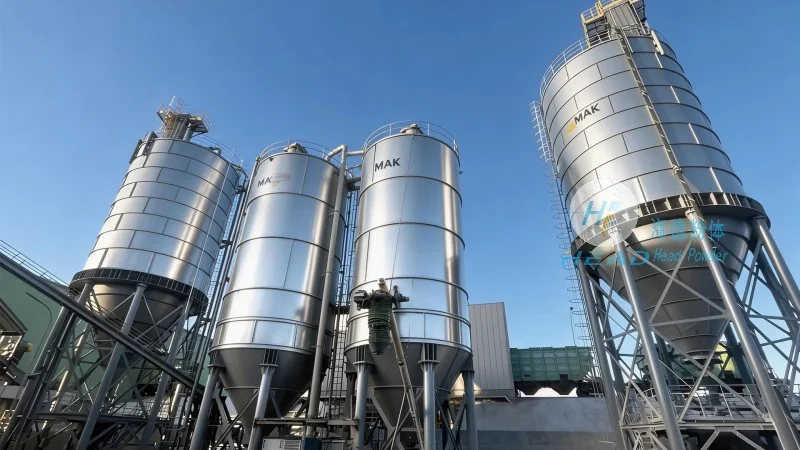
The design of a cereal pneumatic conveying system is based on several key principles that ensure efficient material transport and system reliability. The primary principle involves the creation of a pressure differential within the conveying line. By generating a higher pressure at the inlet and a lower pressure at the outlet, the system creates a flow of air that carries the cereal particles through the pipeline. This is typically achieved using a blower or a vacuum pump, which provides the necessary air flow and pressure. The system also incorporates components such as hoppers, feeders, and control valves to regulate the flow of material and air, ensuring optimal performance. The design must consider factors like material characteristics (e.g., particle size, density, moisture content), system length, and the required conveying capacity to determine the appropriate air velocity and pressure levels. Proper design also includes features like cleaning mechanisms and safety valves to prevent blockages and maintain system integrity. Additionally, the system is engineered to meet hygiene standards, often using stainless steel construction and easy-to-clean components, which is critical in food processing applications where product safety is paramount.
Cereal Pneumatic Conveying System Equipment: Core Components and Functionality
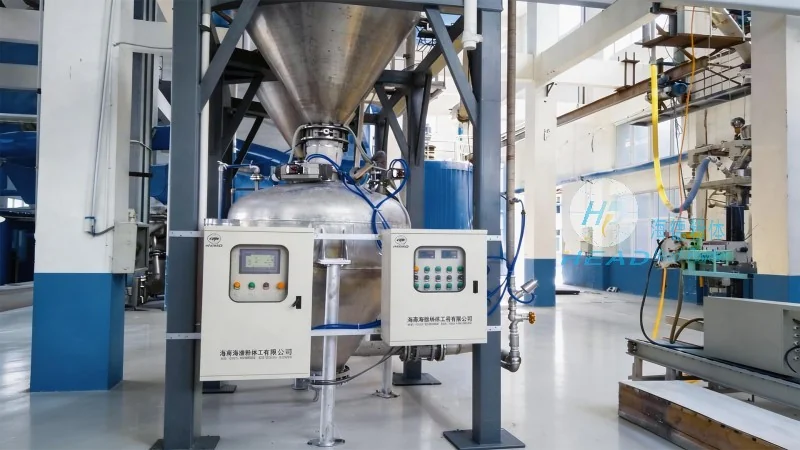
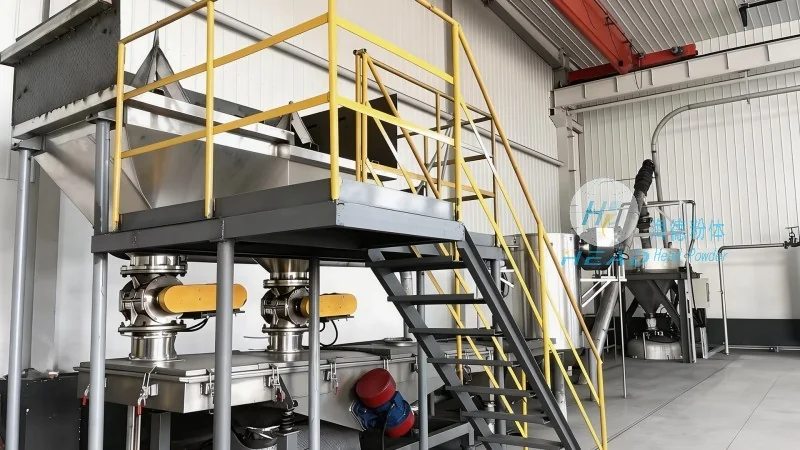
A typical cereal pneumatic conveying system consists of several key components that work together to achieve efficient material transport. The main components include a hopper or feeder, which holds the cereal material and feeds it into the system at a controlled rate. The feeder may be a rotary valve or a screw feeder, depending on the material characteristics and system requirements. The next component is the air supply unit, which can be a positive pressure blower or a vacuum pump, depending on the system configuration. The blower or pump generates the air flow necessary to move the material through the pipeline. The conveying line itself is typically made of stainless steel or other corrosion-resistant materials to ensure hygiene and durability, especially in food processing applications. The system may also include a filter or cyclone separator at the discharge end to separate the material from the air and return the air to the blower for recirculation. Control valves and sensors are integrated into the system to monitor and regulate the flow of material and air, ensuring consistent performance and preventing issues like blockages or overpressure. Each component is carefully selected and designed to work in harmony, ensuring the system operates smoothly and efficiently.
About HeadPowder: Experts in Pneumatic Conveying Solutions
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer and supplier of pneumatic conveying systems, including specialized equipment for cereal transport. With operations based in Shandong, China, the company has established itself as a trusted provider of high-quality, reliable equipment tailored to the needs of the food and agricultural industries. HeadPowder’s expertise lies in the design, manufacturing, and installation of customized pneumatic conveying systems that meet stringent hygiene and efficiency standards. The company’s products are engineered to handle a wide range of cereal types, from wheat and corn to oats and rice, ensuring that materials are transported safely and efficiently while maintaining product quality. The company’s commitment to innovation and customer satisfaction has made it a preferred choice for businesses seeking robust and effective pneumatic conveying solutions. HeadPowder’s team of experienced engineers and technicians work closely with clients to understand their specific operational needs and provide tailored solutions that enhance productivity and reduce downtime.