

Cocoa Pneumatic Conveying System Equipment: Exploring Its Function and Design Principles
When it comes to efficiently transporting cocoa powder and other fine bulk materials, the cocoa pneumatic conveying system equipment emerges as a vital solution in the processing industry. This technology offers a reliable and hygienic method for moving powders from one location to another, ensuring minimal product degradation and maintaining high standards of cleanliness. Understanding the components and design principles behind this system is crucial for industries that rely on consistent and efficient material handling.
Understanding the Cocoa Pneumatic Conveying System
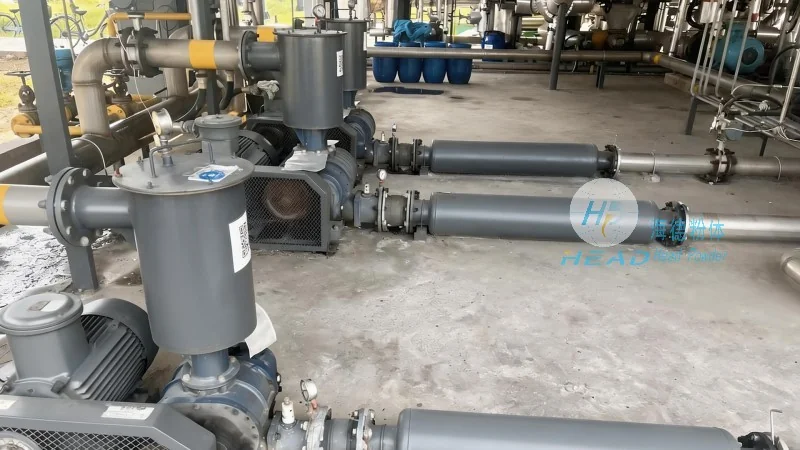
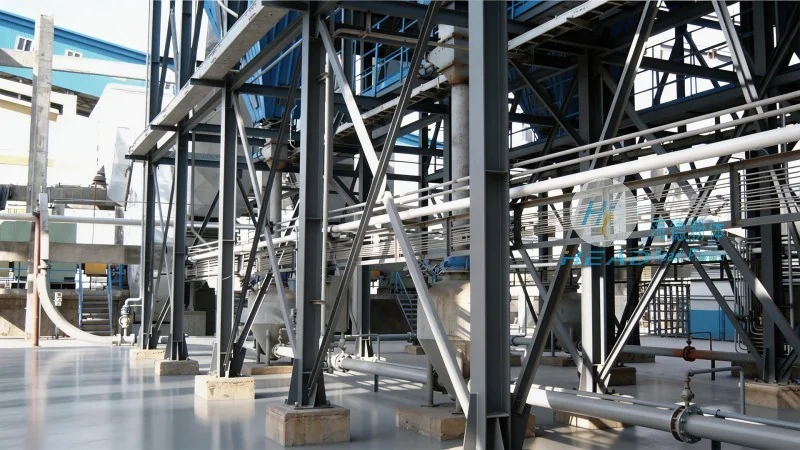
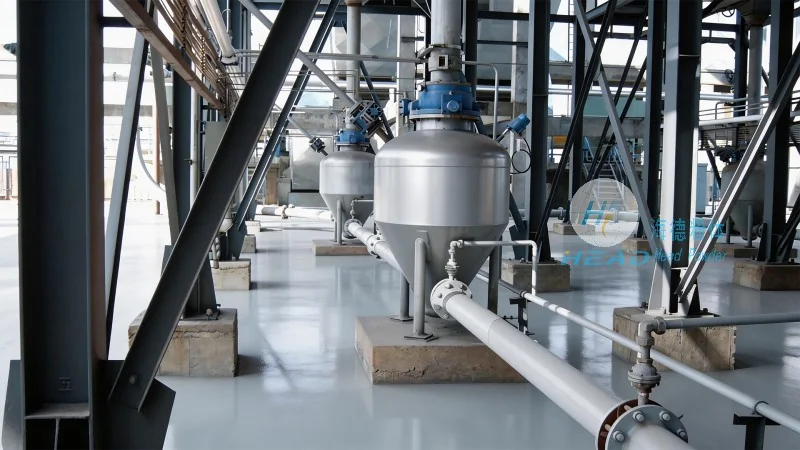
The cocoa pneumatic conveying system equipment is designed to transport dry, free-flowing materials like cocoa powder through a pressurized or vacuum system. At the core of this technology are key components such as the hopper, feeder, conveying line, and receiver. The hopper serves as the storage container, while the feeder regulates the flow of material into the system. The conveying line, often made of stainless steel or other corrosion-resistant materials, transports the material under pressure or suction. The receiver collects the material at the destination, ensuring it is delivered without spillage or contamination.
Design Principles of the System
The design of a cocoa pneumatic conveying system is guided by several critical principles to ensure optimal performance. First, the system must maintain a consistent pressure or vacuum level to prevent material blockages and ensure smooth flow. This is achieved through the use of appropriate air compressors or vacuum pumps, which are matched to the material's characteristics and the system's capacity. Second, the system's components are engineered to handle the specific properties of cocoa powder, such as its fine particle size and potential for caking. This includes using materials that resist corrosion and are easy to clean, which is essential for maintaining food safety standards. Third, the system is designed for scalability, allowing it to adapt to varying production volumes and processing needs. By integrating sensors and control systems, the equipment can automatically adjust its operation, enhancing efficiency and reducing downtime.
Key Features and Benefits
HeadPowder, a leading manufacturer of industrial conveying equipment, specializes in developing customized solutions for the cocoa industry. Their cocoa pneumatic conveying system equipment is engineered with features that address the unique challenges of handling cocoa powder. These include advanced filtration systems to prevent dust accumulation, which not only improves air quality but also extends the life of the system components. The equipment also incorporates easy-to-clean designs, with smooth surfaces and removable parts that facilitate regular maintenance. This ensures that the system remains hygienic and compliant with food safety regulations. Additionally, the system's energy efficiency is optimized through the use of variable frequency drives, which adjust the motor speed based on the material flow, reducing energy consumption and operational costs.
Application in Cocoa Processing
In the cocoa processing industry, the cocoa pneumatic conveying system plays a crucial role in various stages of production. From the initial grinding of cocoa beans to the final packaging of cocoa powder, this equipment ensures that materials are moved safely and efficiently. For example, in a cocoa powder production line, the system can transport ground cocoa from the grinding mill to the drying and sieving stages without the need for manual handling. This not only improves productivity but also reduces the risk of product contamination and worker exposure to dust. The system's ability to handle fine powders also makes it suitable for applications such as blending different cocoa varieties or adding flavorings, where precise control over material flow is essential.
Customization and Support from HeadPowder
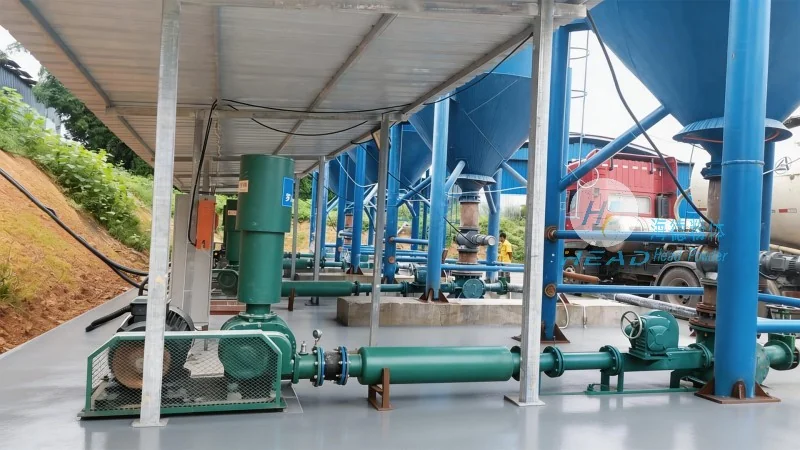
Shandong HeadPowder Engineering Co., Ltd., based in China, offers tailored solutions to meet the specific needs of cocoa processing facilities. Their team of engineers works closely with clients to understand their production requirements and design a system that maximizes efficiency and minimizes downtime. The company provides comprehensive support, including installation, training, and maintenance services, ensuring that the equipment operates at peak performance. By leveraging their expertise in pneumatic conveying technology, HeadPowder helps cocoa manufacturers enhance their operational capabilities and maintain high standards of quality and safety.