

What is a Small Bag Powder Conveying System and Its Design Principles?
When it comes to handling and transporting bulk powders efficiently, the small bag powder conveying system has emerged as a critical solution in various industrial sectors. This equipment is specifically designed to handle powders in small bag formats, offering a flexible and cost-effective method for material transfer. Understanding the components and design principles behind such systems is essential for industries that rely on consistent and reliable powder handling processes.
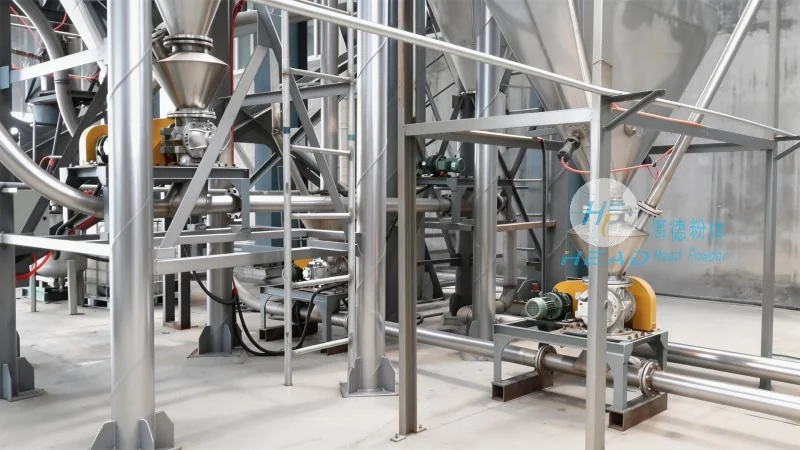
Introduction to Small Bag Powder Conveying Systems
At the core of the small bag powder conveying system is the ability to transfer powders from one location to another using small, portable bags. These systems are particularly advantageous in applications where powders are stored in bags and need to be moved to processing or storage areas without the need for large-scale bulk handling equipment. The system typically includes components such as bag openers, feeders, conveyors, and dust collection systems, all working in tandem to ensure a smooth and efficient powder transfer process.
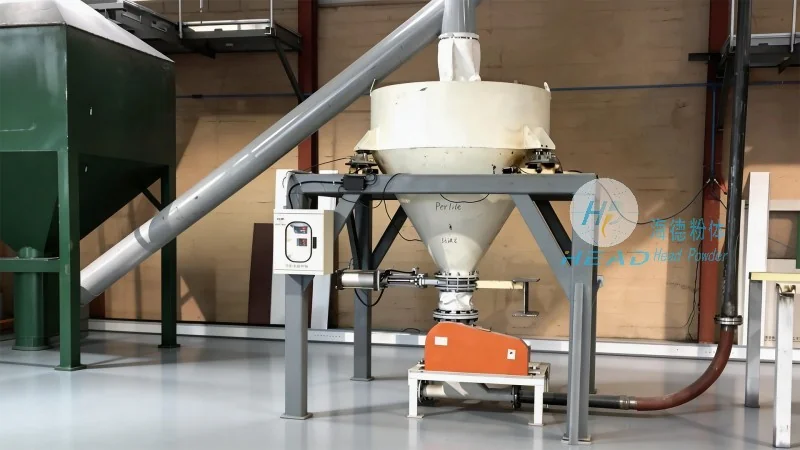
Key Components of the Small Bag Powder Conveying System
The effectiveness of a small bag powder conveying system is largely determined by its key components. The first component is the bag opener, which is responsible for safely and efficiently opening the small bags to release the powder. This component must be designed to handle various bag materials and sizes without damaging the powder or the bag itself. Next, the feeder is a critical part of the system, as it regulates the flow of powder from the bag into the conveyor. The feeder ensures a consistent and controlled flow, preventing overloading or underloading of the conveyor. The conveyor itself is the heart of the system, responsible for transporting the powder from the feeder to the destination. It can be a belt conveyor, screw conveyor, or pneumatic conveyor, depending on the specific requirements of the application. Finally, the dust collection system is essential for maintaining a clean and safe working environment. It captures any airborne particles and returns them to the system or filters them out, ensuring compliance with environmental regulations and worker safety standards.
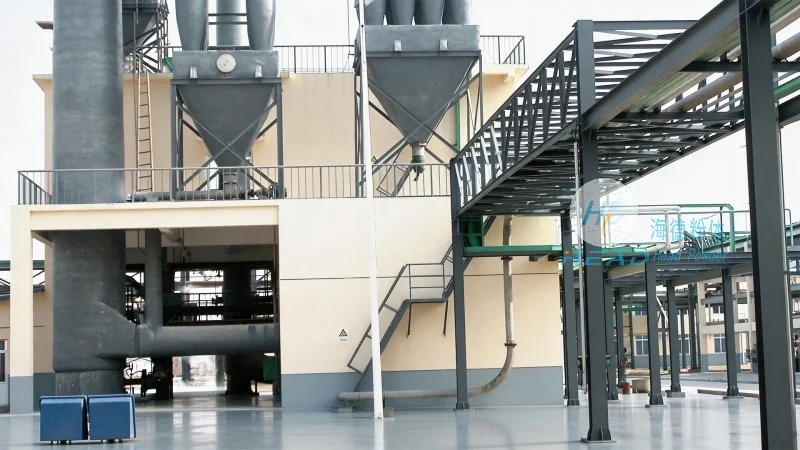
Design Principles Behind the Small Bag Powder Conveying System
The design principles of a small bag powder conveying system are centered around efficiency, safety, and adaptability. Efficiency is achieved through the integration of all components to minimize downtime and maximize material throughput. The system is designed to handle a wide range of powder types, from fine powders to coarse materials, without compromising performance. Safety is a top priority, with features such as dust suppression, proper ventilation, and secure bag handling mechanisms. Adaptability is another key principle, as the system can be customized to fit different bag sizes, powder characteristics, and operational requirements. The design also considers the need for easy maintenance and cleaning, ensuring that the system remains operational over its lifespan.
Applications and Benefits of the Small Bag Powder Conveying System
Small bag powder conveying systems are widely used in various industries, including pharmaceuticals, food processing, chemicals, and construction. In the pharmaceutical industry, these systems are used to handle active pharmaceutical ingredients (APIs) and excipients, ensuring that the powder is transferred without contamination. In food processing, they are used to handle ingredients like flour, sugar, and spices, maintaining the quality and purity of the product. In the chemical industry, they are used to handle raw materials and intermediates, providing a safe and efficient method for material transfer. The benefits of using such systems include reduced labor costs, improved safety, increased throughput, and better material handling efficiency. Additionally, the system reduces the risk of product contamination and damage, which is crucial in industries where product quality is paramount.
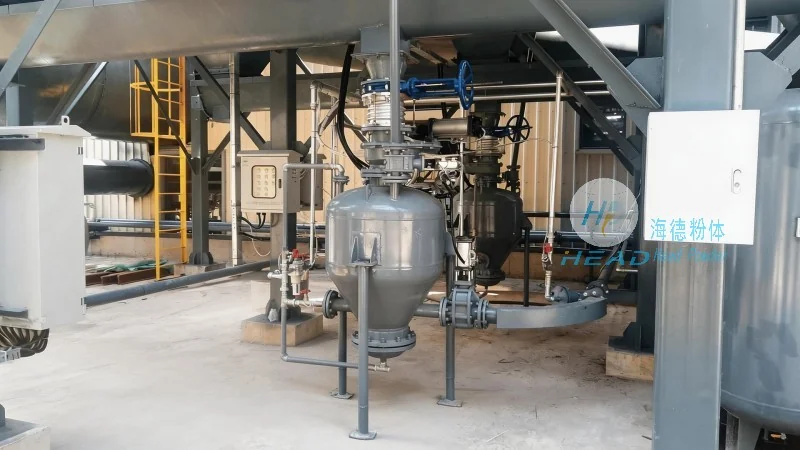
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of small bag powder conveying systems and related equipment. With years of experience in the industry, the company specializes in designing and manufacturing high-quality systems that meet the specific needs of its clients. The company's headquarters is located in Shandong, China, where it has a state-of-the-art manufacturing facility and a team of experienced engineers and technicians. The company is committed to providing reliable and efficient solutions for powder handling, ensuring that its clients can operate their processes with minimal downtime and maximum productivity. Shandong HeadPowder Engineering Co., Ltd. adheres to international quality standards and provides comprehensive after-sales support to its customers, ensuring that the systems are maintained and operated correctly.