

What is a Sugar Powder Conveying System Equipment? And What Are Its Design Principles?
Welcome to Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer specializing in advanced powder handling solutions. In this article, we will explore the concept of a sugar powder conveying system equipment and delve into its fundamental design principles, which are crucial for efficient and reliable sugar transportation in various industrial applications.
Understanding the Sugar Powder Conveying System Equipment
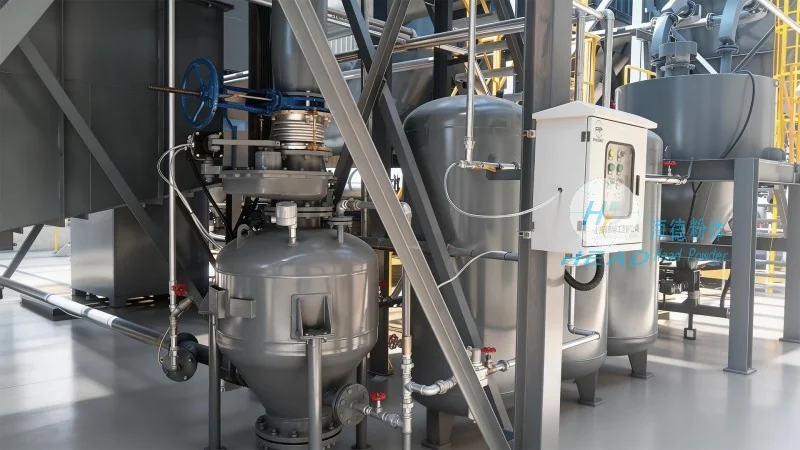
A sugar powder conveying system equipment is a specialized piece of machinery designed to transport granular or powdered sugar from one location to another within a processing facility. This system is essential in the sugar industry, as it ensures the smooth and safe movement of sugar, which is a critical raw material in food production, pharmaceuticals, and other sectors. The equipment typically consists of components such as hoppers, conveyors, and control systems, all working in tandem to achieve optimal performance.
Key Components of the System
The core components of a sugar powder conveying system include the feeding hopper, which holds the sugar and regulates the flow rate; the conveyor mechanism, which can be either pneumatic or mechanical, depending on the system design; and the discharge hopper, which delivers the sugar to the next stage of processing. Additionally, the system may incorporate sensors and control panels to monitor and adjust the conveying process in real-time, ensuring consistent and efficient operation.
Design Principles for Efficient Conveying
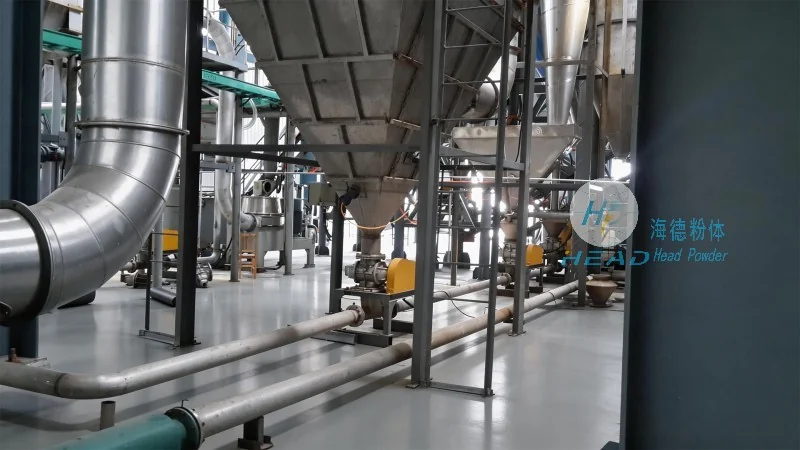
The design of a sugar powder conveying system is guided by several key principles aimed at maximizing efficiency, minimizing product degradation, and ensuring safety. One of the primary principles is the prevention of material buildup and caking, which can occur due to moisture or temperature variations. To address this, the system is often equipped with anti-static features and temperature-controlled environments to maintain the quality of the sugar. Another critical principle is the reduction of product attrition and contamination, which is achieved through the use of smooth, non-abrasive surfaces and proper sealing mechanisms.
Advantages of Using a Sugar Powder Conveying System
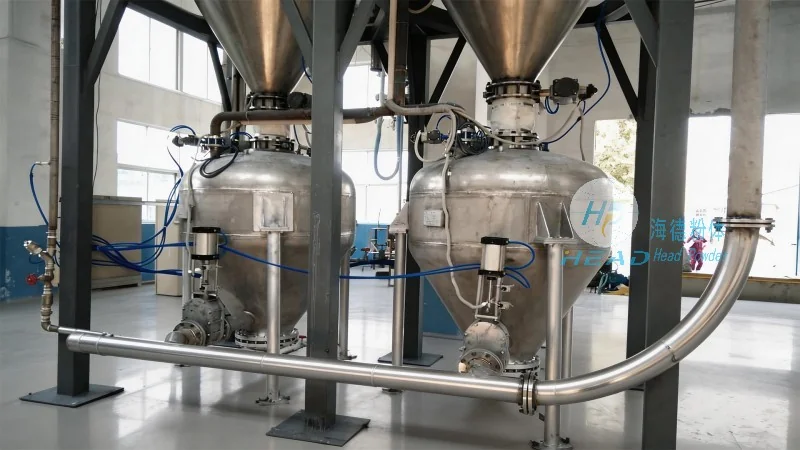
Implementing a well-designed sugar powder conveying system offers numerous advantages for industrial operations. Firstly, it enhances productivity by enabling continuous and automated sugar transportation, reducing labor costs and increasing throughput. Secondly, it improves product quality by minimizing exposure to air, moisture, and contaminants, which can affect the taste and shelf life of the sugar. Thirdly, it enhances safety by eliminating manual handling of bulk sugar, reducing the risk of accidents and exposure to dust. Finally, the system's modular design allows for easy integration with existing production lines, providing flexibility and scalability for growing businesses.
Applications in the Sugar Industry
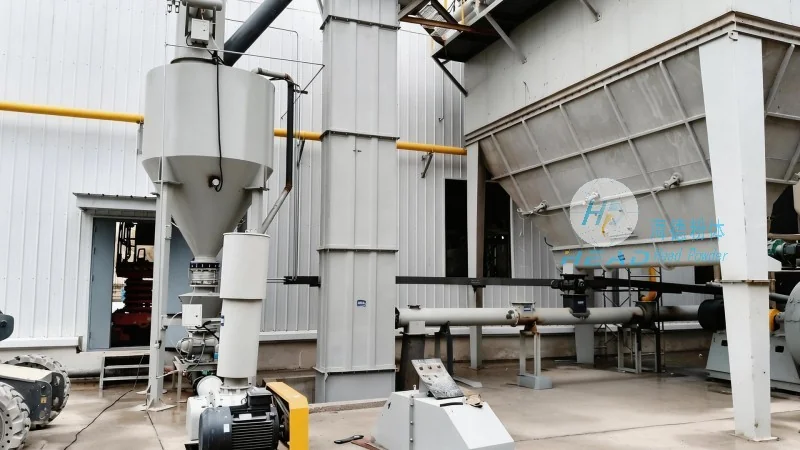
Sugar powder conveying systems are widely used in various applications within the sugar industry. In sugar refineries, these systems are used to transport raw sugar from storage silos to processing units, where it is further refined into white sugar or other sugar products. In food processing plants, they are employed to convey sugar into mixing and blending operations for the production of confectionery, beverages, and baked goods. Additionally, in pharmaceutical and chemical industries, the system is used to handle sugar as an excipient or raw material for various formulations.
Conclusion
In conclusion, a sugar powder conveying system equipment is a vital component in modern industrial operations, particularly in the sugar industry. Its design, which incorporates advanced engineering principles and components, ensures efficient, safe, and reliable transportation of sugar. By understanding the key design principles and advantages of such systems, businesses can optimize their operations, improve product quality, and enhance overall efficiency. Shandong HeadPowder Engineering Co., Ltd. is committed to providing high-quality powder handling solutions tailored to the specific needs of our clients, ensuring that their sugar conveying systems meet the highest standards of performance and reliability.