

High-Pressure Bin Pump Powder Conveying System Equipment: Exploring Its Function and Design Principl
High-pressure bin pump powder conveying systems represent a sophisticated technology designed to transport bulk powders and granular materials over long distances with high efficiency and reliability. These systems are integral to industries such as mining, chemical processing, food processing, and pharmaceuticals, where the safe and efficient movement of powders is critical for operational success. The core component of this system is the high-pressure bin pump, which operates on a principle of pressurized air or gas to create a flow of material through a pipeline network.
Understanding the High-Pressure Bin Pump
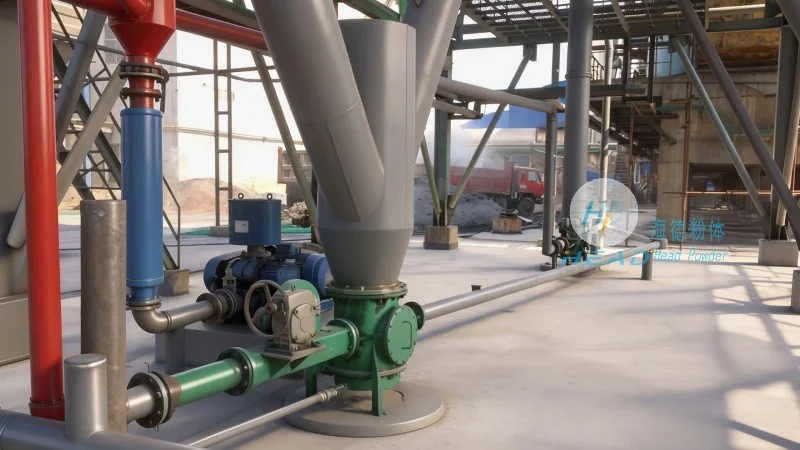
The high-pressure bin pump, often referred to as a pressure-type pump, is the heart of the powder conveying system. It functions by drawing material from a storage bin or hopper and pressurizing it to a high pressure before releasing it into the conveying line. This pump typically consists of a cylindrical chamber with a rotating or reciprocating mechanism that creates a vacuum or pressure differential to draw in material and then forces it out under high pressure. The design of the pump is optimized to handle abrasive and abrasive materials without causing excessive wear, ensuring long-term operational performance.
Design Principles of the Powder Conveying System
The design of a high-pressure bin pump powder conveying system is guided by several key principles aimed at maximizing efficiency, minimizing material degradation, and ensuring system reliability. First, the system must be capable of handling the specific characteristics of the material being conveyed, such as particle size, density, and flowability. Engineers select pump components, such as the impeller or plunger design, based on these material properties to ensure optimal performance. Second, the system incorporates a closed-loop or positive displacement mechanism to maintain consistent pressure and flow rates, preventing material backflow and ensuring a steady supply to the destination. Third, the design emphasizes energy efficiency by using high-pressure air or gas to minimize the need for additional mechanical components, reducing operational costs and environmental impact.
Key Components and Their Roles
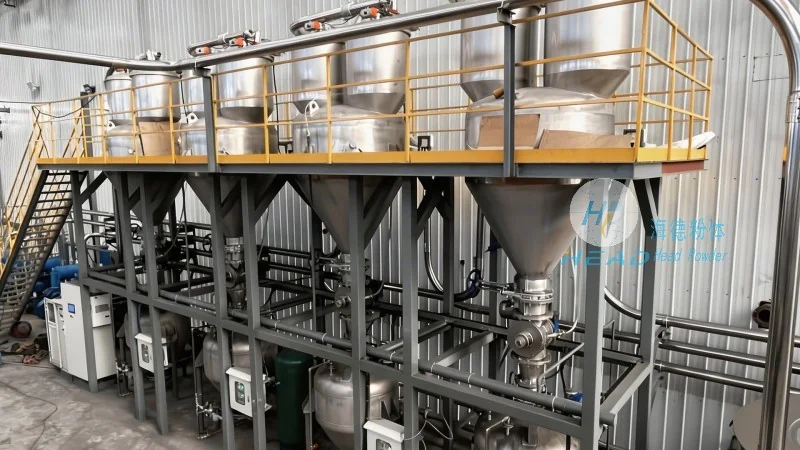
A high-pressure bin pump powder conveying system comprises several critical components that work in concert to achieve effective material transport. The storage bin or hopper serves as the initial container for the bulk material, providing a consistent feed to the pump. The high-pressure bin pump itself, as discussed earlier, is responsible for pressurizing and transporting the material. The conveying pipeline, typically made of durable materials like stainless steel or polyethylene, transmits the pressurized material from the pump to the discharge point. Additionally, the system includes control valves and pressure regulators to manage the flow and pressure, ensuring safe and controlled operation. These components are carefully selected and integrated to create a seamless system that meets the specific requirements of the application.
Applications and Benefits
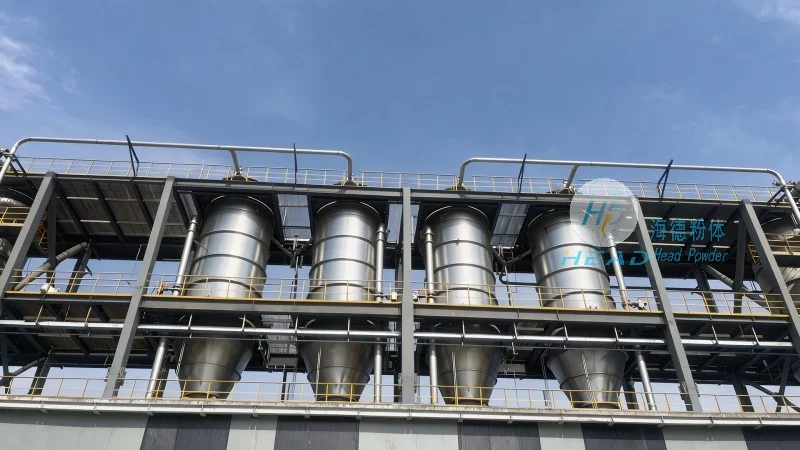
High-pressure bin pump powder conveying systems are widely used in various industrial applications due to their versatility and efficiency. In the mining industry, they are used to transport ore and other minerals from processing plants to storage facilities or for further processing. In chemical processing, these systems handle powders such as catalysts, pigments, and reagents, ensuring precise and controlled delivery to reactors and processing units. The food and pharmaceutical industries also rely on these systems for the safe and hygienic transport of ingredients and products, where contamination and material degradation must be strictly avoided. The benefits of using a high-pressure bin pump system include reduced labor costs, increased production efficiency, minimized material waste, and improved safety through the enclosed and pressurized transport process.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of high-quality powder handling equipment. With a strong focus on innovation and customer satisfaction, the company specializes in the design, development, and production of advanced powder conveying systems, including high-pressure bin pumps. HeadPowder's team of experienced engineers and technicians leverages cutting-edge technology and rigorous quality control processes to ensure that each product meets the highest industry standards. The company's commitment to excellence has earned it a reputation as a trusted partner for businesses seeking reliable and efficient powder handling solutions. HeadPowder's facilities are located in Shandong, China, where the company operates a state-of-the-art manufacturing plant equipped with modern equipment and advanced testing capabilities. This location allows the company to serve clients both domestically and internationally, providing timely and effective support for their powder handling needs.