

What is a Corn Kernels Powder Pneumatic Conveying System? And What Are Its Design Principles?
For industries dealing with corn kernels and other bulk materials, efficient material handling is crucial. A corn kernels powder pneumatic conveying system is a specialized equipment designed to transport corn kernels and similar granular or powdery materials through a pipeline using air pressure. This system offers a reliable and efficient method for moving materials without the need for mechanical components like belts or buckets, reducing wear and maintenance costs.
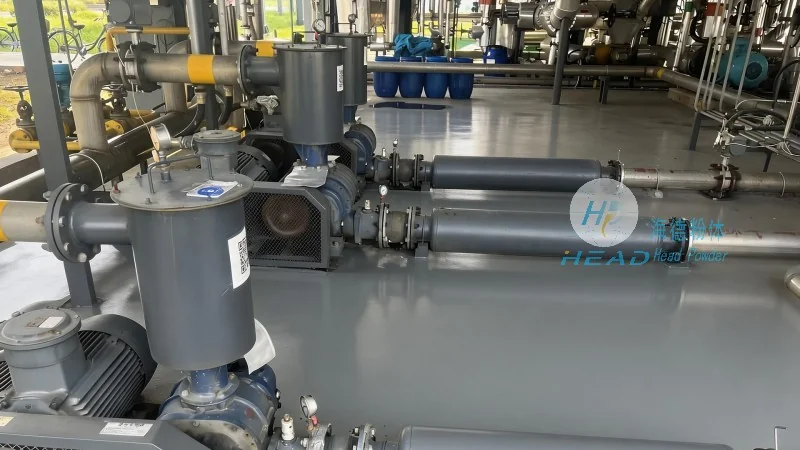
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of powder and bulk material handling, specializes in designing and manufacturing advanced pneumatic conveying systems. With a strong commitment to quality and innovation, HeadPowder provides tailored solutions for various industrial applications. The company is headquartered in Shandong, China, and serves clients globally with its expertise in material handling technology.
Understanding Corn Kernels Powder Pneumatic Conveying Systems
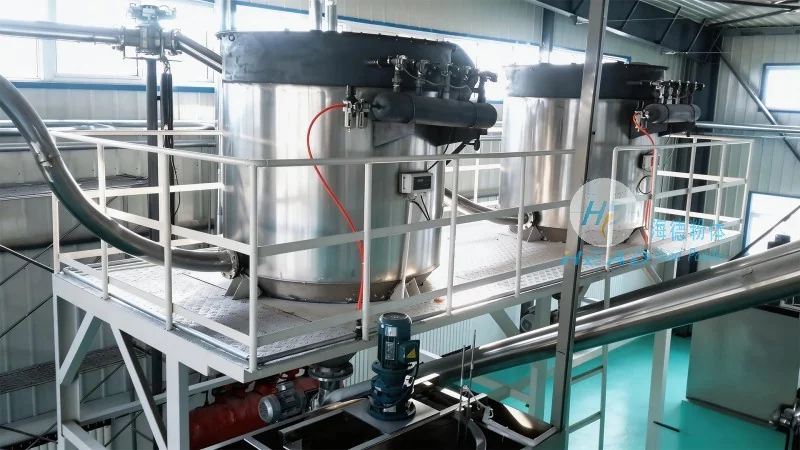
A corn kernels powder pneumatic conveying system is a type of pneumatic conveying equipment specifically engineered to handle corn kernels and other similar bulk materials. The system operates by using compressed air to create a flow that transports the corn kernels through a pipeline. This method is particularly effective for materials that are prone to dust, have high moisture content, or require gentle handling to prevent breakage. The system typically includes components such as a hopper, a feeder, a pipeline, and a receiver, all working in harmony to ensure smooth material transport.
The Design Principles Behind the System
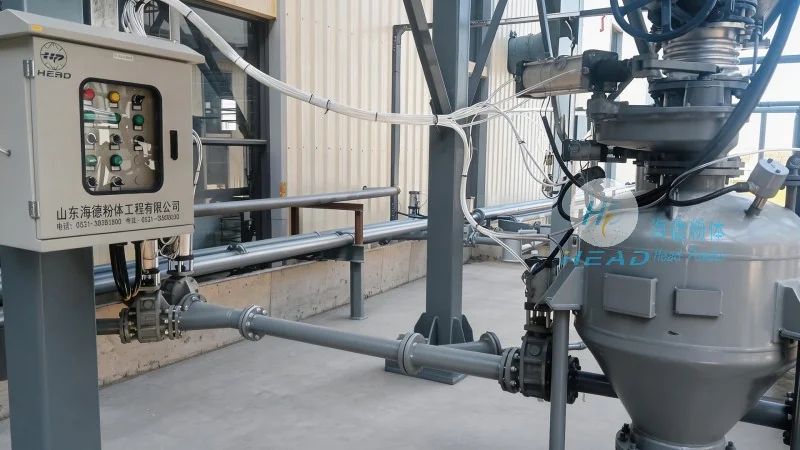
The design of a corn kernels powder pneumatic conveying system is based on several key principles to ensure optimal performance and efficiency. The first principle is the selection of the appropriate conveying method, which can be either pressure or vacuum-based. Pressure systems use compressed air to push the material through the pipeline, while vacuum systems use suction to draw the material. For corn kernels, a pressure system is often preferred as it provides better control over the material flow and can handle higher material loads. The second principle is the design of the hopper and feeder, which must be capable of feeding the corn kernels consistently and uniformly into the pipeline. The hopper is typically designed with a sloped bottom to prevent material bridging and ensure smooth discharge. The feeder, often a rotary valve or a star feeder, regulates the flow rate of the corn kernels into the pipeline. The third principle is the selection of the pipeline material and diameter. The pipeline must be made of materials that are resistant to corrosion and wear, such as stainless steel or polyethylene. The diameter of the pipeline is determined based on the material flow rate and the desired conveying velocity. The fourth principle is the design of the receiver, which is used to collect the conveyed corn kernels at the end of the pipeline. The receiver is typically equipped with a dust collection system to prevent material loss and maintain a clean working environment. The fifth principle is the integration of a control system to monitor and regulate the operation of the conveying system. This system allows operators to adjust the flow rate, pressure, and other parameters to optimize the performance of the system and ensure safe operation.
Key Advantages of the System
Implementing a corn kernels powder pneumatic conveying system offers several advantages over traditional mechanical conveying methods. One of the primary benefits is the reduction in material handling costs. By eliminating the need for mechanical components like belts or buckets, the system reduces wear and maintenance costs, leading to lower operational expenses. Another advantage is the improved material quality. The system provides gentle handling of the corn kernels, preventing breakage and maintaining the integrity of the material. This is particularly important for corn kernels, as broken kernels can affect the quality of the final product. The system also offers better control over the material flow, allowing for precise regulation of the flow rate and pressure. This ensures consistent material delivery and reduces the risk of material blockages or spills. Additionally, the system is more hygienic and easier to clean compared to traditional methods, making it suitable for food processing applications where cleanliness is critical. The system also provides a more compact and space-saving solution, as the pipeline can be installed in a variety of configurations to fit the available space in the facility.
Common Applications
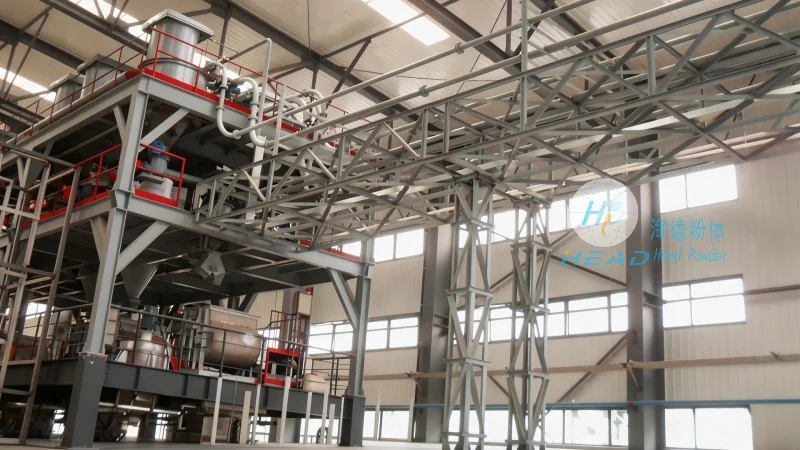
The corn kernels powder pneumatic conveying system is widely used in various industries that handle corn kernels and other bulk materials. Some common applications include the food processing industry, where the system is used to transport corn kernels from storage to processing equipment. The system is also used in the agricultural industry for the transportation of corn kernels from farms to processing facilities. In the pharmaceutical industry, the system is used to transport corn kernels that are used as raw materials for the production of corn starch or other derivatives. The system is also used in the chemical industry for the transportation of corn kernels that are used as a raw material for the production of corn syrup or other products. Additionally, the system is used in the pet food industry for the transportation of corn kernels that are used as an ingredient in pet food products.
Conclusion
A corn kernels powder pneumatic conveying system is a highly efficient and reliable method for transporting corn kernels and other bulk materials. The system is designed based on several key principles, including the selection of the appropriate conveying method, the design of the hopper and feeder, the selection of the pipeline material and diameter, the design of the receiver, and the integration of a control system. The system offers several advantages over traditional mechanical conveying methods, including reduced material handling costs, improved material quality, better control over the material flow, and improved hygiene. The system is widely used in various industries, including food processing, agriculture, pharmaceuticals, chemicals, and pet food. With its ability to handle corn kernels gently and efficiently, the corn kernels powder pneumatic conveying system is an essential equipment for any facility that deals with bulk materials.