

Working Principle and Features of Dust Collector Pneumatic Conveying Equipment
Dust collector pneumatic conveying equipment is a critical component in industrial dust management systems, designed to efficiently collect and transport collected dust from dust collectors to storage or disposal locations. This equipment plays a vital role in maintaining air quality and ensuring the smooth operation of industrial processes. The following sections will delve into the working principle and key features of such systems, providing a comprehensive understanding for potential users and industry professionals.
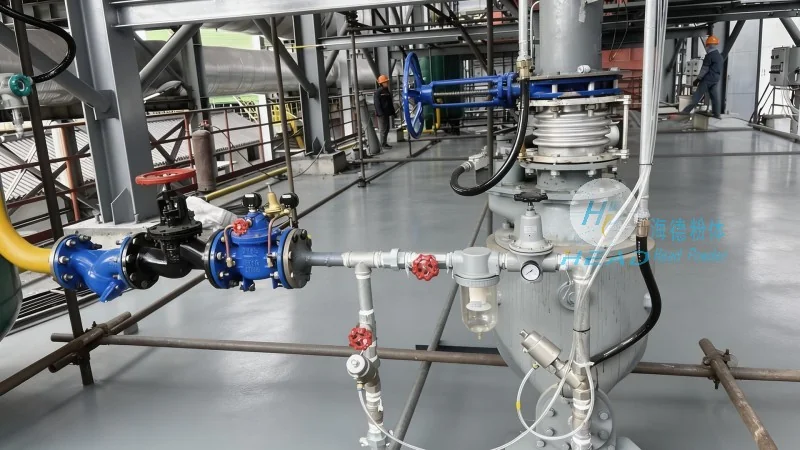
Working Principle of Dust Collector Pneumatic Conveying Equipment
The core mechanism of dust collector pneumatic conveying equipment revolves around the use of compressed air to transport particulate matter. Typically, the system consists of several key components: a dust collector that captures airborne dust, a compressed air source (such as an air compressor), a conveying pipeline network, and a receiver or storage unit. The process begins when the dust collector traps dust particles, which are then transferred to the conveying system. Compressed air is introduced into the pipeline, creating a flow that propels the dust particles through the system. The air flow can be either positive pressure (where air pushes the dust forward) or negative pressure (where air pulls the dust into the pipeline). The choice between these methods depends on the specific application, dust characteristics, and system layout. The equipment ensures that the dust is transported safely and efficiently, minimizing the risk of dust re-entrainment and ensuring compliance with environmental regulations.
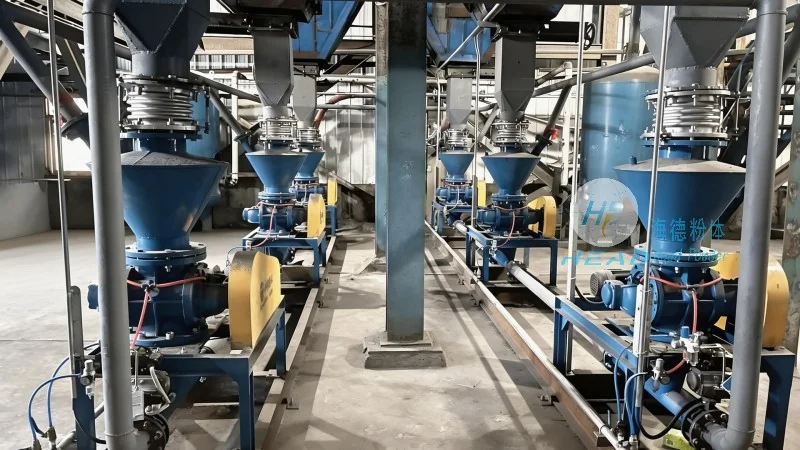
Key Features and Advantages of Dust Collector Pneumatic Conveying Equipment
Dust collector pneumatic conveying equipment offers several distinct advantages that make it a preferred choice in industrial settings. One of the primary features is its high efficiency in dust transport, as it can move large volumes of dust over significant distances with minimal energy consumption compared to traditional methods like manual handling or mechanical conveyors. The system is also highly flexible, allowing for easy integration with existing dust collection systems and adaptation to various industrial environments. Additionally, pneumatic conveying systems are capable of handling a wide range of dust types, including fine powders, coarse particles, and sticky materials, without causing blockages or system damage. Another notable feature is the ability to maintain a clean and dust-free environment, as the equipment operates with enclosed pipelines, preventing dust from escaping into the workplace and reducing the risk of respiratory hazards for workers. The system also contributes to improved operational safety by eliminating the need for manual handling of heavy or hazardous dust loads, thereby reducing the risk of accidents and injuries.
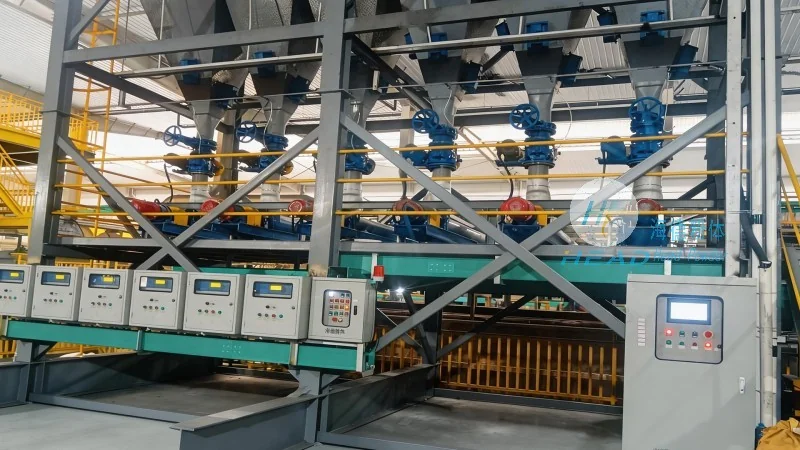
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of dust collector pneumatic conveying equipment. With a strong commitment to quality and innovation, the company has established itself as a trusted partner in the industrial dust management sector. HeadPowder's products are designed to meet the diverse needs of various industries, including manufacturing, mining, and construction, where efficient dust control is essential for operational efficiency and environmental compliance. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with advanced technology and skilled workforce. HeadPowder's team of engineers and technicians is dedicated to developing and manufacturing high-performance pneumatic conveying systems that deliver reliable performance and long service life. The company adheres to strict quality control standards to ensure that each product meets or exceeds industry specifications and customer expectations. Through continuous research and development, HeadPowder remains at the forefront of dust management technology, providing solutions that enhance productivity and safety in industrial operations.
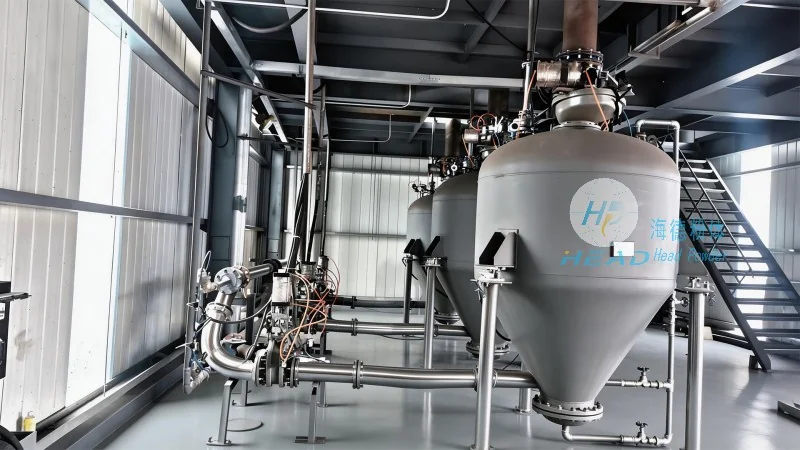
Conclusion
In summary, dust collector pneumatic conveying equipment is a sophisticated and efficient solution for managing industrial dust, combining advanced technology with practical design to address the challenges of dust transport and disposal. The working principle, which relies on compressed air to move dust particles through a closed system, ensures high efficiency and minimal environmental impact. The key features of these systems, including flexibility, versatility, and safety, make them indispensable in modern industrial settings. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. continues to deliver high-quality pneumatic conveying equipment that meets the evolving needs of industries worldwide, contributing to cleaner, safer, and more productive work environments.