

Working Principle and Features of Calcium Carbonate Pneumatic Conveying Equipment
Calcium carbonate, a widely used industrial material, is often transported using pneumatic conveying systems. These systems are essential for efficient material handling in various industrial applications. The following article explores the working principle and key features of calcium carbonate pneumatic conveying equipment, highlighting the technology's efficiency and reliability.

About HeadPowder: Your Trusted Partner in Material Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, is a leading manufacturer specializing in the design and production of advanced material handling equipment. With years of experience in the industry, HeadPowder has established itself as a reliable partner for businesses seeking efficient and durable pneumatic conveying solutions. The company's commitment to quality and innovation ensures that its products meet the highest standards of performance and safety.
The Working Principle of Calcium Carbonate Pneumatic Conveying Machines
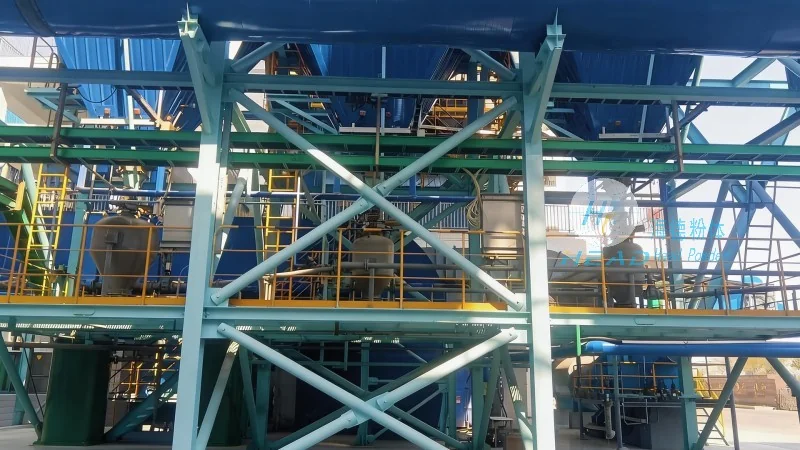
Calcium carbonate pneumatic conveying systems operate on the principle of using air or gas to transport bulk materials through a pipeline. The process typically involves several key components and steps. First, the material is fed into a hopper or feeder, where it is then introduced into the conveying line. A fan or blower generates the necessary air pressure, creating a flow that propels the material through the pipeline. The system may include various components such as a separator, filter, and receiver to ensure efficient material transfer and minimize dust emissions. The entire process is designed to handle calcium carbonate with precision, ensuring minimal product degradation and optimal throughput.
Key Features and Advantages of Calcium Carbonate Pneumatic Conveyors
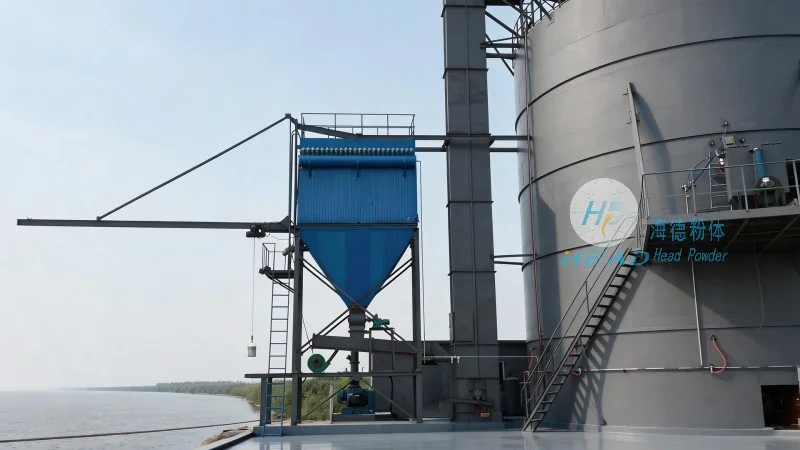
Calcium carbonate pneumatic conveying equipment from HeadPowder offers several distinct advantages that make it ideal for industrial applications. One of the primary features is its ability to handle fine or powdery materials like calcium carbonate without clogging or loss of material. The system's design minimizes product degradation, preserving the quality of the material during transport. Additionally, the equipment is highly efficient, with low energy consumption and minimal maintenance requirements. The use of advanced materials and engineering ensures durability and long service life, reducing downtime and operational costs. Another key feature is the system's flexibility, allowing for easy integration into existing production lines and adaptation to varying material flow rates. The equipment also provides excellent dust control, contributing to a safer and cleaner working environment. These features collectively make calcium carbonate pneumatic conveyors a preferred choice for industries requiring reliable and efficient material handling solutions.
Conclusion and Application Scope
Calcium carbonate pneumatic conveying machines, as exemplified by the products from Shandong HeadPowder Engineering Co., Ltd., represent a sophisticated solution for the efficient transport of calcium carbonate. By leveraging pneumatic conveying technology, these systems offer significant advantages in terms of efficiency, reliability, and environmental friendliness. The working principle, which relies on air pressure to move material through pipelines, combined with advanced design features, ensures optimal performance in various industrial settings. As a leading manufacturer based in Shandong, China, HeadPowder continues to innovate and provide high-quality material handling equipment that meets the evolving needs of the industry. Whether for small-scale or large-scale operations, calcium carbonate pneumatic conveying equipment from HeadPowder is a reliable choice for businesses seeking to enhance their material handling processes.