

Working Principle and Features of Coal Ash Powder Conveying Systems
Coal ash, a byproduct of coal combustion in thermal power plants, poses significant challenges in handling and transportation due to its fine particle size and potential for dust generation. The coal ash powder conveying system is designed to address these challenges efficiently, ensuring safe and reliable transport of coal ash from its source to disposal or utilization sites. This article explores the working principle and key features of such systems, highlighting their importance in modern industrial operations.
Working Principle of Coal Ash Powder Conveying Systems
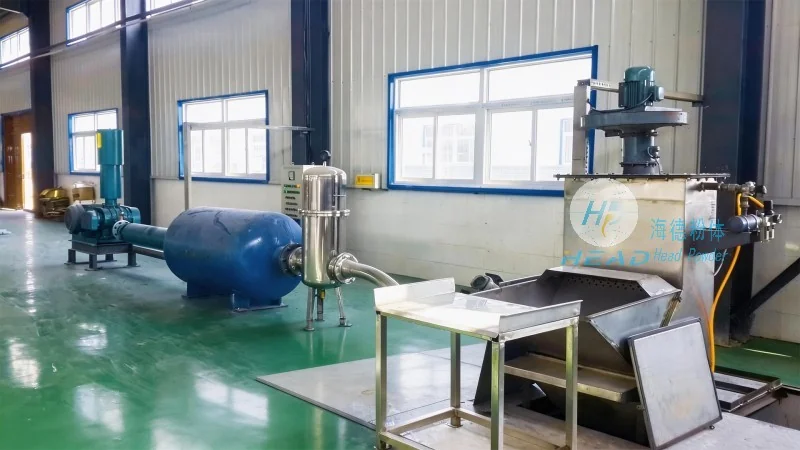
The core of a coal ash powder conveying system lies in its ability to handle fine, dry powders like coal ash without clogging or degradation. The system typically operates on the principle of pneumatic or mechanical transport, with pneumatic systems being more common for coal ash due to their effectiveness in handling dusty materials. A typical pneumatic conveying system for coal ash consists of several key components: a hopper for material storage, a feeder to control the flow rate, a conveying line (often made of stainless steel or other corrosion-resistant materials), and a receiver at the destination. The process begins when coal ash is fed from the hopper into the conveying line. In pneumatic systems, compressed air is introduced into the line, creating a flow that propels the ash particles through the system. The air and ash mixture travels through the pipeline, with the air pressure maintaining the flow and preventing the ash from settling. At the receiving end, the air is separated from the ash, often using a cyclone separator or a filter, and the ash is deposited into the designated container. Mechanical conveying systems, such as screw conveyors or belt conveyors, may also be used for coal ash transport, especially in applications where the ash is more cohesive or contains larger particles. These systems rely on mechanical force to move the ash through the conveyor, with the material being pushed or pulled along the path. Both pneumatic and mechanical systems are designed to handle the specific properties of coal ash, including its low bulk density and tendency to form agglomerates, ensuring consistent and reliable operation.
Key Features of Coal Ash Powder Conveying Systems
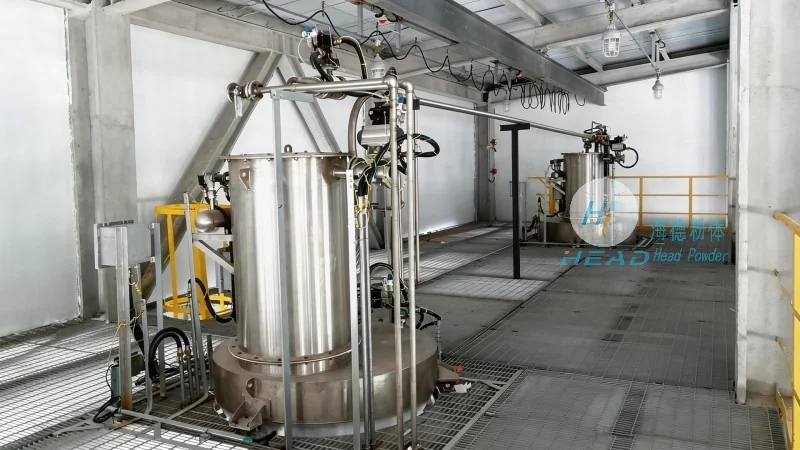
Coal ash powder conveying systems are characterized by several features that make them suitable for industrial applications. One of the primary features is their high efficiency in transporting large volumes of material over long distances. Pneumatic systems, in particular, can convey coal ash at high speeds, reducing the time and labor required for transport. This efficiency is crucial for thermal power plants, which generate substantial amounts of coal ash daily and need to dispose of it quickly to maintain operational capacity. Another important feature is the system's ability to maintain the quality of the coal ash during transport. Coal ash is often used in applications like cement production or road construction, where its quality is critical. The conveying system must prevent the ash from being contaminated or degraded, which could affect its performance in downstream processes. This is achieved through the use of corrosion-resistant materials for the conveying line and proper air filtration to remove any dust or contaminants. Safety is also a key feature of coal ash powder conveying systems. Coal ash can be a respiratory hazard if inhaled, and the system is designed to minimize dust generation and exposure to workers. Pneumatic systems, for example, use enclosed pipelines and proper ventilation to keep dust levels low. Additionally, the system is equipped with safety features such as pressure relief valves and emergency shut-off mechanisms to prevent accidents. The adaptability of the system is another notable feature. Coal ash can vary in composition and particle size depending on the type of coal burned and the combustion conditions. The conveying system is designed to handle a wide range of ash properties, with adjustable settings for flow rate and air pressure to accommodate different ash types. This flexibility allows the system to be used in various applications, from short-distance transport within a power plant to long-distance transport to off-site disposal sites. The system's durability is also a significant feature. Coal ash is abrasive and can cause wear on the conveying components. The system is constructed with high-quality materials, such as stainless steel and wear-resistant coatings, to withstand the abrasive nature of the ash and extend the service life of the equipment. Regular maintenance is also essential to ensure the system operates efficiently and safely over time.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
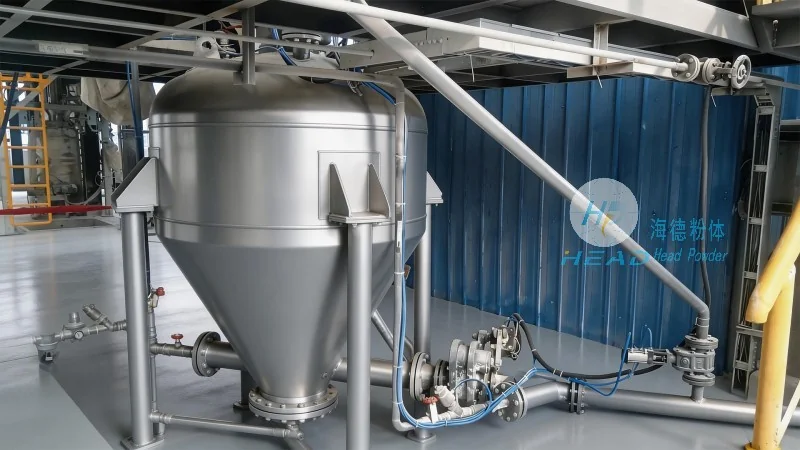
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of coal ash powder conveying systems and related industrial equipment. With a strong focus on innovation and quality, HeadPowder has established itself as a trusted partner for thermal power plants and other industrial facilities requiring efficient coal ash handling solutions. The company's headquarters is located in Shandong, China, where it has a dedicated team of engineers, technicians, and sales professionals. HeadPowder specializes in designing and manufacturing customized conveying systems tailored to the specific needs of its clients. Each system is engineered to meet the unique requirements of the application, including the volume of ash to be transported, the distance, and the environmental regulations. The company uses advanced technology and materials to ensure the highest standards of performance and reliability. HeadPowder's products are known for their durability, efficiency, and safety, making them a preferred choice for industrial operations. The company also provides comprehensive after-sales services, including installation, maintenance, and technical support, to ensure that its clients can operate their systems effectively and with minimal downtime. With a commitment to customer satisfaction and continuous improvement, HeadPowder has built a reputation for excellence in the coal ash handling industry. Its systems are widely used in thermal power plants across China and other countries, contributing to the efficient and safe management of coal ash as a valuable resource.