

Working Principle and Features of Sugar Powder Conveying Systems
Sugar powder conveying systems are essential in the food processing and industrial sectors, particularly for the efficient and safe handling of granular and powdered sugar. These systems are designed to transport sugar from storage silos or processing units to various points of use, such as blending, packaging, or further processing. The proper functioning of these systems is critical to maintaining product quality, ensuring operational efficiency, and complying with industry standards. In this article, we will explore the working principles and key features of modern sugar powder conveying systems, highlighting how they enhance productivity and reliability in sugar handling operations.
Working Principle of Sugar Powder Conveying Systems
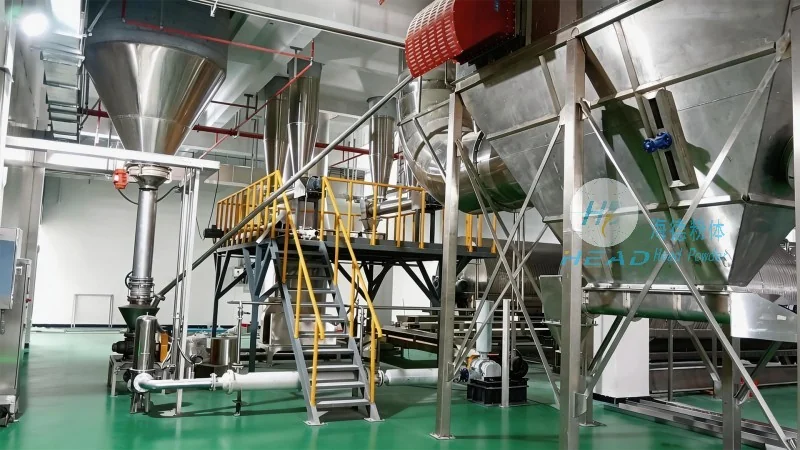
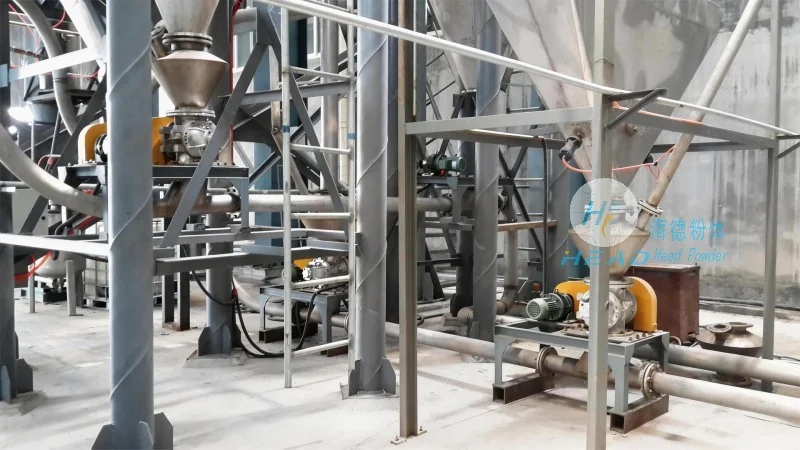
The core working principle of a sugar powder conveying system involves the use of specialized equipment to move bulk sugar powder through a closed or semi-closed system. The process typically begins with the storage of sugar in a silo or hopper, where the powder is held under controlled conditions to prevent caking or moisture absorption. From the storage vessel, the sugar is fed into a conveyor system, which may include components like rotary valves, screw conveyors, or pneumatic ducts, depending on the system design. The conveyor system uses mechanical or pneumatic forces to move the sugar powder through the pipeline network to the destination point. Control systems, often integrated with sensors and automation technology, regulate the flow rate, pressure, and direction of the sugar, ensuring precise and consistent delivery. This closed-loop system minimizes product exposure to contaminants and maintains hygiene standards, which is crucial for food-grade applications.
Key Features of Modern Sugar Powder Conveying Systems
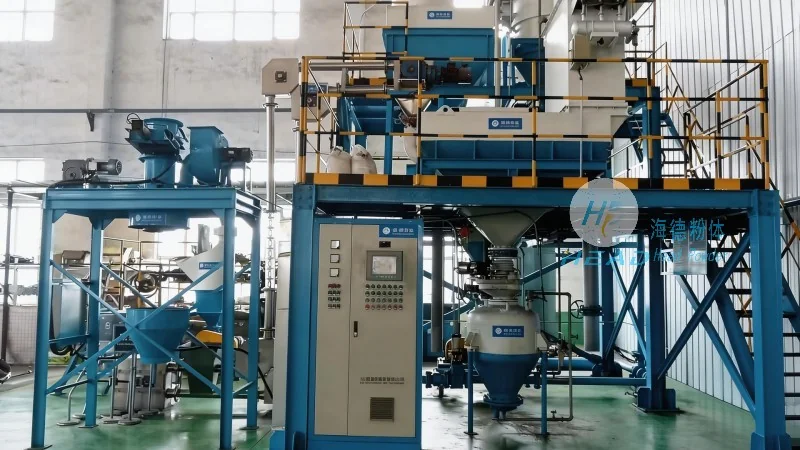
Modern sugar powder conveying systems are equipped with several advanced features that enhance their performance and reliability. One of the primary features is the use of high-quality materials, such as stainless steel or food-grade plastics, to construct the conveyor components. This ensures durability and resistance to corrosion, which is vital for handling sugar and other food products. Another important feature is the integration of advanced control technology, including programmable logic controllers (PLCs) and user-friendly interfaces. These controls allow operators to monitor and adjust the system parameters in real-time, optimizing the conveying process and reducing downtime. Additionally, many systems incorporate dust suppression and filtration systems to maintain a clean and safe working environment, preventing the spread of sugar dust and ensuring compliance with occupational health and safety regulations. The modular design of these systems also enables easy installation, maintenance, and scalability, allowing businesses to adapt the system to changing production needs without significant disruptions.
Advantages of Using a Professional Supplier: Shandong HeadPowder Engineering Co., Ltd.
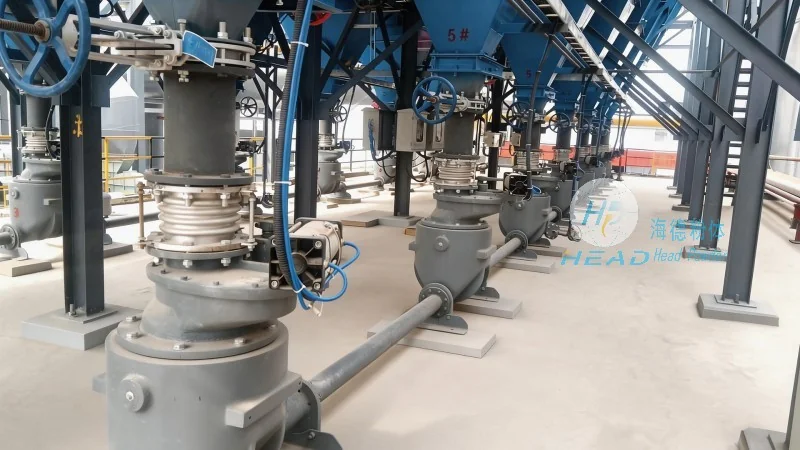
When selecting a sugar powder conveying system, partnering with a reputable supplier is essential to ensure the best performance and support. Shandong HeadPowder Engineering Co., Ltd., trading as headpowder, is a leading manufacturer and supplier of bulk material handling solutions, including specialized systems for sugar powder. With headquarters in Shandong, China, headpowder combines years of industry experience with cutting-edge technology to deliver high-quality, customized conveying systems tailored to the specific needs of sugar processing facilities. The company’s expertise lies in designing and manufacturing systems that meet the stringent requirements of the food industry, including hygiene standards, safety regulations, and operational efficiency. By choosing headpowder, clients benefit from comprehensive support, from initial system design and installation to ongoing maintenance and technical assistance. The company’s commitment to quality and customer satisfaction ensures that businesses can rely on their sugar powder conveying systems for long-term performance and reliability, ultimately enhancing their overall production capabilities and profitability.