

Working Principle and Features of Tonne Bag Unpacking Material Conveying Lines
For industrial facilities dealing with bulk materials, the tonne bag unpacking material conveying line is a critical piece of equipment designed to streamline the process of handling and transporting unpacked materials from large bags. This system, developed by Shandong HeadPowder Engineering Co., Ltd., integrates multiple functions, including automatic bag opening, material discharge, and subsequent conveying to storage or processing areas. The following sections will explore the working principle and key features of such a system, highlighting its operational efficiency and technical advantages.
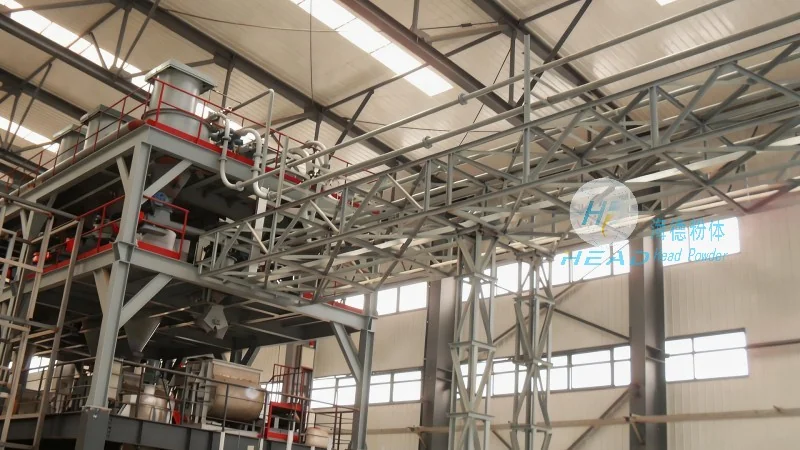
Working Principle of the Tonne Bag Unpacking Material Conveying Line
The tonne bag unpacking material conveying line operates through a series of coordinated mechanical and pneumatic processes. Initially, a tonne bag, typically containing bulk materials like chemicals, fertilizers, or powders, is positioned on a loading platform. The system then uses a pneumatic or mechanical bag opener to rupture the bag's seal, allowing the material to flow out. A hopper or chute collects the discharged material and feeds it into a conveyor system, which may include belt conveyors, screw conveyors, or pneumatic pipelines to transport the material to the desired location. Throughout this process, sensors and control systems monitor the flow rate, ensuring consistent and controlled material transfer. The entire operation is automated, reducing manual labor and minimizing the risk of material spillage or contamination.
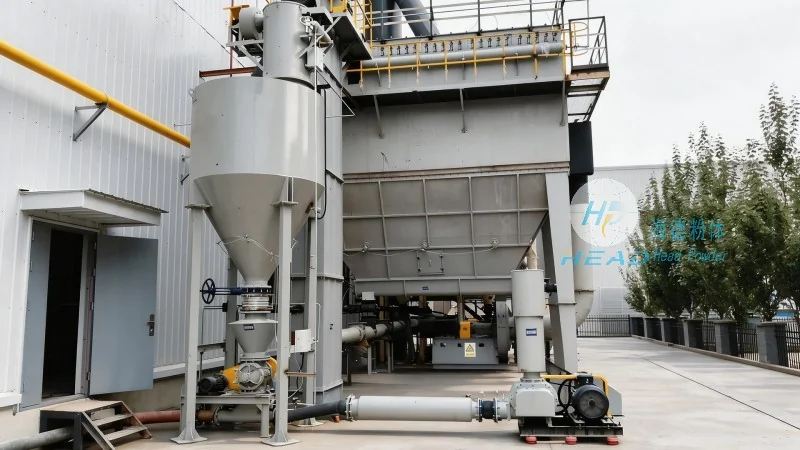
Key Features of the Tonne Bag Unpacking Material Conveying Line
Several notable features distinguish the tonne bag unpacking material conveying line, making it an ideal solution for various industrial applications. Firstly, the system is highly automated, with minimal human intervention required for bag handling and material transfer. This automation enhances operational efficiency and reduces labor costs. Secondly, it is designed for durability and reliability, using robust components that can withstand heavy-duty industrial environments. The equipment is also equipped with safety features, such as emergency stop buttons and overload protection, to ensure safe operation. Additionally, the conveying line can be customized to accommodate different bag sizes and material types, providing flexibility for diverse industrial needs. Energy efficiency is another key feature, as the system optimizes power usage through intelligent control systems, reducing operational costs. The integration of advanced sensors and control technology allows for real-time monitoring and adjustment of the conveying process, further improving performance and material handling accuracy.
Technical Specifications and Operational Capabilities
The technical specifications of the tonne bag unpacking material conveying line vary based on the specific design and application requirements. Typically, these systems can handle bag capacities ranging from 500 kg to 2 tonnes, with material flow rates adjustable to meet production demands. The conveyor components, such as belt width and speed, are tailored to the material's characteristics, ensuring smooth and efficient transport. For example, in applications involving fine powders, the system may include dust collection and filtration systems to maintain air quality and prevent material loss. The control system often incorporates programmable logic controllers (PLCs) that allow for easy programming and adjustment of operational parameters. This flexibility enables the system to adapt to changing production schedules or material types without significant downtime. The equipment is also designed for easy maintenance, with accessible components and modular design that simplifies repairs and replacements.
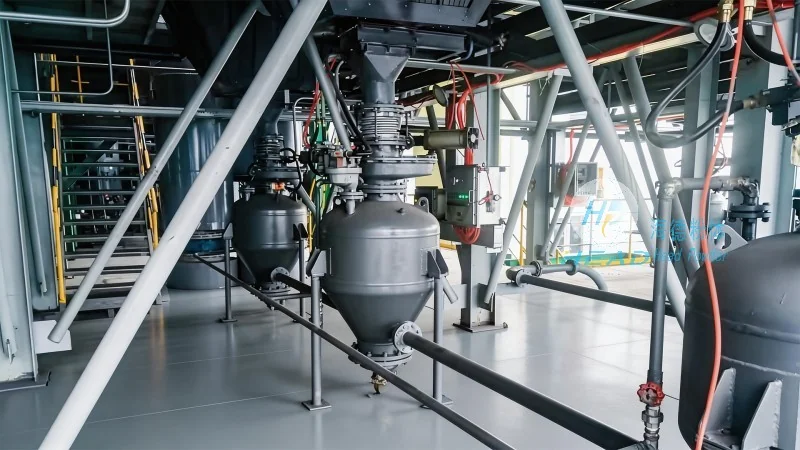
Application Scenarios and Industry Benefits
The tonne bag unpacking material conveying line is widely used in industries such as chemical manufacturing, fertilizer production, food processing, and mining. In chemical plants, it efficiently handles bulk chemicals, reducing the risk of exposure to hazardous materials during manual handling. In fertilizer production, the system streamlines the process of transferring raw materials to processing units, improving overall production throughput. The food processing industry benefits from the hygienic design of the equipment, which minimizes contamination risks and complies with food safety regulations. The mining sector uses the system to transport raw ores or minerals from storage to processing facilities, enhancing operational efficiency. Overall, the adoption of this conveying line leads to significant benefits, including increased productivity, reduced labor costs, improved material handling accuracy, and enhanced workplace safety. By automating the unpacking and conveying process, industrial facilities can achieve higher operational efficiency and better control over material flow, contributing to improved overall performance and profitability.