

Principle and Application Scenarios of Chromium Oxide Pneumatic Conveying Equipment
HeadPowder, a leading provider in the field of material handling solutions, specializes in the design and manufacturing of advanced pneumatic conveying systems. This article focuses on the principle and key application scenarios of chromium oxide pneumatic conveying equipment, highlighting its technical advantages and practical uses in industrial settings.
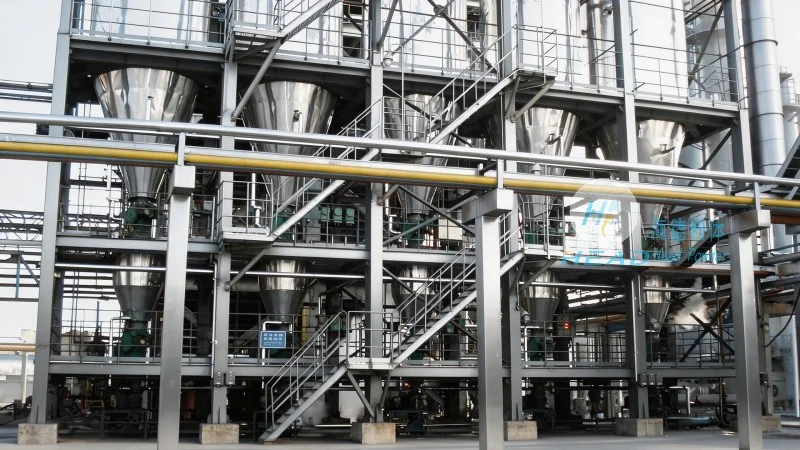
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for businesses seeking efficient and reliable material transport solutions. Our expertise lies in customizing pneumatic conveying systems to meet the unique demands of various industries, ensuring optimal performance and durability.
The Principle of Pneumatic Conveying for Chromium Oxide
Chromium oxide, a critical material in many industrial applications, requires specialized handling due to its properties and potential hazards. Pneumatic conveying systems offer a safe and efficient method for transporting this material. The core principle involves using compressed air to move the material through a pipeline system. The process typically involves a hopper where the material is fed into the system, followed by the introduction of air to create a flow. The air velocity is carefully controlled to ensure the material is transported without degradation or damage. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and operational costs.
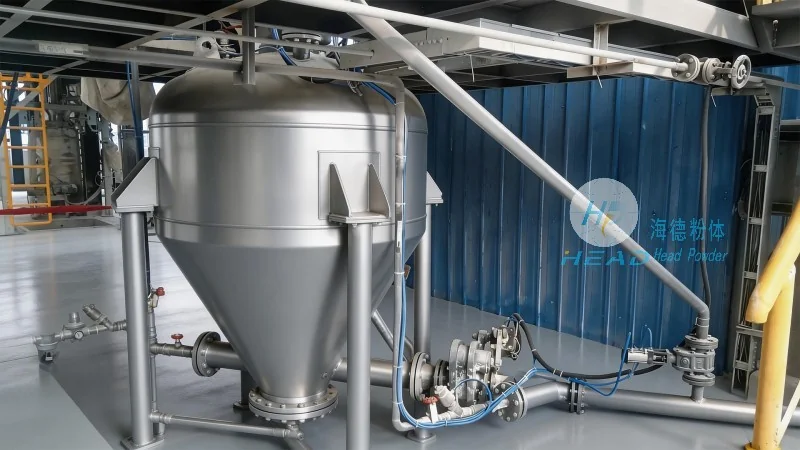
Key Features and Technical Advantages
Chromium oxide pneumatic conveying equipment from HeadPowder is engineered with several key features that enhance performance and reliability. The system utilizes high-efficiency air pumps and precise control mechanisms to maintain consistent air pressure and flow rates. This ensures smooth material transport and minimizes the risk of blockages or material degradation. Additionally, the equipment is designed with corrosion-resistant materials to handle the chemical properties of chromium oxide, extending its service life. The modular design allows for easy installation and maintenance, making it suitable for both new and existing industrial facilities.
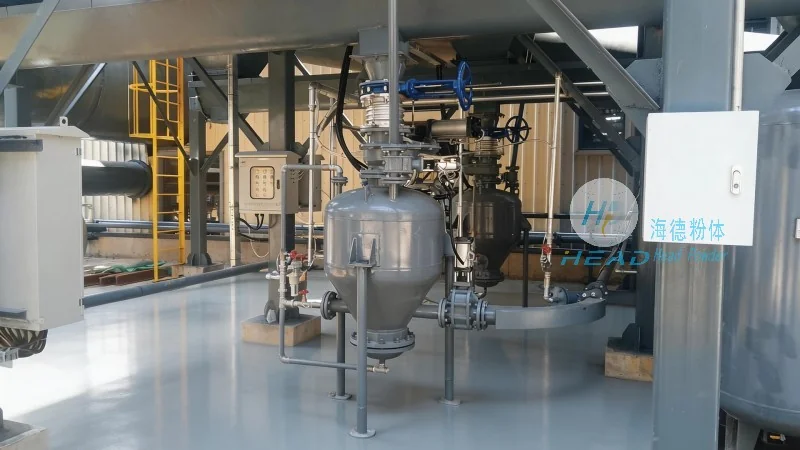
Application Scenarios and Industrial Uses
The versatility of chromium oxide pneumatic conveying systems makes them suitable for a wide range of applications. In the chemical industry, these systems are used to transport chromium oxide in the production of pigments and coatings. The food and pharmaceutical sectors also benefit from this technology, as it provides a hygienic and dust-free method for handling materials. Additionally, in the manufacturing of electronic components, the precise control of material flow is crucial, and pneumatic conveying systems meet these requirements effectively. The equipment is also used in research and development laboratories where accurate and controlled material transport is essential for experimental processes.
Benefits for Industrial Operations
Implementing chromium oxide pneumatic conveying equipment brings several benefits to industrial operations. Firstly, it improves safety by eliminating the need for manual handling of potentially hazardous materials. The enclosed system reduces exposure to dust and fumes, protecting both workers and the environment. Secondly, it enhances efficiency by reducing downtime and maintenance costs. The automated nature of the system ensures consistent performance, leading to higher productivity. Finally, the system’s adaptability allows it to be integrated into existing production lines with minimal disruption, making it a cost-effective solution for businesses looking to upgrade their material handling processes.