

Principle and Working Scenarios of Bin Pump Material Handling
Bin pumps are critical equipment in bulk material handling systems, designed to transport powders and granular materials with high efficiency and reliability. Understanding the underlying principles and diverse application scenarios of bin pumps is essential for optimizing material transport processes in various industrial settings.
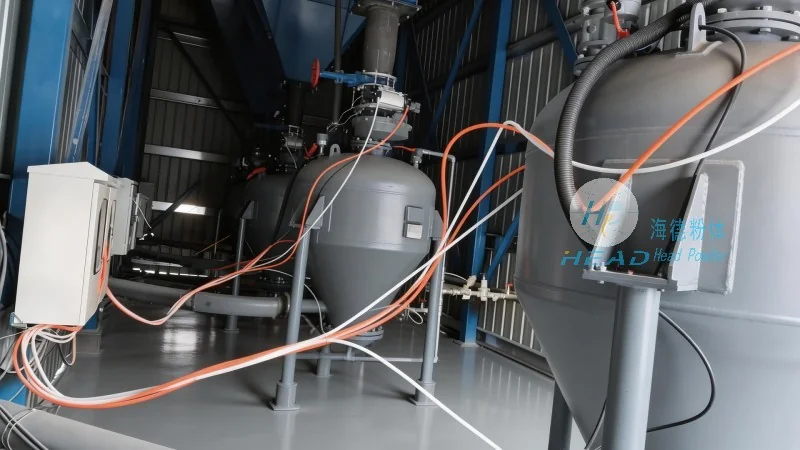
Principle of Bin Pump Material Transport
At the core of bin pump operation is the use of pressure differentials to move materials from a storage bin or hopper into a discharge line. The process typically involves the following key steps: first, the material is fed into the pump chamber from the storage vessel; second, the pump chamber is sealed and pressurized, often using compressed air or other gases; third, the pressurized material is forced through the discharge pipe to the destination point. This mechanism allows for controlled and consistent material flow, minimizing the risk of clogging and ensuring smooth operation.
The bin pump's design incorporates a flexible membrane or diaphragm that expands and contracts to create the pressure changes necessary for material movement. This design is particularly effective for handling fine powders and abrasive materials, as it reduces wear and tear on the pump components compared to traditional screw or belt conveyors. The pressure control system is crucial, as it allows operators to adjust the flow rate and pressure according to the specific characteristics of the material being transported.
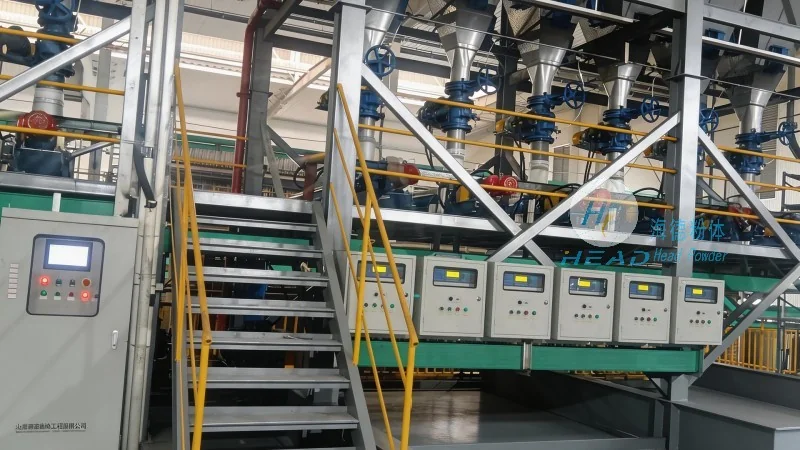
Working Scenarios and Application Characteristics
Bin pumps are widely used in a variety of industrial applications, each with unique requirements that influence their design and operation. For instance, in the cement and mining industries, bin pumps are commonly employed to transport raw materials such as limestone, clay, and ore from storage silos to processing plants. The high pressure and consistent flow provided by bin pumps help maintain the quality and uniformity of the material, which is critical for downstream processes like grinding and mixing.
In the chemical and pharmaceutical sectors, bin pumps are used to handle sensitive powders and granules, where contamination and material degradation must be minimized. The enclosed design of the bin pump, combined with its ability to operate under controlled pressure, ensures that the material remains sterile and free from external contaminants. This is particularly important for pharmaceutical products, where purity and consistency are paramount.
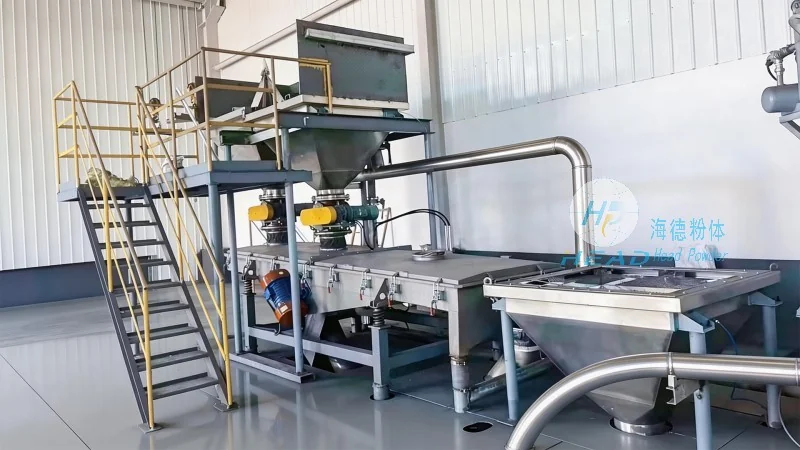
In addition to these industries, bin pumps are also used in the food and beverage industry to transport ingredients like flour, sugar, and spices. The hygienic design of modern bin pumps, with smooth surfaces and easy-to-clean components, meets the stringent sanitary standards required in food processing facilities. The ability to operate at low pressures and maintain a clean environment helps prevent cross-contamination and ensures product safety.
In the power generation sector, bin pumps are utilized to transport coal or biomass from storage bins to boilers. The high capacity and reliability of bin pumps make them ideal for handling large volumes of bulk materials, which is essential for maintaining consistent power output. The ability to adjust the flow rate according to the boiler's demand ensures efficient and cost-effective operation.
Company Profile and Technical Expertise
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of bulk material handling equipment, specializes in the design, manufacturing, and supply of bin pumps and related systems. With years of experience in the industry, the company has developed a reputation for producing high-quality, reliable equipment that meets the diverse needs of its clients. The company's technical team consists of experienced engineers and technicians who are well-versed in the principles of bin pump operation and material handling.
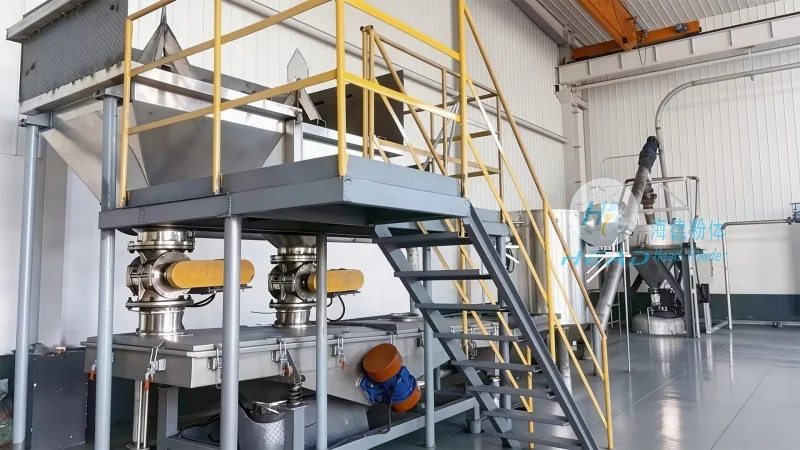
HeadPowder's bin pumps are designed to be versatile and adaptable, with options for different materials, flow rates, and pressure ranges. The company's products are manufactured using high-quality materials and advanced manufacturing techniques, ensuring durability and long service life. The company also provides comprehensive after-sales support, including maintenance, repair, and technical assistance, to ensure that its clients can maximize the performance and lifespan of their equipment.
HeadPowder's commitment to quality and customer satisfaction is reflected in its adherence to international standards and certifications. The company's products are tested and validated to meet the requirements of various industries, ensuring that they are safe, reliable, and effective. With a strong focus on innovation and research, HeadPowder continues to develop new and improved bin pump designs that meet the evolving needs of the market.