

Principles and Working Scene Characteristics of Wheat Material Conveying
Wheat material conveying is a critical process in agricultural and food processing industries, ensuring efficient movement of grain from one stage to another. Understanding the underlying principles and the specific characteristics of different working scenes is essential for optimizing operations and maintaining product quality. This article explores the fundamental mechanisms of wheat material conveying and highlights the key features of various operational environments where such systems are employed.
Core Principles of Wheat Material Conveying
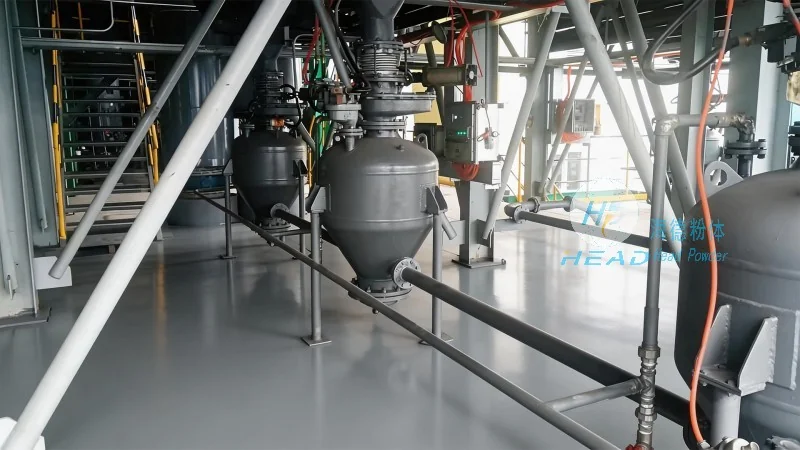
The primary goal of wheat material conveying is to transport grain efficiently and safely, minimizing damage and loss. Several key principles underpin the design and operation of conveying systems. First, gravity plays a significant role, especially in inclined or vertical conveyors, where the natural downward force assists in moving material. Mechanical forces, such as those generated by belts, screws, or buckets, are also crucial, providing the necessary traction to move wheat against gravity or in horizontal directions. Additionally, air pressure and vacuum systems are employed in pneumatic conveyors, using air to lift and transport grain through pipes. The choice of principle depends on the specific application, material characteristics, and operational requirements.
Working Scene Characteristics of Wheat Material Conveying Systems
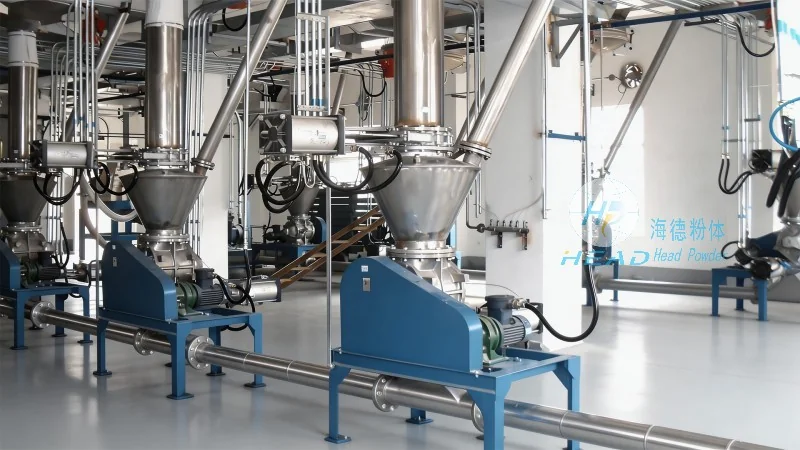
Wheat material conveying systems operate in diverse environments, each with unique characteristics that influence system design and performance. In agricultural settings, such as on-farm storage and handling, systems are often designed for high-volume, low-speed operation, focusing on moving grain from fields to storage silos or trucks. These scenes typically involve large quantities of raw wheat, requiring robust and durable equipment capable of handling abrasive materials and varying moisture levels. The working environment may also include outdoor conditions, necessitating weather-resistant components and protective enclosures.
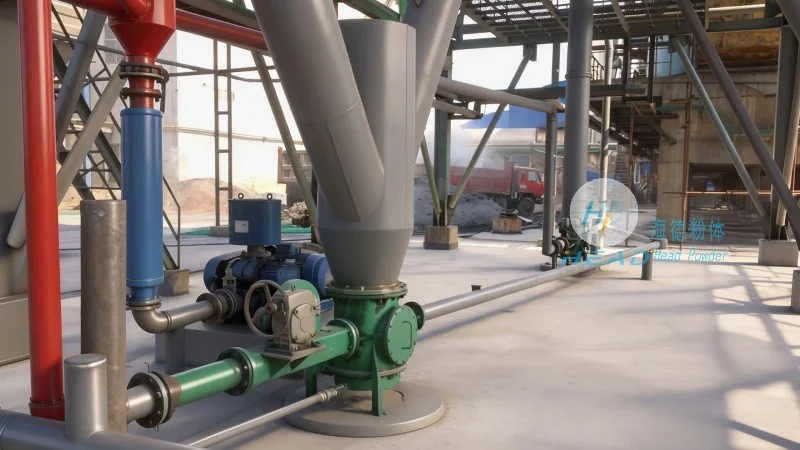
In industrial processing facilities, like flour mills and grain elevators, conveying systems operate under more controlled conditions but at higher speeds and with stricter quality control. Here, the focus shifts to precision and efficiency, with systems designed to minimize grain breakage and maintain uniform moisture content. The working scene may involve multiple stages of processing, such as cleaning, drying, and grinding, where conveyors integrate seamlessly with other machinery. This requires flexible and adaptable systems that can handle different grain types and processing stages without interruption.
Application of Conveying Principles in Real-World Scenarios
Real-world applications of wheat material conveying principles vary widely, reflecting the diverse needs of the industry. For example, in bulk handling operations, bucket elevators are commonly used to transport wheat vertically over long distances, leveraging mechanical force to lift grain from ground level to elevated storage bins. These systems are highly efficient for vertical movement and are widely adopted in large-scale grain storage facilities. In contrast, belt conveyors are preferred for horizontal or slight incline transport, offering a cost-effective solution for moving grain over short to medium distances. Screw conveyors, on the other hand, are ideal for handling bulk materials with high moisture content or sticky properties, as the rotating screw pushes material forward through a tube.
Case Study: Shandong HeadPowder Engineering Co., Ltd. and Wheat Conveying Solutions
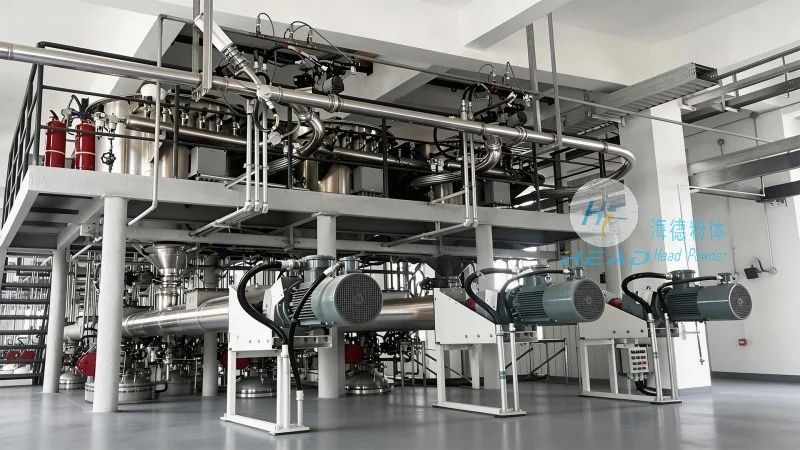
Shandong HeadPowder Engineering Co., Ltd., a leading provider of engineering solutions in the agricultural and food processing sectors, specializes in designing and manufacturing advanced wheat material conveying systems. Based in Shandong, China, the company leverages its deep understanding of grain handling principles to develop customized solutions tailored to specific operational needs. Their products range from traditional belt and screw conveyors to modern pneumatic systems, all engineered to meet the demands of both on-farm and industrial applications. The company’s commitment to quality and innovation ensures that their conveying systems not only adhere to industry standards but also enhance operational efficiency and product integrity. By integrating the core principles of wheat material conveying with practical working scene considerations, HeadPowder delivers reliable and effective solutions that contribute to the smooth operation of grain handling processes.