

Detailed Explanation of Sugar Pneumatic Conveying Systems
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of efficient bulk material handling solutions. Among their core offerings is the sugar pneumatic conveying system, a technology that revolutionizes the transport of granular materials like sugar from storage to processing or packaging units. This system leverages air pressure to move sugar through pipelines, offering advantages such as reduced labor costs, minimized material loss, and enhanced safety compared to traditional methods like belt conveyors or manual handling.
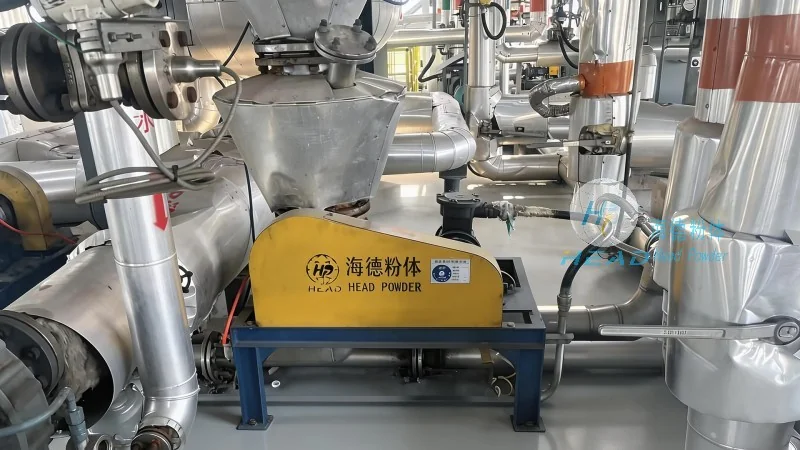
Key Components of a Sugar Pneumatic Conveying System
The sugar pneumatic conveying system consists of several critical components that work in tandem to ensure smooth operation. The primary elements include a hopper or storage silo for holding raw sugar, a rotary airlock or feeder to control the flow of sugar into the system, a blower or air compressor that generates the necessary air pressure, and a pipeline network that transports the sugar. Additionally, the system may incorporate a dust collector to manage airborne particles and a control panel for monitoring and adjusting operational parameters. Each component is carefully selected and sized to match the specific requirements of the sugar processing facility, ensuring optimal performance and reliability.
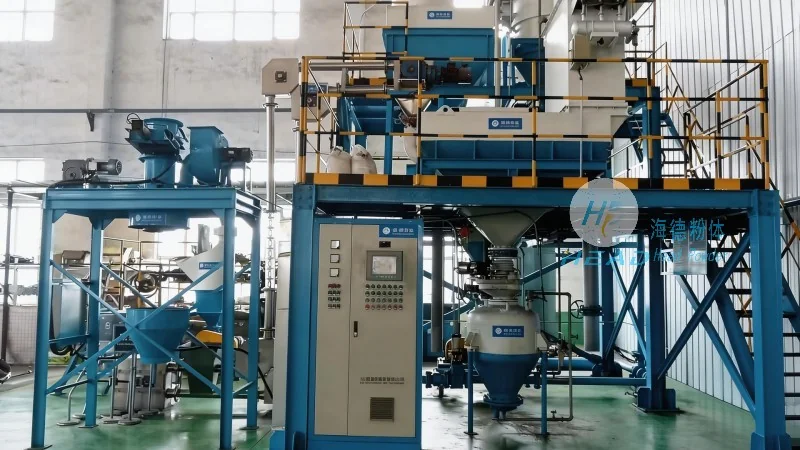
Advantages of Using a Pneumatic Conveying System for Sugar
Implementing a pneumatic conveying system for sugar processing offers numerous benefits that enhance operational efficiency and product quality. One of the most significant advantages is the reduction in material handling time and labor costs. Unlike traditional conveyors that require frequent maintenance and manual intervention, pneumatic systems operate continuously with minimal human involvement. This not only improves productivity but also reduces the risk of human error and workplace accidents. Furthermore, the enclosed pipeline system minimizes the exposure of sugar to contaminants, preserving its purity and quality throughout the transport process. Another key benefit is the ability to handle different sugar types and granule sizes without the need for extensive modifications to the system. This flexibility makes the system suitable for various applications, from raw sugar transport to refined sugar delivery to packaging lines.
Customization and Scalability of the System
HeadPowder understands that each sugar processing facility has unique operational needs and space constraints. Therefore, they offer customized pneumatic conveying systems tailored to specific requirements. The company's engineers work closely with clients to assess their current processes, storage capacities, and production volumes to design a system that maximizes efficiency and minimizes downtime. The systems can be scaled from small-scale installations for laboratory or pilot plants to large-scale industrial systems capable of handling thousands of tons of sugar per day. This scalability ensures that the system can grow with the client's business, providing a long-term solution that adapts to changing production demands. Additionally, the company provides comprehensive support, including installation, commissioning, and ongoing maintenance services, to ensure the system operates at peak performance throughout its lifecycle.
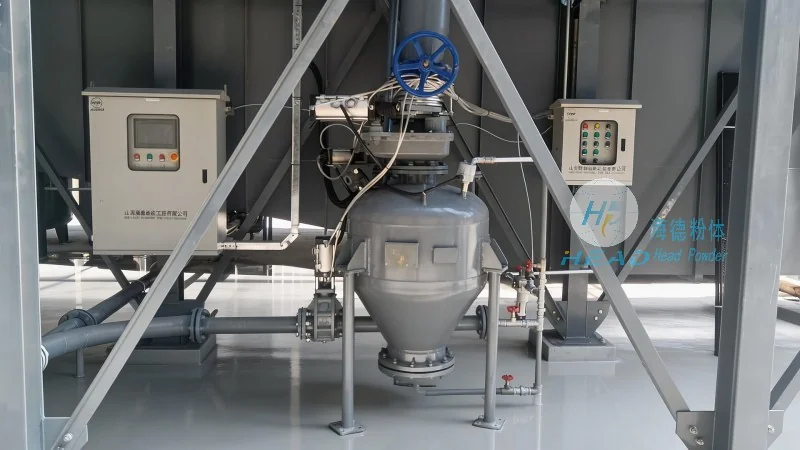
Installation and Maintenance Considerations
The successful implementation of a sugar pneumatic conveying system requires careful planning and execution. HeadPowder follows a systematic approach to installation, starting with site surveys to identify the optimal layout of the pipeline network and equipment placement. This ensures that the system integrates seamlessly with existing infrastructure and meets all safety and regulatory standards. During the installation phase, the company's technicians adhere to strict quality control measures to minimize the risk of leaks or air pressure loss. After installation, a thorough commissioning process is conducted to test the system's performance under various operating conditions. This includes checking the flow rates, air pressure levels, and material transfer efficiency to ensure that the system meets the client's specifications. Regular maintenance is also a critical aspect of the system's long-term performance. HeadPowder provides scheduled maintenance services, including filter changes, blower inspections, and pipeline cleaning, to prevent system downtime and extend the lifespan of the equipment. By adhering to these maintenance protocols, clients can ensure that their sugar pneumatic conveying system operates reliably and efficiently for years to come.