

Classification and Application Analysis of Quartz Sand Particle Pneumatic Conveying Systems
HeadPowder, a leading enterprise in the field of pneumatic conveying technology, specializes in the design, manufacturing, and implementation of advanced systems for transporting quartz sand particles. With a strong presence in Shandong, China, the company has established itself as a reliable partner for industries requiring efficient and reliable material handling solutions. This article provides a comprehensive overview of the classification of quartz sand particle pneumatic conveying systems and their practical applications, highlighting the technical aspects and operational benefits that make these systems indispensable in modern industrial processes.
Introduction to Quartz Sand Particle Pneumatic Conveying Systems
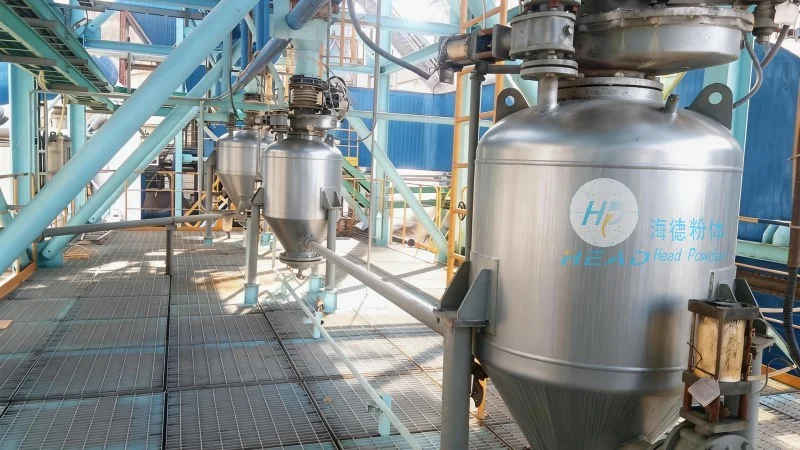
Quartz sand, a widely used industrial material, often requires efficient and dust-free transportation from production sites to processing facilities. Pneumatic conveying systems offer a solution that addresses these needs by utilizing air as the primary medium to transport solid particles. These systems are particularly advantageous for quartz sand due to its abrasive properties and the need for clean handling to maintain product quality. HeadPowder's expertise lies in developing customized pneumatic conveying solutions that cater to the specific requirements of quartz sand applications, ensuring optimal performance and longevity.
Classification of Pneumatic Conveying Systems for Quartz Sand
Pneumatic conveying systems for quartz sand can be broadly classified into two main categories: dilute-phase and dense-phase systems. Dilute-phase systems, which are more common for quartz sand, operate at higher air velocities, allowing particles to be suspended in the air stream. These systems are typically used for long-distance or high-capacity transport and are characterized by lower pressure requirements. Dense-phase systems, on the other hand, operate at lower air velocities, causing particles to form a slurry-like mixture with the air. This method is preferred for sensitive or valuable materials, as it minimizes particle degradation and ensures gentle handling. HeadPowder's engineers carefully evaluate the characteristics of quartz sand, such as particle size, density, and moisture content, to recommend the most suitable system type. For instance, in applications where quartz sand is transported over long distances with minimal pressure drop, a dilute-phase system with positive displacement blowers might be recommended. Conversely, for delicate or high-value quartz sand, a dense-phase system with rotary valves and pressure vessels could be implemented to preserve product integrity.
Key Components and Design Considerations in Quartz Sand Pneumatic Conveying
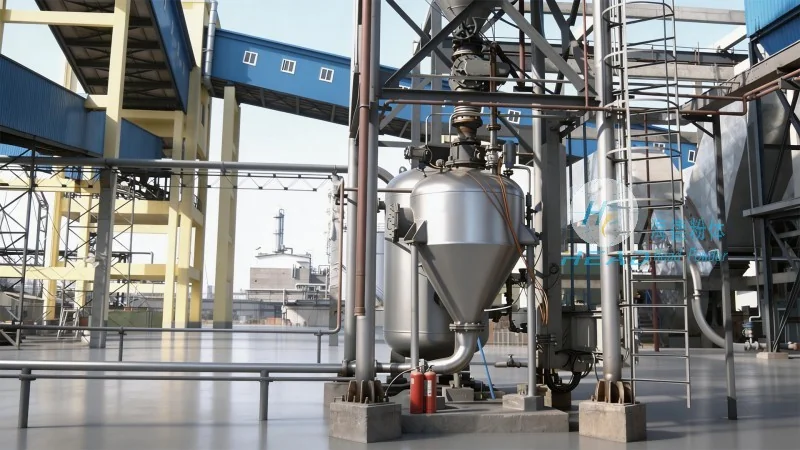
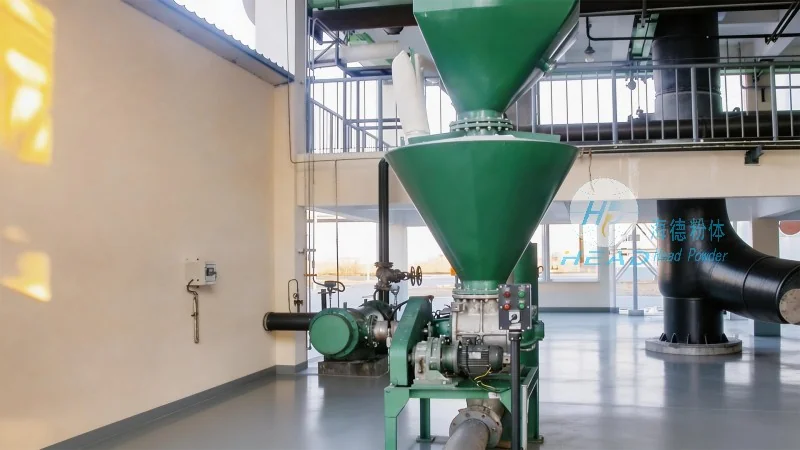
The effectiveness of a quartz sand pneumatic conveying system depends on several critical components and design factors. The primary components include the feed hopper, which ensures a consistent flow of quartz sand into the system; the air supply unit, typically a blower or compressor, which provides the necessary air pressure and volume; the conveying line, which transports the particles; and the discharge device, which delivers the quartz sand to the destination. HeadPowder emphasizes the importance of material selection for these components, as quartz sand is abrasive and can cause wear on metal surfaces. Therefore, components such as hoppers, pipelines, and valves are often constructed from corrosion-resistant materials like stainless steel or special alloys to extend their service life. Additionally, the system design considers factors like particle size distribution, which affects the air velocity required for proper suspension, and the system's overall pressure drop, which impacts energy efficiency. By optimizing these parameters, HeadPowder ensures that the conveying system operates efficiently while minimizing operational costs and maintenance requirements.
Application Analysis of Quartz Sand Pneumatic Conveying Systems
Quartz sand particle pneumatic conveying systems find extensive applications across various industries. In the glass manufacturing sector, quartz sand is a primary raw material, and efficient transportation is crucial for maintaining production schedules. HeadPowder's systems are commonly used to convey quartz sand from storage silos to glass furnaces, ensuring a continuous and clean supply. The systems are designed to handle the high temperatures and abrasive nature of quartz sand, with components that can withstand thermal stress and particle impact. In the construction industry, quartz sand is used in concrete and mortar production, and pneumatic conveying systems facilitate the transport of sand from bulk storage to mixing plants. This method reduces dust exposure for workers and improves the quality of the final product by preventing contamination. Furthermore, in the chemical and pharmaceutical industries, where quartz sand is used as a filler or abrasive, the systems must meet stringent cleanliness and hygiene standards. HeadPowder's solutions often incorporate dust collection and filtration systems to ensure that the conveyed material is free from contaminants, making them suitable for these applications. The versatility of quartz sand pneumatic conveying systems also makes them applicable in mining operations, where they are used to transport crushed quartz sand from processing plants to storage or shipping facilities. In each of these applications, the system's design is tailored to the specific operational conditions, ensuring that the quartz sand is transported safely, efficiently, and in compliance with industry standards.
Operational Benefits and Advantages of Quartz Sand Pneumatic Conveying
Implementing a quartz sand particle pneumatic conveying system offers numerous operational benefits that enhance productivity and reduce costs. One of the most significant advantages is the elimination of manual handling, which reduces labor costs and minimizes the risk of workplace injuries. The systems also provide a dust-free environment, improving worker safety and comfort. Additionally, pneumatic conveying systems are more energy-efficient compared to traditional methods like belt conveyors or bucket elevators, as they use air to transport the material rather than mechanical components. This results in lower energy consumption and reduced operational expenses over time. The systems are also highly flexible, allowing for easy integration with existing production lines and the ability to adjust the conveying rate based on demand. HeadPowder's systems are equipped with advanced control systems that enable real-time monitoring and adjustment, ensuring optimal performance. Furthermore, the systems are designed for easy maintenance, with components that can be easily accessed and replaced, reducing downtime and maintenance costs. The durability of the components, particularly those made from corrosion-resistant materials, contributes to the long-term reliability of the system, making it a cost-effective solution for quartz sand transportation.
Conclusion and Future Outlook
Quartz sand particle pneumatic conveying systems, as classified and analyzed in this article, represent a sophisticated and efficient solution for material handling in various industries. HeadPowder's expertise in designing and implementing these systems ensures that clients receive tailored solutions that meet their specific needs. By leveraging advanced technology and careful engineering, the company provides systems that are not only effective but also durable and cost-efficient. As industries continue to demand higher efficiency and cleaner production processes, the importance of reliable pneumatic conveying systems for quartz sand will only grow. HeadPowder remains committed to innovation and excellence, continuing to develop new solutions that enhance the performance and sustainability of quartz sand transportation. With its strong presence in Shandong, China, and a global reputation for quality, HeadPowder is well-positioned to meet the evolving needs of the industry and provide sustainable material handling solutions for quartz sand and other industrial materials.