

Working Principle and Characteristics of High-Pressure Bin Pump Powder Transport
High-pressure bin pumps represent a critical technology in the realm of bulk material handling, particularly for industries dealing with powders such as cement, chemicals, and food products. These systems are engineered to transport solid materials efficiently under high pressure, ensuring stable and reliable operation across various industrial processes. This article aims to explore the fundamental working principle of high-pressure bin pumps and highlight their key characteristics, providing a comprehensive overview of their functionality and advantages.
Working Principle of High-Pressure Bin Pump
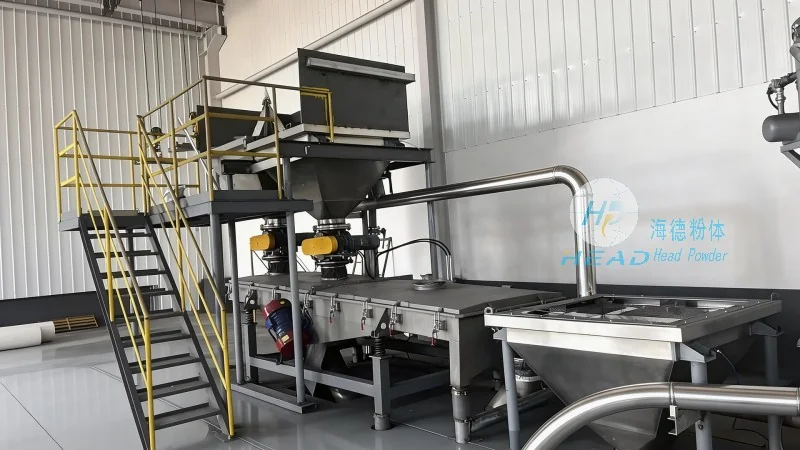
The operation of a high-pressure bin pump is centered on the principle of pressure-driven material displacement. The pump system typically comprises a hopper for material storage, a pressure chamber, and a discharge valve. When the hopper is filled with the powder material, the pump's pressure generation system activates, creating a high-pressure environment within the chamber. This pressure forces the material from the hopper into the pressure chamber, which then transfers the material through a pipeline to the intended destination. The core mechanism often involves a piston or diaphragm that cyclically compresses and releases, maintaining the necessary pressure to move the material. Control systems monitor parameters like pressure, flow rate, and material level, ensuring the pump operates within optimal conditions and adjusts automatically to maintain consistent performance. This automated process eliminates manual intervention, enhancing efficiency and reducing the risk of operational errors.
Key Characteristics of High-Pressure Bin Pump
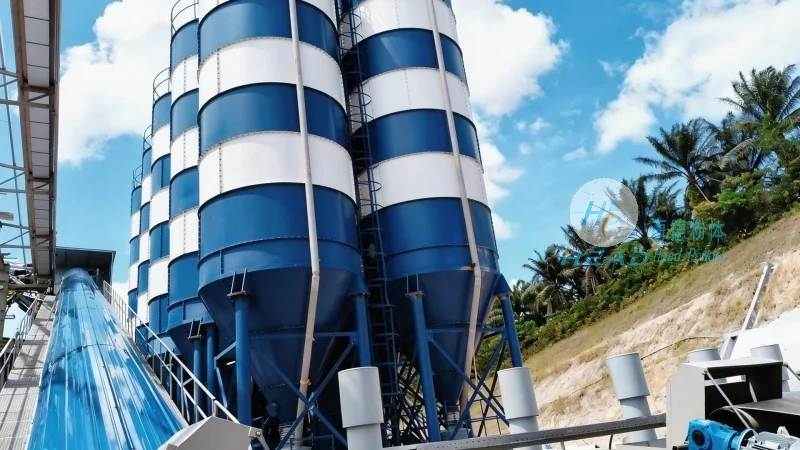
High-pressure bin pumps exhibit several distinct attributes that make them suitable for diverse industrial applications. Firstly, they deliver high transport efficiency, capable of moving substantial volumes of powder at elevated speeds. The high-pressure environment minimizes material degradation and ensures a consistent flow, which is vital for maintaining product quality. Secondly, the pumps are built for durability and reliability, featuring robust construction that can withstand harsh operating conditions. Materials such as corrosion-resistant steel and wear-resistant components are commonly used, extending the equipment's service life and reducing maintenance needs. Thirdly, they offer precise control over material discharge, allowing for accurate regulation of flow rates. This capability is essential for processes requiring exact dosing or batching, ensuring uniformity in production. Additionally, high-pressure bin pumps are energy-efficient, with optimized pressure systems that reduce operational costs. Their design minimizes energy waste while maximizing material throughput. Finally, the pumps are low-maintenance, with simple yet effective mechanisms that minimize downtime and maintenance expenses, making them cost-effective for long-term use.
Applications and Industrial Advantages
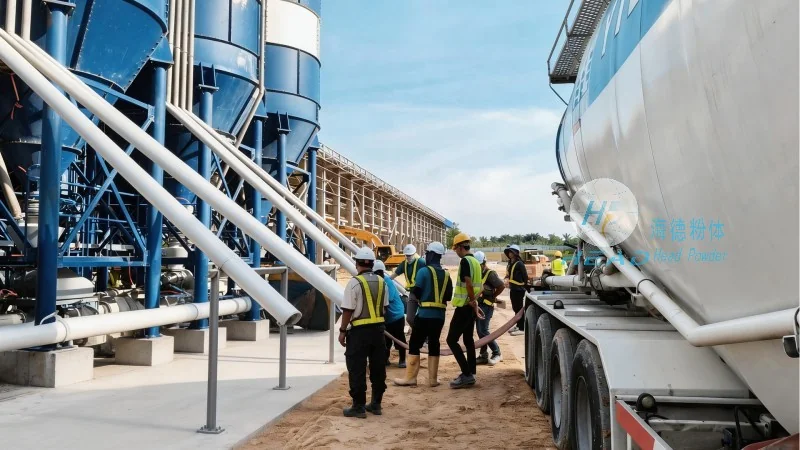
High-pressure bin pumps find extensive application across multiple industries, where efficient powder transport is critical. In the cement industry, they are employed to handle raw materials and finished products, facilitating smooth production lines and reducing material handling time. The chemical industry utilizes them to transport various powders, including chemicals and additives, ensuring safety and preventing contamination. The food processing sector also benefits from their use, as they can handle food-grade powders without compromising quality or safety. The advantages of high-pressure bin pumps in these settings include improved production efficiency, reduced material loss, and enhanced operational safety. Their ability to handle abrasive and corrosive materials makes them versatile for different industrial needs. Furthermore, the pumps contribute to cost savings by reducing labor and maintenance costs, while increasing overall productivity. This makes them a preferred choice for industries seeking reliable and economical powder handling solutions.
Conclusion and Company Profile
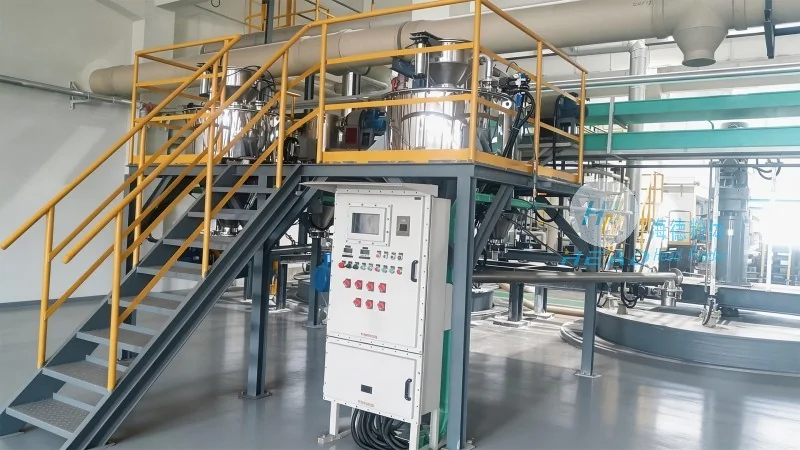
High-pressure bin pumps are indispensable in modern industrial operations, offering a reliable and efficient solution for bulk powder transport. Their working principle, based on pressure-driven displacement, ensures consistent and high-volume material transfer. The key characteristics, including high efficiency, durability, and precise control, make them superior to traditional transport methods. As a leading manufacturer in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and producing high-quality high-pressure bin pumps tailored to meet the specific needs of various industries. With a focus on innovation and quality, the company provides durable and reliable equipment that enhances operational efficiency and reduces costs for its clients. Based in Shandong, China, HeadPowder Engineering Co., Ltd. has established itself as a trusted partner in the powder handling industry, delivering solutions that meet the highest standards of performance and reliability. The company's commitment to excellence and customer satisfaction has positioned it as a key player in providing advanced powder transport technologies to global markets.