

Working Principle and Features of Automatic Powder Conveyors
Automatic powder conveyors are essential equipment in various industrial sectors, designed to efficiently transport bulk powders from one location to another. These systems are engineered to handle a wide range of powder types, including chemicals, food ingredients, and pharmaceuticals, ensuring safe and reliable material handling. The technology behind these conveyors combines mechanical components with advanced control systems to optimize performance and minimize downtime.
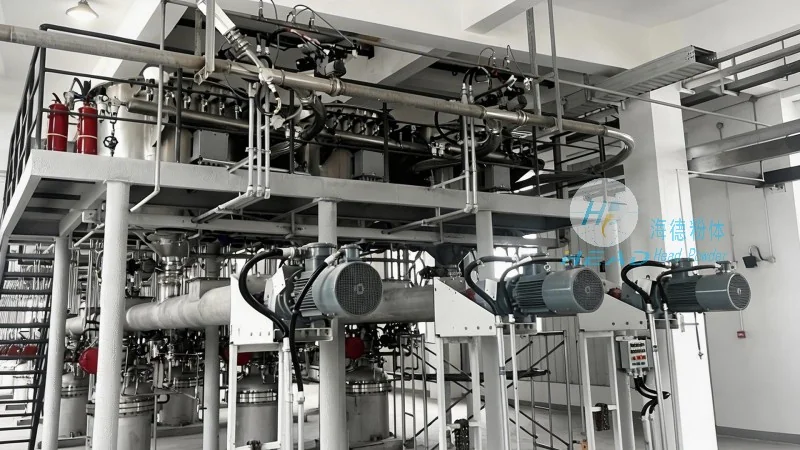
Working Principle of Automatic Powder Conveyors
The core operation of an automatic powder conveyor involves several key components working in tandem. A typical system includes a hopper for material storage, a conveyor mechanism (such as a screw or pneumatic tube), and a control unit that regulates the flow. The process begins when the powder is fed into the hopper. The control unit then activates the conveyor, which moves the material through the system. For pneumatic conveyors, compressed air is used to create a pressure differential that propels the powder forward. In contrast, mechanical conveyors rely on rotating screws or belts to transport the material. The system is equipped with sensors and valves to monitor and adjust the flow rate, ensuring consistent and controlled delivery. This integrated approach allows for precise control over the conveying process, adapting to varying material characteristics and operational demands.
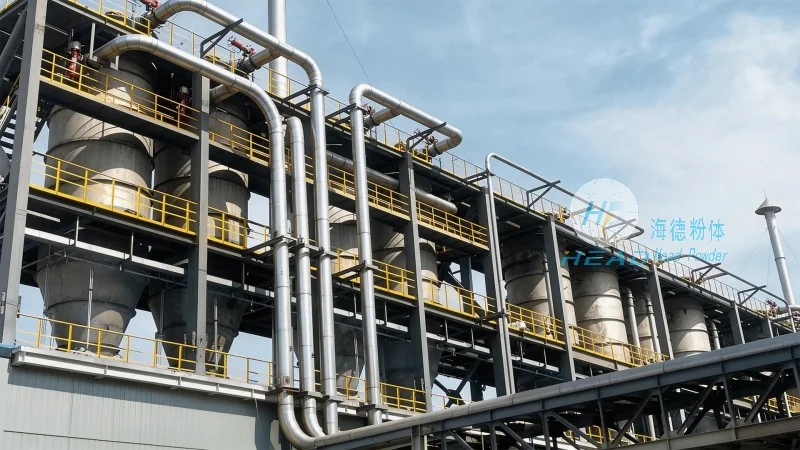
Key Features of Automatic Powder Conveyors
Automatic powder conveyors are distinguished by several critical features that enhance their functionality and reliability. One of the primary advantages is their ability to handle diverse powder types, from fine powders to coarse granules, without causing segregation or degradation. The systems are designed with hygienic and dust-proof features, making them suitable for applications in food, pharmaceutical, and chemical industries. Advanced control systems enable real-time monitoring and adjustment, reducing the risk of overloading or underflow. Additionally, these conveyors are equipped with safety mechanisms, such as emergency stop buttons and overload protection, to prevent accidents and equipment damage. The modular design allows for easy installation and maintenance, with components that can be replaced or upgraded without disrupting the entire system. This flexibility ensures that the equipment can adapt to changing production needs and evolving industry standards.
Applications and Benefits in Industrial Settings
Automatic powder conveyors find extensive applications across multiple industries, contributing to improved efficiency and product quality. In the chemical industry, they are used to transport raw materials and finished products, facilitating seamless production workflows. The food and beverage sector benefits from their hygienic design, which ensures compliance with safety regulations and maintains product integrity. Pharmaceutical manufacturers rely on these systems to handle active ingredients and excipients, minimizing contamination risks and ensuring consistent dosing. The benefits of using automatic powder conveyors extend beyond operational efficiency; they also contribute to cost savings by reducing labor costs and minimizing material waste. The precise control over flow rates helps prevent overfilling or underfilling, which can lead to product defects or waste. Furthermore, the reduced need for manual handling improves workplace safety, lowering the risk of injuries and accidents. These advantages make automatic powder conveyors a valuable investment for businesses seeking to enhance their production processes and maintain competitiveness in their respective markets.
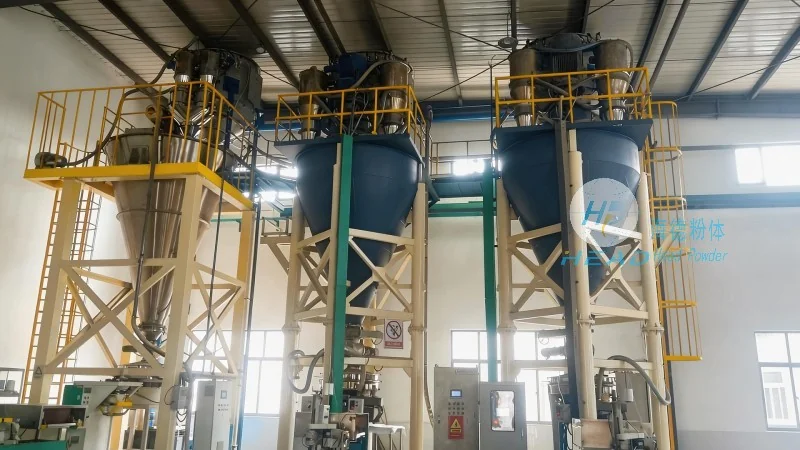
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of industrial powder handling equipment. With a focus on innovation and quality, the company specializes in designing and producing automatic powder conveyors tailored to meet the diverse needs of various industries. HeadPowder's commitment to customer satisfaction is reflected in their comprehensive product line, which includes a range of conveyor systems, from basic pneumatic models to advanced mechanical solutions. The company's headquarters is located in Shandong, China, where a team of experienced engineers and technicians work to develop cutting-edge technology and provide reliable support to clients worldwide. By adhering to strict quality standards and adhering to international regulations, HeadPowder ensures that their products meet the highest industry benchmarks, delivering performance and durability that customers can trust. The company's dedication to research and development enables them to stay ahead of market trends, offering solutions that address the evolving challenges of modern industrial operations.