

Working Principle and Features of Calcium Phosphate Powder Conveyors
Shandong HeadPowder Engineering Co., Ltd. specializes in the design and manufacturing of advanced powder handling equipment, including calcium phosphate powder conveyors. These conveyors are engineered to efficiently transport calcium phosphate powders, a critical component in various industrial applications. Understanding the working principle and key features of these systems is essential for optimizing material flow and ensuring operational reliability. This article provides a comprehensive overview of how calcium phosphate powder conveyors operate and the characteristics that make them ideal for handling bulk powders.
Working Principle of Calcium Phosphate Powder Conveyors
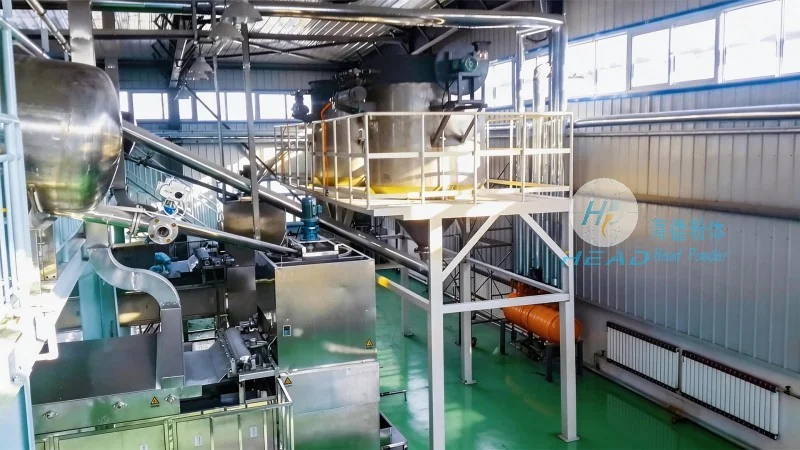
The working principle of calcium phosphate powder conveyors relies on mechanical or pneumatic systems to move bulk materials. These conveyors typically use screw, belt, or air-assisted mechanisms to transport the powder from the inlet to the outlet. The design is tailored to accommodate the unique properties of calcium phosphate powders, such as their particle size distribution, flowability, and potential tendency to agglomerate. The process begins with the powder being fed into the conveyor inlet, where it is then propelled along the conveyor path by rotating screws or moving belts. The speed and direction of the conveyor can be adjusted to control the flow rate, ensuring consistent and controlled material delivery. This mechanism minimizes the risk of clogging or blockages, which are common issues with less efficient systems. The continuous operation of the conveyor allows for a steady supply of powder to downstream processes, enhancing overall production efficiency.
Key Features of Calcium Phosphate Powder Conveyors
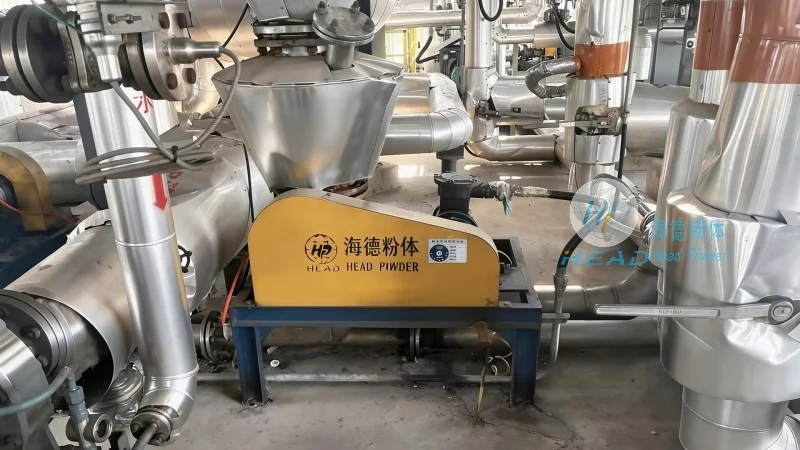
Several key features distinguish calcium phosphate powder conveyors from other bulk handling equipment. One of the most significant features is their robust construction, often made from stainless steel or specialized alloys, which provides resistance to abrasion and corrosion. This is particularly important when handling calcium phosphate powders, which may have high wear resistance or chemical reactivity. The durable materials ensure long-term performance and reduce maintenance costs over the equipment's lifespan. Another notable feature is the design for easy cleaning and maintenance. Many models include removable components and self-cleaning mechanisms that prevent powder buildup, which is critical for maintaining hygiene standards in food and pharmaceutical applications. The ability to maintain a clean system also helps prevent cross-contamination and ensures product quality. Additionally, these conveyors are equipped with variable speed drives and adjustable feed controls, allowing operators to fine-tune the system to match the specific requirements of the production process. This adaptability enhances efficiency and reduces downtime by optimizing material flow.
Applications and Benefits in Industrial Operations
Calcium phosphate powder conveyors are widely used in industries such as food processing, pharmaceutical manufacturing, and chemical production. In the food industry, they are used to transport calcium phosphate as an ingredient in dairy products, bakery items, and other food formulations. The ability to maintain low contamination levels and control the flow of the powder ensures that final products meet strict regulatory standards. In pharmaceutical applications, these conveyors are crucial for handling active pharmaceutical ingredients (APIs) and excipients, where precision and cleanliness are paramount. The features that enhance hygiene and prevent cross-contamination, such as sealed systems and easy-to-clean components, are particularly valuable in this sector. In chemical manufacturing, calcium phosphate powders are used as raw materials in the production of fertilizers and other chemical products. The robust design of the conveyors, with their ability to handle high volumes and abrasive materials, contributes to the overall efficiency of the production line. The benefits of using these conveyors include improved material handling efficiency, reduced labor costs, and enhanced safety by minimizing manual handling of powders. Overall, the combination of their working principle and key features makes calcium phosphate powder conveyors a reliable and effective solution for bulk material transportation in industrial settings.
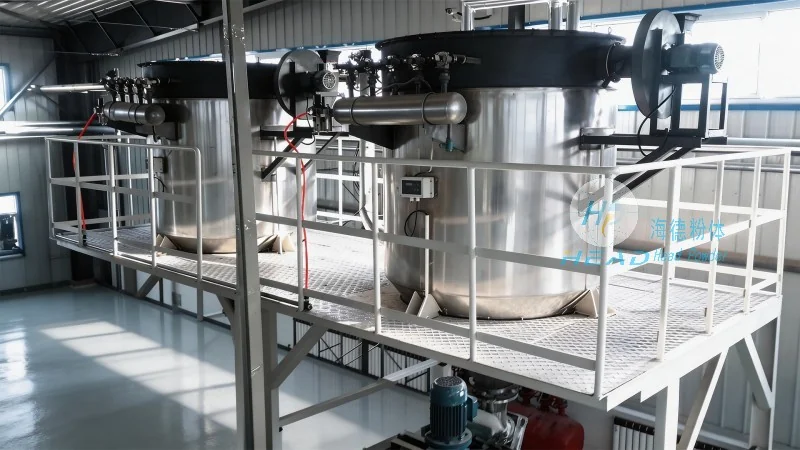
With a focus on quality and innovation, Shandong HeadPowder Engineering Co., Ltd. provides calcium phosphate powder conveyors that meet the highest industry standards. The company's commitment to customer satisfaction and product excellence ensures that clients receive equipment that is durable, efficient, and tailored to their specific needs. Based in Shandong, China, HeadPowder Engineering continues to lead the way in powder handling technology, delivering solutions that enhance operational performance and support business growth.