

Working Principle and Characteristics of High-Pressure Bin Pump Powder Pneumatic Conveying
High-pressure bin pumps are a critical component in modern powder handling systems, offering an efficient and reliable method for pneumatic conveying of bulk materials. This article explores the working principle and key characteristics of high-pressure bin pump systems, providing insights into their operation and advantages in industrial applications.
Working Principle of High-Pressure Bin Pump Powder Pneumatic Conveying
The core mechanism of a high-pressure bin pump involves the use of compressed air to create a pressure differential that propels bulk powders through a pipeline. The system typically consists of a storage bin equipped with a discharge valve and an airlock mechanism. When the bin is filled with the target powder, the discharge valve is closed, and compressed air is introduced into the bin. This pressurization forces the powder to flow out through the discharge line, which is connected to the conveying pipeline. The airlock ensures that only a controlled amount of powder is released at a time, preventing clogging and maintaining consistent flow rates. The compressed air acts as the driving force, converting the stored potential energy in the bin into kinetic energy for the powder particles, enabling them to travel through the pipeline to the destination point.
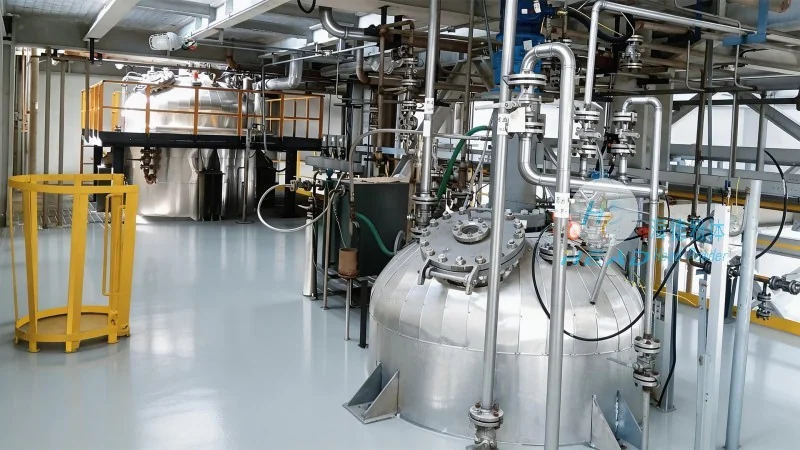
Key Characteristics of High-Pressure Bin Pump Systems
High-pressure bin pump systems exhibit several notable characteristics that make them suitable for a wide range of industrial applications. Firstly, they offer high conveying efficiency, capable of transporting powders over long distances with minimal pressure loss. The system's ability to handle abrasive and corrosive materials without significant wear or damage is another key advantage. Additionally, high-pressure bin pumps are energy-efficient, as they utilize compressed air effectively to move large volumes of material with relatively low operational costs. Environmental considerations are also addressed, as the system minimizes dust emissions and reduces the need for manual handling, contributing to a cleaner and safer working environment. The design of the bin pump allows for easy integration with existing processing lines, making it a versatile solution for various industries, including pharmaceuticals, food processing, and chemical manufacturing.
Applications and Advantages in Industrial Settings
High-pressure bin pumps are widely used in industries where the handling of fine powders is essential. In the pharmaceutical sector, for example, these systems ensure the safe and hygienic transfer of raw materials and finished products, maintaining compliance with regulatory standards. The food industry benefits from the system's ability to handle sensitive ingredients without contamination or degradation. In chemical manufacturing, the high-pressure bin pump's durability and resistance to corrosive substances make it ideal for transporting reactive powders. The advantages of this technology extend beyond material handling, as it enhances overall production efficiency by reducing downtime and improving process reliability. The system's compact design and low maintenance requirements further contribute to its appeal in modern industrial settings.
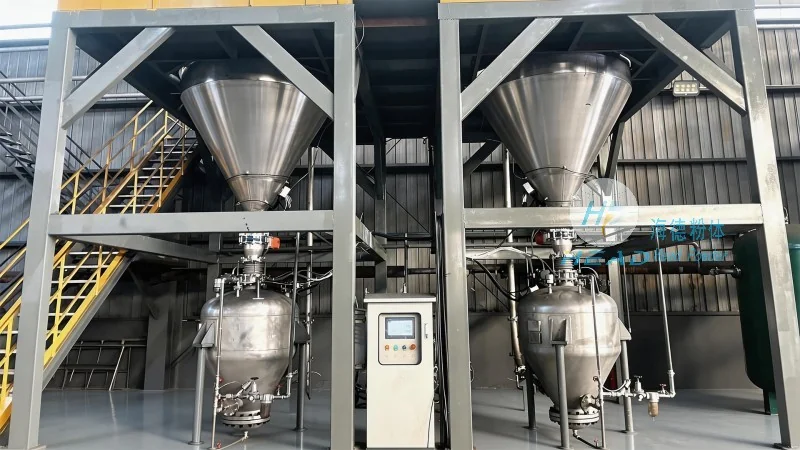
Conclusion and Company Overview
High-pressure bin pump powder pneumatic conveying systems represent a sophisticated solution for efficient bulk material transport. By leveraging compressed air to move powders through pipelines, these systems offer significant advantages in terms of efficiency, reliability, and environmental impact. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality high-pressure bin pump systems tailored to meet the specific needs of various industries. With a focus on innovation and customer satisfaction, the company has established itself as a trusted partner for businesses seeking reliable and effective powder handling solutions. Based in Shandong, China, HeadPowder continues to advance the technology of pneumatic conveying, ensuring that clients receive cutting-edge solutions that enhance their operational performance and productivity.