

Principle and Working Scene Characteristics of Automatic Bulk Bag Opening Pneumatic Conveying System
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer based in Shandong, China. The company specializes in the research, development, and production of advanced pneumatic conveying systems, particularly those designed for efficient bulk bag handling and material transport. With a focus on innovation and quality, HeadPowder has established itself as a leading provider of industrial material handling solutions, serving clients across various sectors including food, pharmaceuticals, chemicals, and mining.
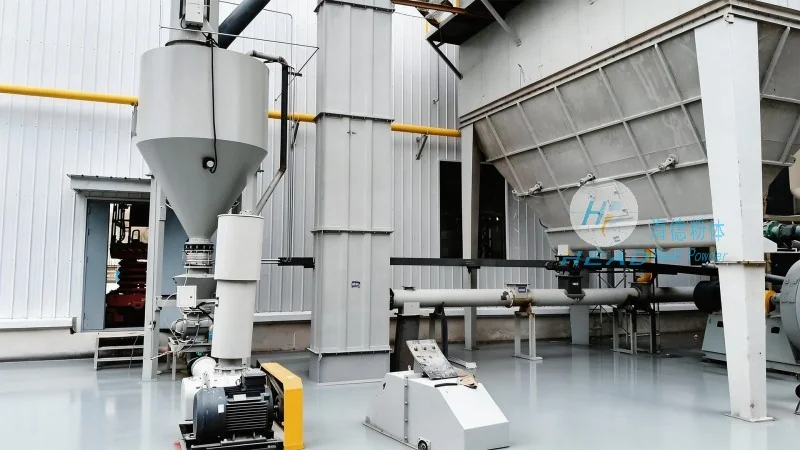
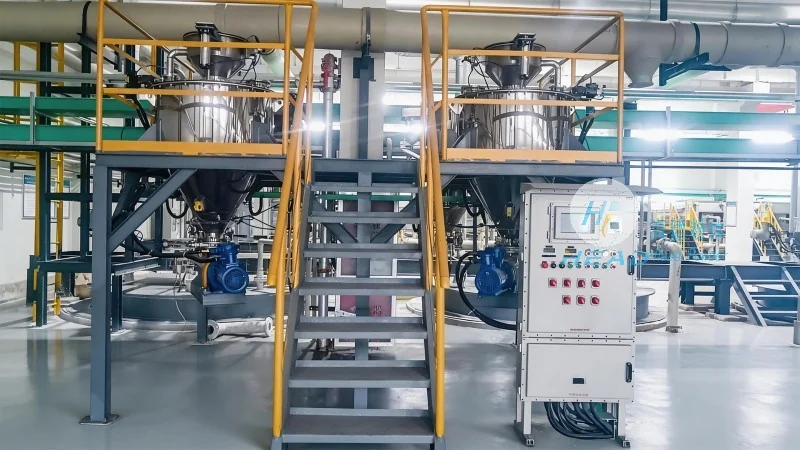
Principle of the Automatic Bulk Bag Opening Pneumatic Conveying System
The automatic bulk bag opening pneumatic conveying system is a sophisticated piece of equipment engineered to streamline the process of handling bulk materials from sealed bags. At its core, the system operates on the principle of pneumatic conveying, which utilizes air pressure to move particulate materials through a pipeline network. The system begins with the automatic opening of the bulk bag, a critical step that eliminates the need for manual intervention and reduces the risk of material spillage or contamination. Once the bag is opened, the material is drawn into the conveying line through a hopper or inlet, where it is then propelled by a series of air jets or a positive pressure blower. The air flow is carefully controlled to ensure the material moves smoothly and efficiently through the system, minimizing blockages and maximizing throughput. The system may also incorporate features such as air filtration to maintain air quality and prevent dust accumulation, as well as material separation mechanisms to handle different types of bulk powders or granules. The overall design is optimized for reliability and efficiency, ensuring that the system can operate continuously without frequent maintenance or downtime.
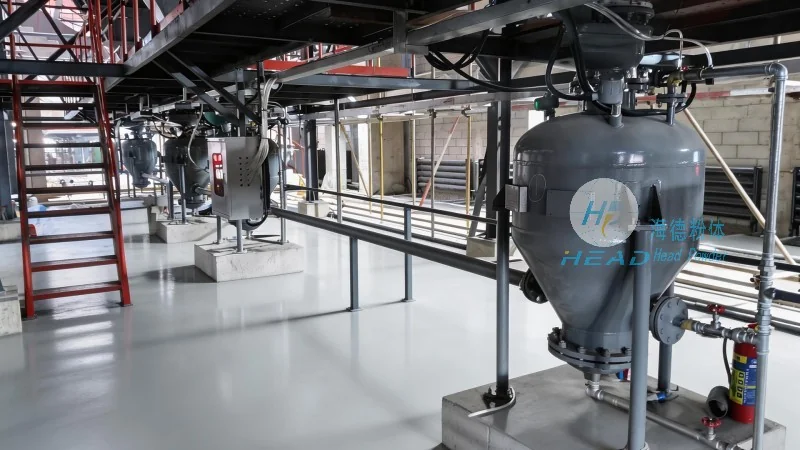
Working Scene Characteristics and Application Scenarios
The automatic bulk bag opening pneumatic conveying system is designed for a wide range of industrial applications where bulk material handling is essential. These systems are commonly used in industries such as food processing, pharmaceuticals, chemicals, and mining, where the need to handle large quantities of powders or granules efficiently and safely is paramount. The system's ability to handle various materials, including sensitive products that require dust-free environments, makes it a versatile solution for many manufacturing processes. In a typical working scene, the system is integrated into a production line where bulk bags are delivered to the facility. The automatic opening mechanism ensures that the bags are opened quickly and reliably, allowing the material to be transferred directly into the processing equipment without the need for intermediate storage or manual handling. This integration enhances operational efficiency by reducing downtime and labor costs associated with manual bag handling. The system's design also allows for easy integration with existing production infrastructure, making it a cost-effective upgrade for companies looking to improve their material handling capabilities. Additionally, the system's compact and modular design makes it suitable for both new installations and retrofitting into existing facilities, providing flexibility in deployment.
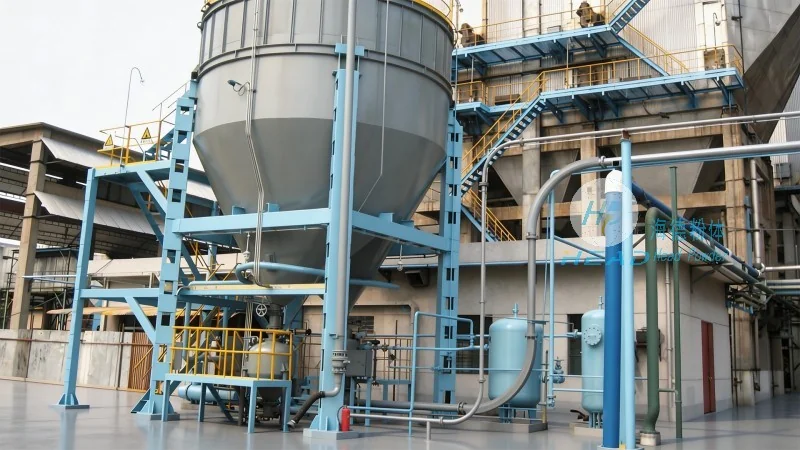
Key Features and Advantages
One of the key features of the automatic bulk bag opening pneumatic conveying system is its automated operation, which significantly reduces the need for manual labor and minimizes the risk of human error. The system can be programmed to handle different bag sizes and types, ensuring compatibility with a wide range of bulk bag materials. The pneumatic conveying technology used in the system is highly efficient, as it eliminates the need for mechanical components like belts or screws that can cause wear and tear over time. This results in lower maintenance costs and longer service life for the equipment. Another advantage is the system's ability to handle a variety of materials, from fine powders to coarse granules, without the need for adjustments or modifications. The air filtration system is also a critical feature, as it helps to maintain a clean and safe working environment by capturing dust and particles that are generated during the conveying process. This is particularly important in industries where air quality is a regulatory requirement, such as pharmaceutical manufacturing or food processing.