

Principle and Working Scene Characteristics of Coke Powder Conveying Equipment
For industrial applications involving the handling of coke powder, efficient and reliable conveying equipment is essential to ensure smooth material flow and operational safety. This article explores the fundamental principles behind coke powder conveying systems and highlights the key characteristics of working environments where such equipment is typically deployed. The information is presented by Shandong HeadPowder Engineering Co., Ltd., a leading provider of specialized powder handling solutions based in China.
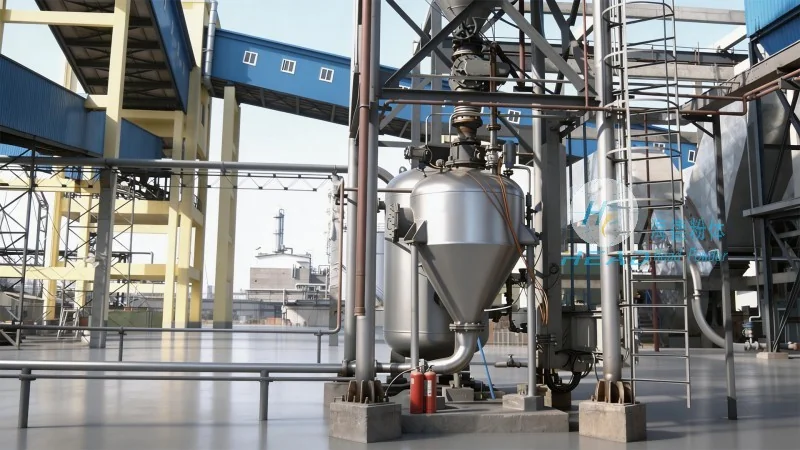
Introduction to Coke Powder Conveying Equipment
Coke powder, a fine particulate material derived from the carbonization of coal, is widely used in various industrial processes, including steel production, chemical manufacturing, and energy generation. The efficient transport of coke powder from storage silos or production units to processing points requires specialized equipment designed to handle its unique physical properties. Conveying systems for coke powder must address challenges such as dust generation, material segregation, and the need for low maintenance while maintaining high throughput rates. Shandong HeadPowder Engineering Co., Ltd. specializes in developing and manufacturing advanced coke powder conveying solutions tailored to meet the demands of modern industrial operations.
Principle of Operation for Coke Powder Conveying Systems
The core principle of coke powder conveying equipment is to utilize mechanical forces to move the fine particles through a pipeline or duct. Common types of conveying systems include pneumatic conveying (air-assisted) and mechanical conveying (e.g., screw conveyors, belt conveyors). Pneumatic conveying systems operate by injecting compressed air or other gases into a pipeline, creating a flow that transports the coke powder particles. This method is particularly effective for handling fine powders and can be adapted for both low and high-pressure applications. Mechanical conveyors, on the other hand, rely on rotating components like screws or belts to physically move the material along a defined path. Each system has its advantages and is selected based on factors such as material characteristics, distance to be conveyed, and environmental constraints.
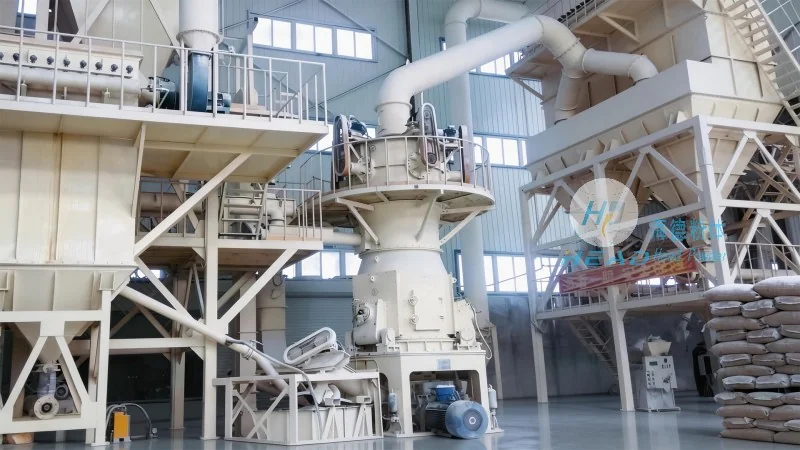
Key Working Scene Characteristics
The working environment for coke powder conveying equipment is typically characterized by several distinct features that influence equipment design and performance. First, the material itself is prone to dust generation, which necessitates robust dust control measures to prevent contamination and ensure workplace safety. Second, coke powder can be abrasive, requiring equipment with durable components to minimize wear and extend service life. Third, the need for continuous operation in industrial settings demands high reliability and low downtime, making equipment maintenance and operational efficiency critical considerations. Additionally, the scale of industrial operations often involves large volumes of material, necessitating conveyors with high capacity and consistent performance. Shandong HeadPowder Engineering Co., Ltd. designs its conveying systems to address these challenges, ensuring optimal performance in diverse industrial applications.
Application Examples and Operational Scenarios
Coke powder conveying equipment is widely used in various industrial settings, including steel mills, chemical plants, and power generation facilities. In steel production, for instance, coke powder is transported from storage silos to blast furnaces for use as a fuel and reducing agent. The conveying system must handle large quantities of coke powder under high-temperature and high-pressure conditions, requiring specialized materials and design features. In chemical plants, coke powder may be used as a raw material in the production of fertilizers or other chemicals, where the conveying equipment must maintain material purity and prevent contamination. Power generation facilities may also utilize coke powder as a fuel source, requiring efficient and reliable transport to combustion units. Each of these scenarios presents unique challenges, and Shandong HeadPowder Engineering Co., Ltd. tailors its solutions to meet the specific requirements of each application.

Advantages of Advanced Coke Powder Conveying Solutions
Modern coke powder conveying systems offer several advantages over traditional methods, including improved efficiency, reduced labor costs, and enhanced safety. Pneumatic conveying systems, for example, can transport materials over long distances with minimal energy consumption and without the need for multiple transfer points. Mechanical conveyors, while requiring more maintenance, provide a cost-effective solution for short-distance transport and can handle a wide range of material types. The use of advanced materials and design techniques has also improved the durability and reliability of conveying equipment, reducing the need for frequent repairs and extending the operational lifespan. Additionally, modern control systems allow for real-time monitoring of conveyor performance, enabling operators to quickly identify and address issues before they impact production. Shandong HeadPowder Engineering Co., Ltd. leverages these advancements to provide cutting-edge coke powder conveying solutions that meet the evolving needs of industrial clients.
Conclusion
In conclusion, coke powder conveying equipment plays a vital role in industrial operations by ensuring the efficient and safe transport of this critical material. The principles of operation, combined with the working scene characteristics, dictate the design and selection of appropriate conveying systems. Shandong HeadPowder Engineering Co., Ltd., with its expertise in powder handling technology, provides comprehensive solutions tailored to the unique requirements of coke powder applications. By addressing challenges such as dust control, material abrasiveness, and operational reliability, these systems contribute to improved productivity and safety in industrial settings. As industrial demands continue to evolve, advanced coke powder conveying solutions will remain essential for maintaining operational efficiency and meeting the needs of modern manufacturing processes.