

Principle and Working Scene Characteristics of Coffee Material Pneumatic Conveying Equipment
HeadPowder, a leading manufacturer in the field of material handling solutions, specializes in the design and production of advanced coffee material pneumatic conveying equipment. This article delves into the fundamental principles behind these systems and explores the key characteristics of their application in various working environments.
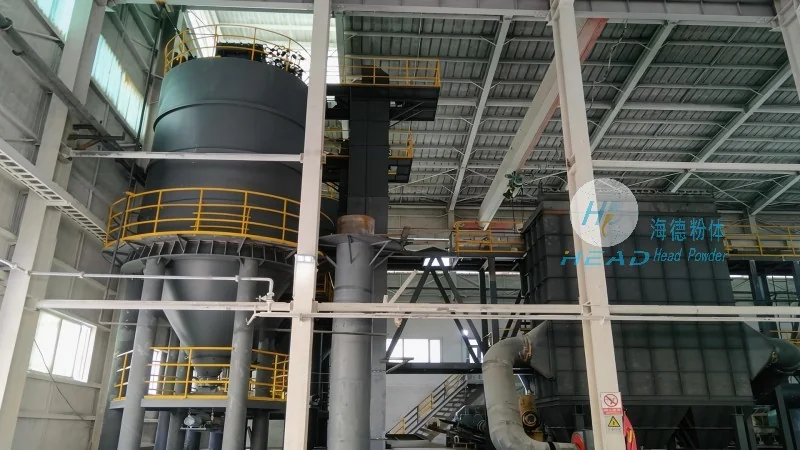
Understanding the Core Principle of Pneumatic Conveying for Coffee Materials
Pneumatic conveying systems operate by using air or gas to transport bulk materials, such as coffee beans or ground coffee, through a pipeline network. The process typically involves a combination of positive and negative pressure or a vacuum system to move the material from the source to the destination. For coffee materials, which are often delicate and require gentle handling, specialized designs are employed to minimize product degradation and ensure consistent quality. The equipment utilizes a series of components, including a hopper, a rotary valve, a conveyor line, and a receiver, all working in tandem to achieve efficient and reliable material transport. The principle of air suspension, where the material is suspended in a stream of air, allows for smooth and low-friction movement, reducing the risk of breakage or contamination. This method is particularly advantageous for coffee, as it preserves the aroma and integrity of the product during transit.
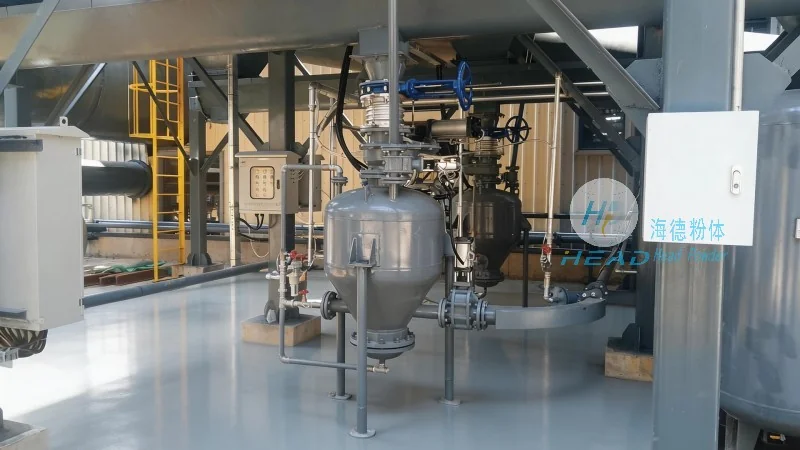
Key Working Scene Characteristics of Coffee Material Pneumatic Conveying Equipment
The application of coffee material pneumatic conveying equipment varies across different working scenarios, each tailored to meet specific operational needs. In coffee processing plants, these systems are commonly used for transferring raw coffee beans from storage silos to roasting machines or for moving ground coffee from grinding units to packaging lines. The flexibility of pneumatic conveyors allows for vertical, horizontal, or inclined transport, adapting to the layout of the facility. In warehouse environments, they are employed to move coffee products between storage areas, loading docks, and shipping zones, enhancing workflow efficiency and reducing manual handling. The equipment's ability to handle different particle sizes and moisture contents makes it suitable for various coffee processing stages, from raw bean handling to final product packaging. Additionally, the systems are designed with hygiene and safety in mind, featuring easy-to-clean components and compliance with industry standards, ensuring that the coffee remains free from contaminants and meets quality regulations.
Advantages and Practical Applications in Coffee Industry Settings
Implementing coffee material pneumatic conveying equipment offers several benefits that enhance operational performance. The primary advantage is the reduction in labor costs and manual handling, as the system automates the material transport process. This not only improves efficiency but also minimizes the risk of product damage and workplace injuries. Furthermore, the systems provide a clean and dust-free environment, which is crucial for maintaining the quality and aroma of coffee products. The compact design of the equipment allows for installation in limited spaces, making it suitable for both large-scale processing facilities and smaller coffee roasting shops. In terms of practical applications, these systems are widely used in coffee roasting, grinding, and packaging operations, where consistent and reliable material transport is essential. The ability to handle high volumes of coffee materials at a steady rate ensures that production lines run smoothly without interruptions. Moreover, the systems can be integrated with other processing equipment, such as sorting machines or flavoring units, creating a seamless workflow that optimizes the entire coffee production process.
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., based in Shandong, China, is at the forefront of developing innovative coffee material pneumatic conveying solutions. With a focus on precision engineering and customer-centric design, the company provides equipment that meets the unique demands of the coffee industry. By leveraging advanced technology and adhering to international standards, HeadPowder ensures that its products deliver superior performance, reliability, and durability. The company's commitment to quality and customer satisfaction has established it as a trusted partner for coffee processing facilities worldwide, helping businesses enhance their operational efficiency and maintain the highest standards of product quality.