

Sulfate Ammonium Pneumatic Conveying: A Material Handling Solution to Overcome Distance Limitations
Efficient and reliable material handling is a critical factor in the production and processing of sulfate ammonium, a widely used fertilizer and chemical raw material. Traditional conveying methods often face limitations in terms of distance and complexity, which can impact operational efficiency and cost-effectiveness. This is where pneumatic conveying systems emerge as a transformative solution, enabling the seamless transport of sulfate ammonium over extended distances with enhanced flexibility and reduced maintenance requirements.
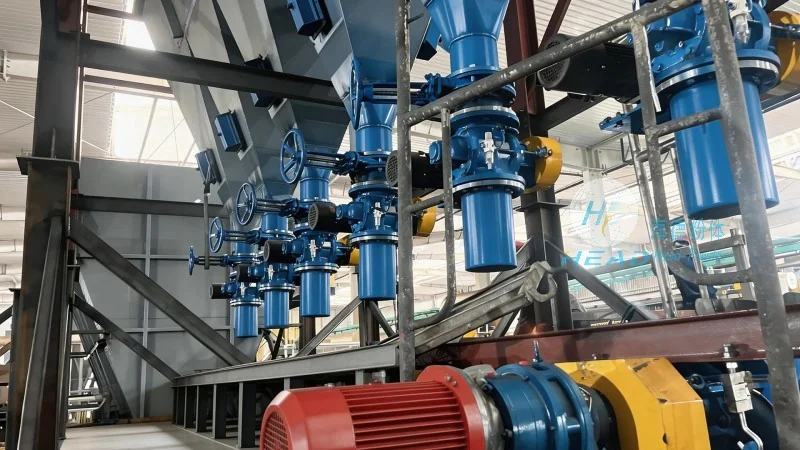
Pneumatic Conveying Technology for Sulfate Ammonium: Advantages and Applications
Sulfate ammonium, also known as ammonium sulfate, is a key component in agricultural and industrial applications due to its high nitrogen content and versatility. Conventional methods like belt conveyors or bucket elevators may struggle with long-distance transport, especially when dealing with fine powders that are prone to dust and clogging. Pneumatic conveying, however, offers a superior alternative by utilizing air pressure to move material through a pipeline network. This technology not only overcomes the distance limitations but also provides a dust-free and enclosed transport environment, minimizing environmental impact and ensuring product integrity.
HeadPowder Engineering: Leading Provider of Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a prominent manufacturer and supplier of advanced pneumatic conveying systems tailored for sulfate ammonium and other bulk materials. With a strong presence in China, particularly in Shandong province, HeadPowder has established itself as a trusted partner in the chemical and fertilizer industries. The company specializes in designing, manufacturing, and installing customized pneumatic conveying solutions that meet the specific needs of clients, ensuring optimal performance and durability in demanding operational environments.
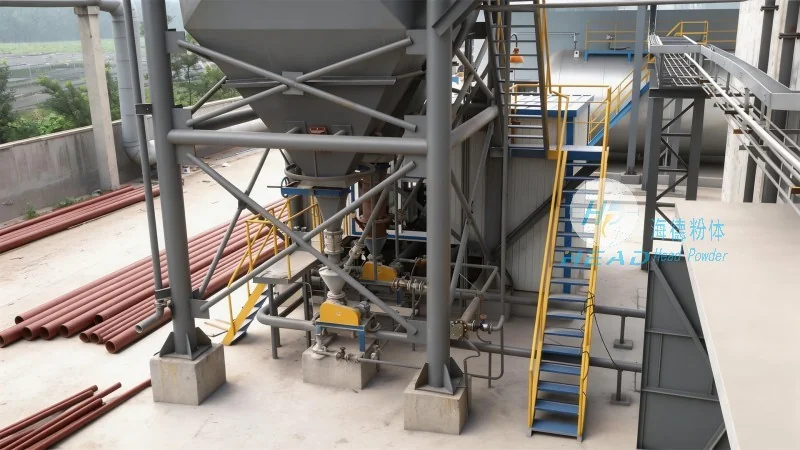
Key Features of HeadPowder's Pneumatic Conveying Systems
HeadPowder's pneumatic conveying systems for sulfate ammonium are engineered with precision to deliver high efficiency and reliability. These systems typically incorporate components such as feeders, airlocks, cyclones, and dust collectors, all working in harmony to ensure smooth material flow. The use of positive pressure or negative pressure conveying methods allows for flexibility in system design, accommodating various distance requirements and layout configurations. Additionally, the systems are equipped with advanced control mechanisms that monitor pressure, flow rate, and material level, providing real-time operational data and enhancing process control.
Customization and Integration: Meeting Unique Operational Needs
Every industrial facility has distinct operational requirements, and HeadPowder recognizes the importance of customization in delivering effective solutions. The company works closely with clients to understand their specific challenges, such as the need for long-distance transport, high material throughput, or integration with existing production lines. By leveraging its expertise in material handling and process engineering, HeadPowder designs tailored pneumatic conveying systems that optimize performance while minimizing downtime and maintenance costs. This approach ensures that clients receive a solution that is not only efficient but also adaptable to future growth and technological advancements.
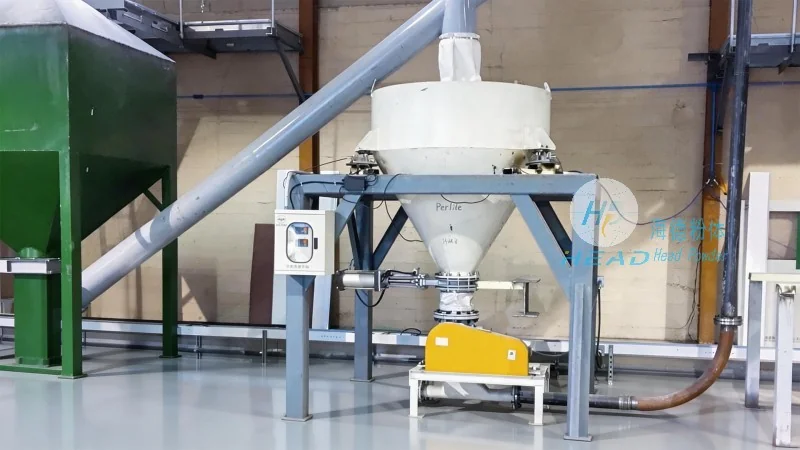
Quality Assurance and Reliability: Ensuring Long-Term Performance
At HeadPowder, quality is a top priority, reflected in the rigorous testing and validation of all pneumatic conveying systems. The company adheres to international standards and employs advanced manufacturing techniques to ensure the durability and longevity of its equipment. Regular maintenance and support services are also provided to clients, ensuring that the systems operate at peak performance throughout their service life. This commitment to quality and reliability has earned HeadPowder a reputation for delivering dependable solutions that meet the highest industry standards.
Conclusion: Enhancing Material Handling with Pneumatic Conveying
In conclusion, pneumatic conveying systems represent a significant advancement in the efficient transport of sulfate ammonium, offering a solution to the traditional limitations of distance and complexity. HeadPowder Engineering, with its expertise and commitment to quality, provides state-of-the-art pneumatic conveying solutions that enhance operational efficiency, reduce costs, and ensure product integrity. By choosing HeadPowder's systems, clients can achieve reliable and sustainable material handling, supporting their production processes and contributing to overall business success.