

Potassium Sulfate Pneumatic Conveying Solutions
HeadPowder, a leading engineering firm based in Shandong, China, specializes in providing advanced pneumatic conveying systems tailored for the efficient handling and transportation of potassium sulfate. This article explores the key aspects of our solutions, focusing on technical innovations, operational benefits, and practical applications in industrial settings.
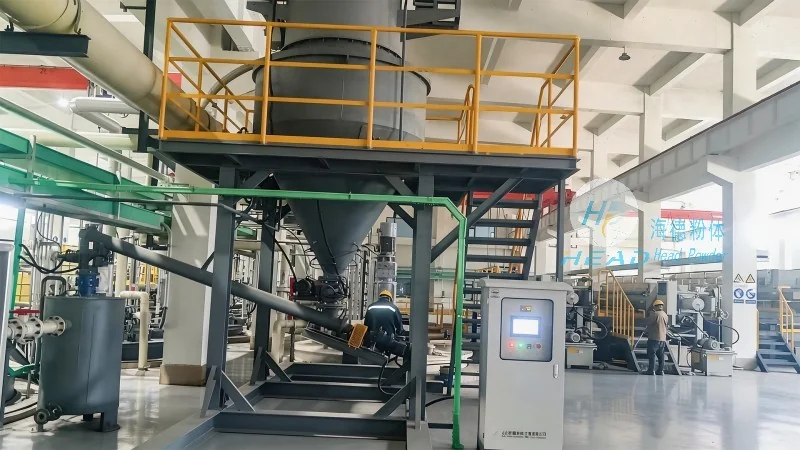
Understanding Pneumatic Conveying for Potassium Sulfate
Potassium sulfate, a critical fertilizer and industrial chemical, requires reliable and efficient material handling to ensure consistent quality and minimize operational disruptions. Pneumatic conveying systems offer a non-contact, low-maintenance method for transporting bulk materials like potassium sulfate, addressing challenges such as dust control, material degradation, and environmental compliance. Our solutions are designed to meet the specific demands of potassium sulfate processing, from raw material intake to final product delivery.
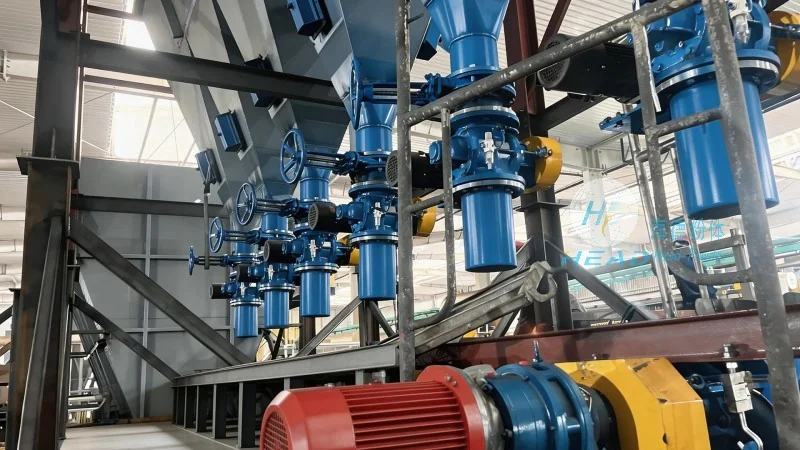
Key Technical Features of Our Pneumatic Conveying Systems
At Shandong HeadPowder Engineering Co., Ltd., we leverage cutting-edge technology to develop customized pneumatic conveying solutions. Our systems incorporate several key features that enhance performance and reliability:
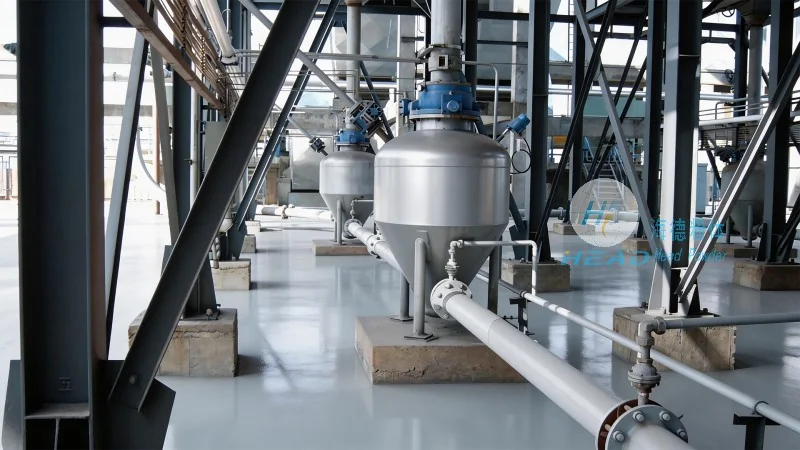
- Positive Pressure Conveying: Utilizes compressed air to push material through pipelines, ensuring consistent flow rates and preventing material degradation.
- Material Handling Flexibility: Adaptable to various particle sizes and moisture content, accommodating different grades of potassium sulfate.
- Low Maintenance Design: Simplified components and robust construction reduce downtime and operational costs.
- Dust and Environmental Control: Integrated filtration systems and sealed pipelines minimize dust emissions, adhering to environmental regulations.
Operational Benefits for Potassium Sulfate Handling
Implementing our pneumatic conveying solutions for potassium sulfate processing delivers significant operational advantages:
- Enhanced Product Quality: Non-contact transport prevents contamination and material breakdown, maintaining the purity and quality of potassium sulfate.
- Improved Safety: Enclosed systems reduce exposure to dust and hazardous materials, creating a safer working environment.
- Increased Efficiency: Automated conveying processes streamline material flow, reducing labor costs and improving overall production throughput.
- Scalable Solutions: Systems can be scaled to accommodate varying production volumes, from small-scale operations to large industrial facilities.
Application Scenarios and Customization
Our pneumatic conveying solutions are versatile and can be applied in diverse industrial settings, including:
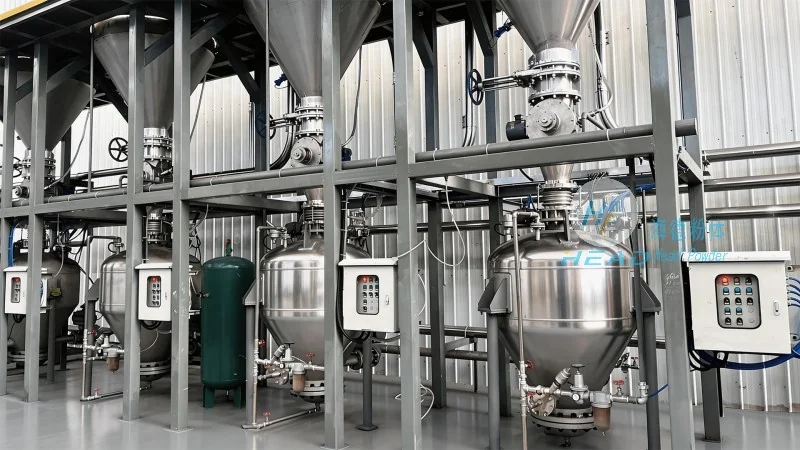
- Raw Material Handling: Efficient intake and transfer of potassium sulfate from storage silos or bulk containers.
- Process Integration: Seamless integration with existing fertilizer production lines, ensuring smooth material flow between processing stages.
- Product Packaging: Precise delivery of potassium sulfate to packaging equipment, minimizing waste and maximizing output.
- Waste Management: Safe and controlled transport of byproducts or waste materials from processing facilities.
Conclusion and Company Overview
Shandong HeadPowder Engineering Co., Ltd. is committed to delivering high-quality, customized pneumatic conveying solutions for potassium sulfate applications. With our expertise in engineering and material handling, we provide reliable systems that enhance operational efficiency, ensure product quality, and meet environmental standards. Based in Shandong, China, our team of professionals works closely with clients to understand their specific needs and develop tailored solutions that drive success in the fertilizer and chemical industries.