

Working Principle and Features of Coke Particle Powder Pneumatic Conveying Equipment
For industrial applications involving the transport of coke particles and powders, the pneumatic conveying system is a critical piece of equipment. This equipment, manufactured by Shandong HeadPowder Engineering Co., Ltd., is designed to efficiently handle the movement of coke particles from one location to another within a facility. The following sections will explore the working principle and key features of this specialized equipment.
Working Principle of Coke Particle Powder Pneumatic Conveying Equipment
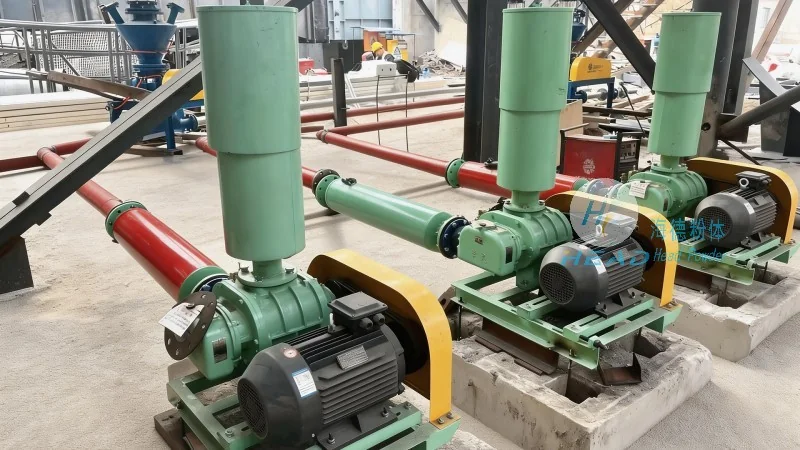
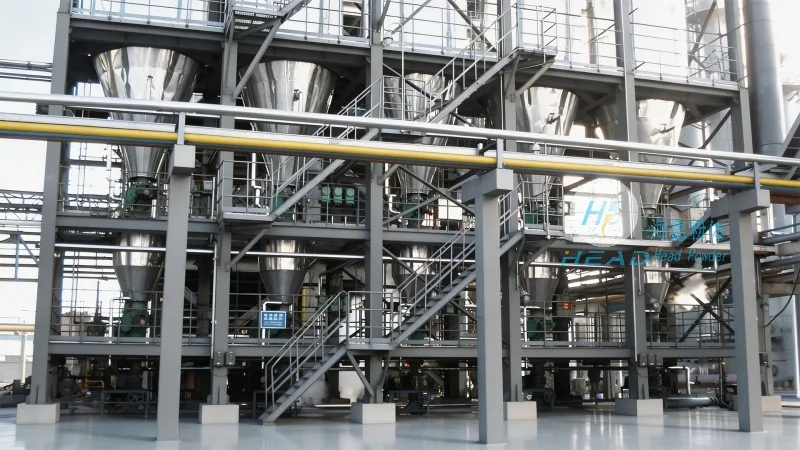
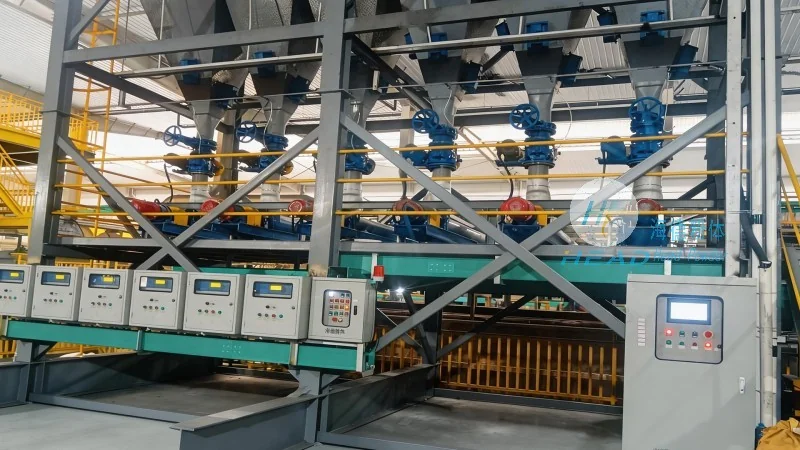
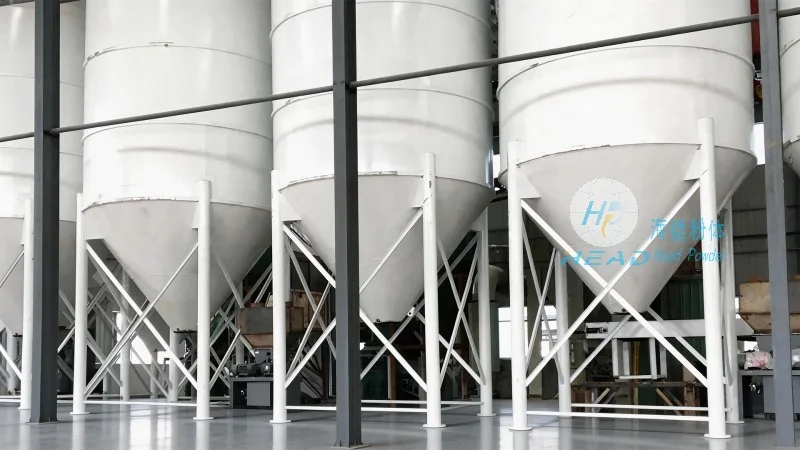
The pneumatic conveying system for coke particles operates on the principle of air movement to transport solid materials. This equipment, produced by Shandong HeadPowder Engineering Co., Ltd., utilizes either positive pressure or negative pressure to achieve material transport. The process begins with the coke particles being fed into the system through a hopper or feeder. The air is then introduced into the pipeline by a blower or compressor. In a positive pressure system, the blower pushes air through the pipeline, creating a high-pressure environment that forces the coke particles along the path. This method is suitable for long-distance or complex pipeline configurations where maintaining consistent air flow is crucial. Conversely, a negative pressure system uses a vacuum to draw air and coke particles into the pipeline. This approach is often used for shorter distances or in enclosed spaces where dust containment is a priority. The air flow entrains the coke particles, carrying them through the pipeline. At the discharge end, a separator, such as a cyclone separator or bag filter, separates the coke particles from the air. The separated particles are collected in a storage bin, while the air is either filtered and released or recirculated back into the system. This continuous cycle ensures efficient and reliable transport of coke particles, minimizing material loss and operational downtime.
Key Features of the Coke Particle Powder Pneumatic Conveying Equipment
The coke particle powder pneumatic conveying equipment from Shandong HeadPowder Engineering Co., Ltd. is engineered with several key features that enhance its performance and usability in industrial settings. One of the standout features is its high efficiency in material handling. By leveraging air as the conveying medium, the system can transport large volumes of coke particles at a rapid pace while consuming less energy compared to traditional mechanical conveying methods like belt conveyors or bucket elevators. This efficiency is particularly advantageous in steel production and coke processing plants, where large quantities of coke are processed daily. Another critical feature is the system's adaptability to various particle characteristics. It can handle a wide range of coke particle sizes, from fine powders to larger chunks, without experiencing clogging or damage to components. This flexibility makes it suitable for diverse applications, including blending fine coke powders for quality control or moving larger coke pieces for further processing in furnaces. The equipment also prioritizes environmental sustainability by reducing dust emissions. The enclosed pipeline and separation system effectively contain dust, minimizing the impact on workplace air quality and complying with environmental regulations. Additionally, the system is designed for low maintenance and easy operation. Constructed from durable materials that resist abrasion from coke particles, the components are built to last. The inclusion of features like automatic cleaning cycles and real-time monitoring ensures smooth operation and reduces the need for frequent maintenance, lowering operational costs. The system offers precise control over the material flow, allowing operators to adjust air pressure and flow rate to regulate the speed and quantity of coke particles being transported. This level of control is essential for maintaining consistent production processes and meeting strict quality standards. Furthermore, the equipment is compact and space-efficient, making it ideal for facilities with limited floor space. The modular design facilitates easy installation and integration into existing production lines, minimizing the need for major structural modifications. This adaptability allows the system to be customized to fit various plant layouts and operational requirements, ensuring optimal performance. Safety is also a key consideration in the design, with features such as explosion-proof components and overpressure protection to mitigate risks in environments where coke dust may be present. These safety measures ensure the equipment operates reliably and securely, providing peace of mind to operators and compliance with safety standards.