

Working Principle and Features of Carburizing Purification Ash Powder Pneumatic Conveying Equipment
Carburizing purification ash is a critical byproduct in the production of calcium carbide, and its efficient handling is essential for industrial processes. The pneumatic conveying system designed for this specific application, manufactured by Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated solution to manage the challenges associated with ash powder transport. This article explores the working principle and key features of this equipment, providing insights into its design and operational benefits.
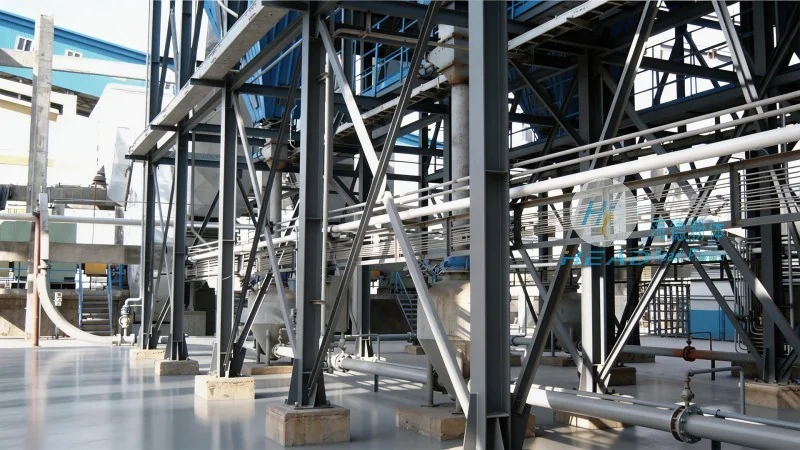
Introduction to Carburizing Purification Ash Pneumatic Conveying Systems
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in engineering solutions for powder handling and material transport. The company’s expertise in pneumatic conveying technology is evident in the development of systems tailored for carburizing purification ash, a fine powder that requires specialized equipment to ensure safe and efficient movement. The equipment is designed to handle the unique properties of ash powder, including its dustiness and potential reactivity, while maintaining operational efficiency and reliability.
Working Principle of the Pneumatic Conveying Machine
The core of the carburizing purification ash pneumatic conveying system is its ability to transport powder through a pressurized or vacuum environment. The system operates by generating a flow of air or gas that propels the ash particles through a pipeline network. In a typical setup, the ash is first collected from the purification process and fed into a hopper or feeder. From there, it is introduced into the conveying line, where the air flow, either positive pressure (blower-driven) or negative pressure (vacuum-driven), moves the powder to the desired destination, such as a storage silo or processing unit. The working principle involves precise control of air pressure, flow rate, and particle size to ensure optimal conveying performance. The system is equipped with components like rotary valves, airlocks, and filters to regulate the flow and prevent clogging or dust emissions.
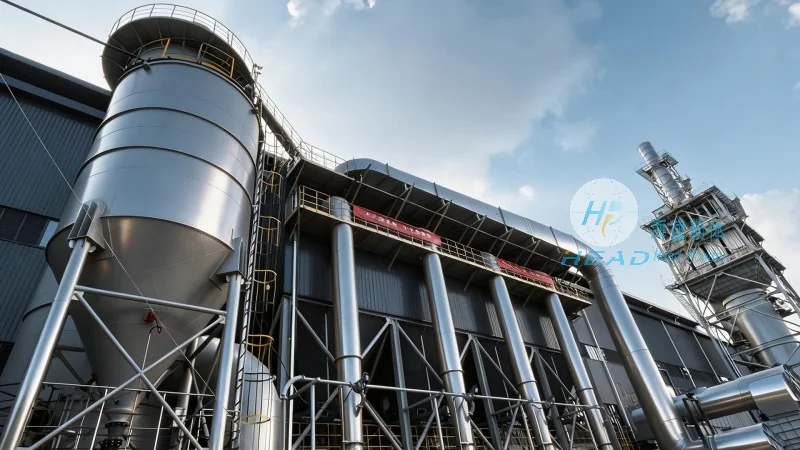
Key Features and Technical Specifications
The pneumatic conveying equipment for carburizing purification ash from Shandong HeadPowder Engineering Co., Ltd. incorporates several advanced features that enhance its performance and usability. One of the primary features is the use of high-efficiency blower systems that provide consistent air pressure, ensuring reliable transport of fine ash particles without degradation. The system is designed with robust materials, such as stainless steel or corrosion-resistant alloys, to withstand the chemical and physical properties of the ash, preventing material degradation or equipment wear. Additionally, the equipment includes advanced control systems that allow for real-time monitoring of pressure, flow, and particle concentration, enabling operators to adjust parameters for optimal performance. The design also emphasizes safety, with features like dust collection systems and explosion-proof components to mitigate risks associated with handling fine powders. The system’s modular design allows for easy integration into existing industrial setups, providing flexibility in installation and operation.
Advantages of Using Pneumatic Conveying for Ash Handling
Compared to traditional methods like belt conveyors or bucket elevators, pneumatic conveying offers several advantages for handling carburizing purification ash. The primary benefit is the ability to transport fine powders over long distances without the need for multiple transfer points, reducing the risk of material loss or contamination. The system also eliminates the need for physical contact between the ash and the conveying equipment, minimizing wear and tear and extending the equipment’s lifespan. Furthermore, pneumatic conveying is more energy-efficient than other methods, as it requires less power to move the powder compared to mechanical systems. The system’s ability to handle varying particle sizes and moisture content makes it versatile for different industrial applications. The reduced labor requirements and automated control features also contribute to operational efficiency and cost savings for manufacturers.
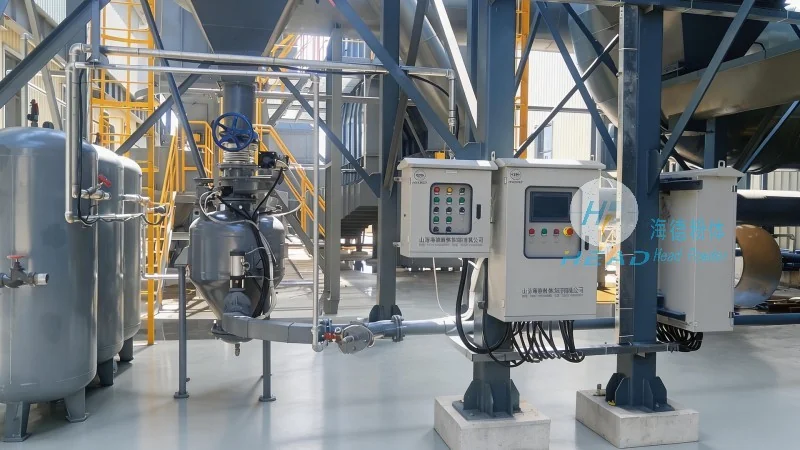
Application and Operational Considerations
The carburizing purification ash pneumatic conveying system is widely used in the chemical and metallurgical industries, where efficient handling of ash byproducts is critical. The system is typically integrated into the production line of calcium carbide plants, where the ash is generated during the purification process. Operational considerations include the need for regular maintenance of the blower and filter systems to ensure consistent performance. The system’s design allows for easy cleaning and maintenance, with components that can be accessed and serviced without disrupting the entire operation. The use of advanced sensors and control systems enables operators to monitor the system’s performance in real-time, detecting any issues such as clogging or pressure drops promptly. The system’s ability to handle high volumes of ash efficiently makes it suitable for large-scale industrial operations, where consistent and reliable material transport is essential for maintaining production schedules.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. has developed a sophisticated pneumatic conveying system for carburizing purification ash that combines advanced technology with robust design. The system’s working principle, based on pressurized or vacuum air flow, ensures efficient transport of fine ash particles while maintaining operational safety and reliability. Key features such as high-efficiency blower systems, corrosion-resistant materials, and advanced control features enhance the system’s performance and usability. The advantages of pneumatic conveying, including long-distance transport, reduced material loss, and energy efficiency, make it an ideal solution for handling carburizing purification ash. With its application in the chemical and metallurgical industries, this equipment contributes to improved operational efficiency and cost savings for manufacturers. The system’s design and functionality reflect the company’s expertise in powder handling technology, providing a reliable solution for industrial ash management.