

[FREE]Food Powder Conveying: An Introduction to Structure and Working Principles
Food powder conveying systems are essential in the food processing industry, ensuring efficient and hygienic movement of bulk materials. This article provides an overview of the key components, structural design, and operational principles of food powder conveying equipment, highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd. as a leading manufacturer in this field.
Understanding Food Powder Conveying Systems
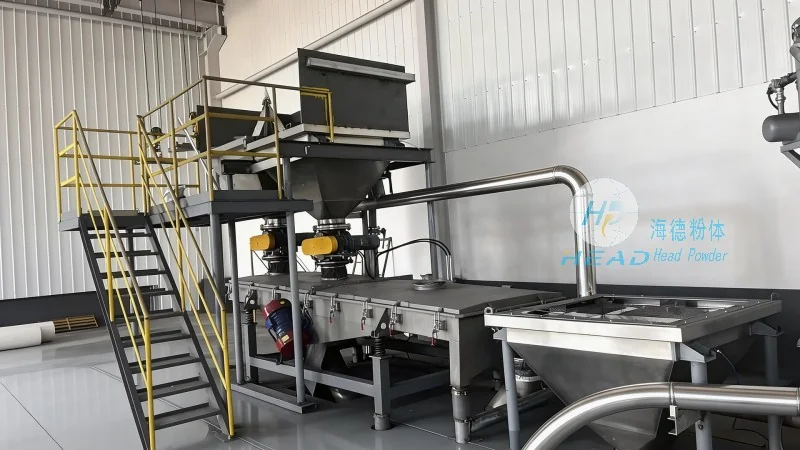
Food powder conveying involves the transportation of fine, dry particles such as flour, sugar, and other food ingredients from one processing stage to another. The effectiveness of these systems directly impacts production efficiency, product quality, and overall operational costs. A well-designed conveying system must adhere to strict hygiene standards, as food products are highly sensitive to contamination and require clean, reliable equipment.
Core Components and Structural Design
The structure of a typical food powder conveying system includes several critical components that work in tandem to ensure smooth operation. These components include the hopper, which serves as the storage and feeding unit, the conveyor itself (e.g., screw, pneumatic, or belt conveyor), and the control mechanisms that regulate the flow rate and direction. The design of each component is tailored to the specific characteristics of the food powder, such as particle size, moisture content, and flowability. For instance, the hopper may feature a conical or rectangular shape to minimize material bridging and ensure consistent feeding. The conveyor may use stainless steel or food-grade materials to prevent corrosion and maintain hygiene standards. Additionally, the system incorporates seals and gaskets to prevent dust leakage and maintain a clean environment.
Working Principles of Food Powder Conveying
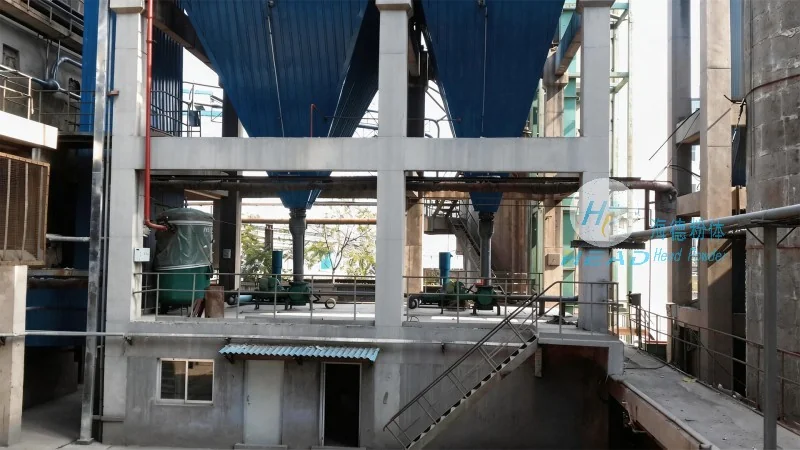
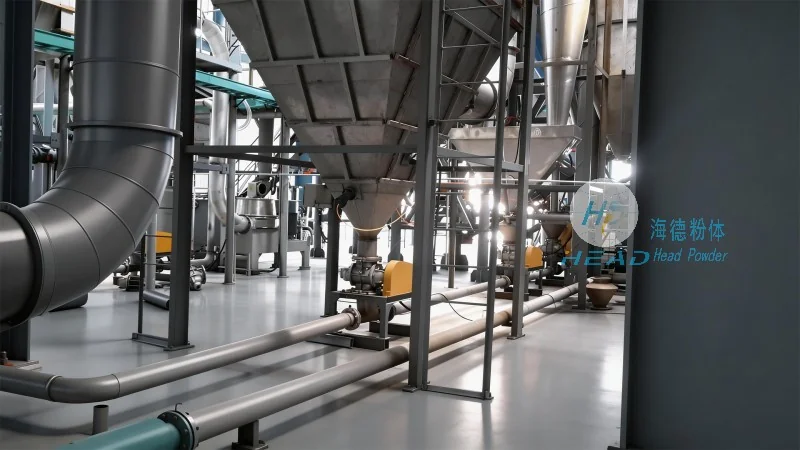
The operational principle of a food powder conveying system varies depending on the type of equipment used. The most common methods include mechanical, pneumatic, and gravity-based conveying. Mechanical conveyors, such as screw conveyors, use rotating screws to push the powder forward through a tube or trough. This method is suitable for materials with moderate flowability and can handle a wide range of particle sizes. Pneumatic conveyors, on the other hand, utilize air pressure to transport the powder in a sealed system. This method is ideal for fine powders that are prone to dusting and requires less maintenance compared to mechanical systems. Gravity conveyors rely on the natural slope of the system to move the powder, which is suitable for short-distance transportation and low-volume applications. Regardless of the method, the system must maintain a consistent flow rate to prevent clogging and ensure uniform material distribution.
Applications in the Food Industry
Food powder conveying systems are widely used in various stages of food production, from raw material handling to packaging. In the baking industry, for example, flour and sugar are conveyed from storage silos to mixing machines. In the dairy industry, powdered milk is transported from production lines to storage tanks. The versatility of these systems allows them to adapt to different production requirements, whether it's high-volume processing or small-scale batch production. The ability to handle different food powders without compromising quality makes them indispensable in modern food processing facilities.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of food powder conveying equipment. With a focus on innovation and quality, the company specializes in designing and manufacturing systems that meet the stringent requirements of the food industry. Headpowder's products are engineered to ensure high efficiency, low maintenance, and compliance with international hygiene standards. The company's team of experts works closely with clients to understand their specific needs and provide customized solutions that enhance production capabilities. Headpowder's commitment to excellence has earned it a reputation as a trusted partner in the food processing sector, serving clients both domestically and internationally.