

Glass Particle Pneumatic Conveying: How to Efficiently Transport Bulk Powders with Air Flow
When it comes to transporting glass particles and other fine bulk materials, the efficiency and reliability of the conveying system are critical factors. Glass particles, with their unique properties such as fragility and varying sizes, require specialized handling methods to prevent breakage and ensure smooth operation. This is where pneumatic conveying technology comes into play, offering a solution that leverages air flow to move materials with precision and control.
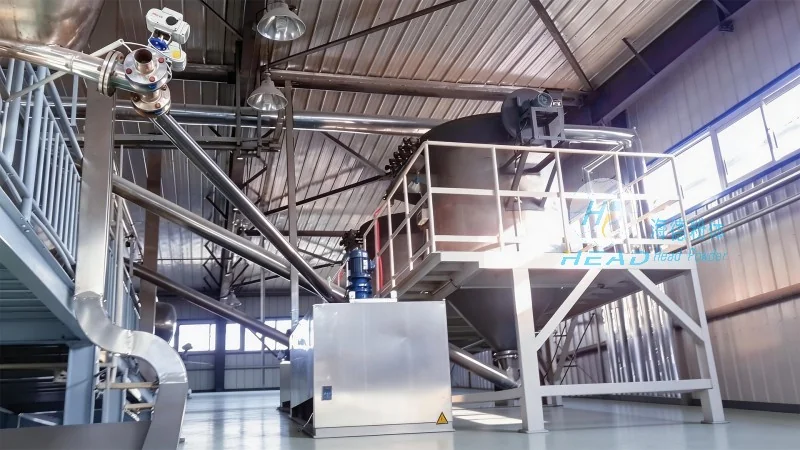
HeadPowder, a leading provider of engineering solutions for material handling, specializes in designing and implementing pneumatic conveying systems tailored to the specific needs of glass particle applications. With years of experience in the industry, HeadPowder understands the challenges associated with handling glass particles, including the risk of particle attrition, system clogging, and uneven flow. By addressing these challenges through innovative design and advanced technology, HeadPowder delivers systems that enhance productivity while maintaining the quality of the glass particles.
One of the key aspects of efficient glass particle pneumatic conveying is the selection of the right air flow parameters. The velocity of the air, the pressure, and the system design all play crucial roles in determining the effectiveness of the conveying process. HeadPowder’s engineers utilize advanced computational fluid dynamics (CFD) and material testing to optimize these parameters for each client's specific glass particle characteristics. This ensures that the air flow is sufficient to lift and transport the particles without causing excessive wear or damage to the system components.
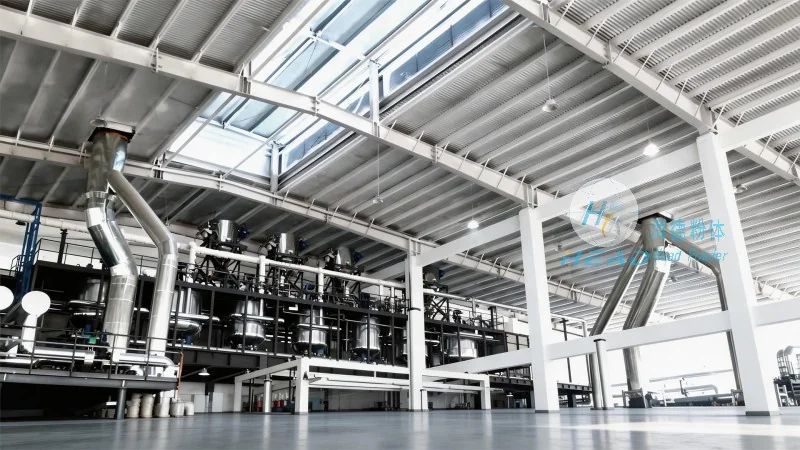
Another critical component in glass particle pneumatic conveying is the choice of equipment. HeadPowder offers a range of equipment, including rotary valves, airlocks, and cyclone separators, all designed to handle glass particles effectively. The rotary valves, for instance, are engineered to provide a consistent flow of glass particles into the conveying line, while the airlocks prevent backflow and maintain system pressure. The cyclone separators, on the other hand, efficiently separate the glass particles from the air stream, allowing for clean material recovery and reducing waste. Each piece of equipment is carefully selected and integrated into the system to ensure seamless operation and minimal downtime.
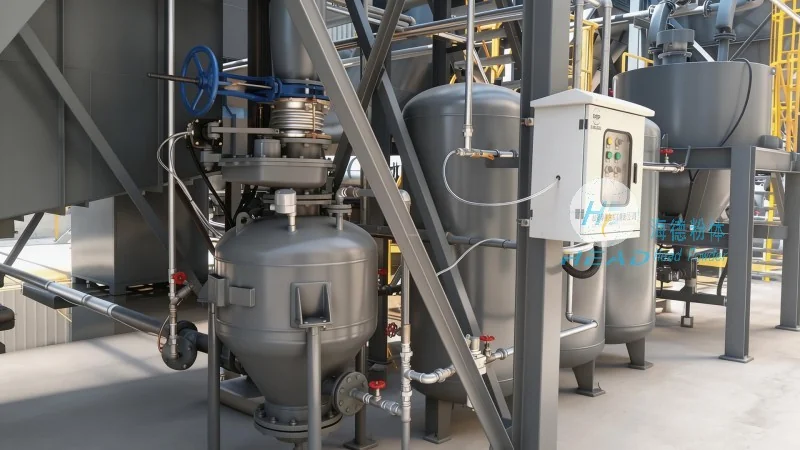
HeadPowder’s approach to glass particle pneumatic conveying also emphasizes system integration and maintenance. The company provides comprehensive support, from initial system design and installation to ongoing maintenance and troubleshooting. This includes regular inspections of the conveying lines, cleaning of equipment, and replacement of worn parts. By maintaining the system in optimal condition, HeadPowder helps clients achieve consistent performance and extend the lifespan of their equipment. The company’s team of experienced technicians is available to provide on-site support, ensuring that any issues are addressed promptly and effectively.
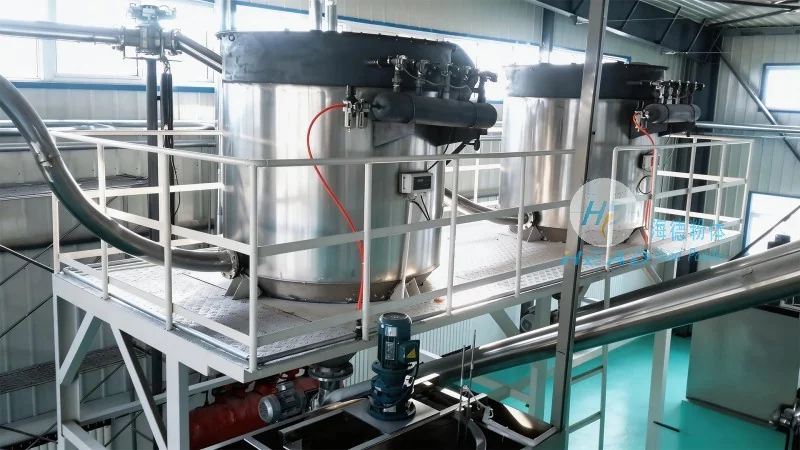
Furthermore, HeadPowder’s commitment to sustainability and environmental responsibility is reflected in its pneumatic conveying solutions. The systems are designed to minimize energy consumption and reduce emissions, contributing to a greener and more sustainable operation. By using efficient air flow and energy-saving components, HeadPowder helps clients reduce their carbon footprint while maintaining high levels of productivity. This approach aligns with the growing demand for eco-friendly solutions in the material handling industry.
For businesses dealing with glass particles, choosing the right pneumatic conveying system is essential for maximizing efficiency and minimizing costs. HeadPowder’s expertise in glass particle handling, combined with its innovative technology and comprehensive support, makes it the ideal partner for achieving efficient and reliable material transport. By leveraging the power of air flow, HeadPowder’s systems enable businesses to streamline their operations, improve product quality, and stay competitive in the market.