

What is Red Sugar Material Handling? What Are Its Design Principles?
Red sugar material handling refers to the process of transporting and managing red sugar, a type of unrefined sugar, from its source to various processing or storage stages. This involves the use of specialized equipment and systems to ensure efficient and safe movement of the raw material. The design principles behind such systems are crucial for optimizing workflow, maintaining product quality, and ensuring operational efficiency in sugar processing facilities.
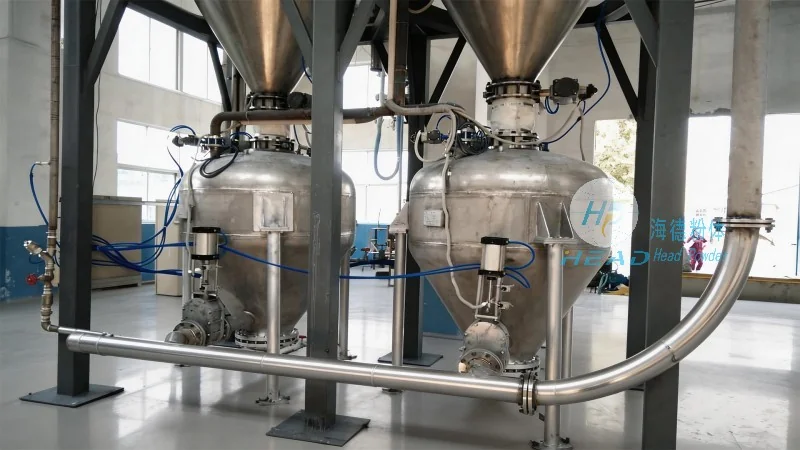
Understanding Red Sugar Material Handling
Red sugar, also known as brown sugar or unrefined cane sugar, is produced through the extraction of juice from sugarcane and subsequent processing steps that retain molasses content. Unlike white refined sugar, red sugar retains its natural color and flavor, making it a popular choice in culinary applications and traditional food production. Material handling for red sugar involves handling bulk quantities of this granular or crystalline material, which requires specialized equipment to prevent breakage, contamination, and loss during transport.
Key Design Principles for Red Sugar Material Handling Systems
The design of red sugar material handling systems is guided by several fundamental principles aimed at maximizing efficiency and preserving product integrity. These principles include:
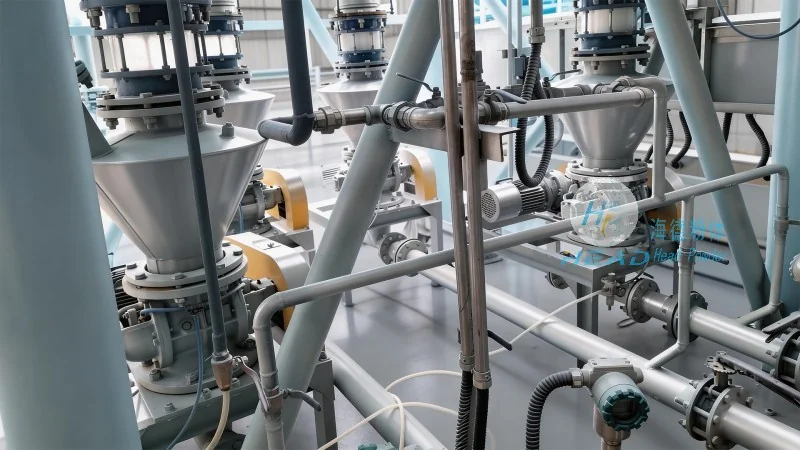
- Material Compatibility: Equipment must be constructed from materials that are non-reactive with red sugar and its components, such as molasses and minerals. Common materials include stainless steel, which resists corrosion and maintains hygiene standards.
- Prevention of Product Degradation: Systems are designed to minimize exposure to air, moisture, and temperature fluctuations, which can affect the color, flavor, and crystalline structure of red sugar. This is achieved through enclosed conveyors, airtight storage tanks, and temperature-controlled environments.
- Efficient Flow and Minimization of Friction: The layout and components of the handling system are optimized to reduce friction and impact on the sugar crystals. This includes using smooth, rounded surfaces on conveyor belts and chutes, as well as gentle inclines to prevent breakage or caking.
- Hygiene and Sanitation: Given that red sugar is often used in food applications, the handling system must be easily cleanable and maintain high sanitary standards. This involves features like removable parts, easy-to-clean surfaces, and the ability to perform thorough cleaning and disinfection cycles.
Components of a Typical Red Sugar Material Handling System
A comprehensive red sugar material handling system typically includes several key components that work in tandem to ensure smooth operation. These components may include:
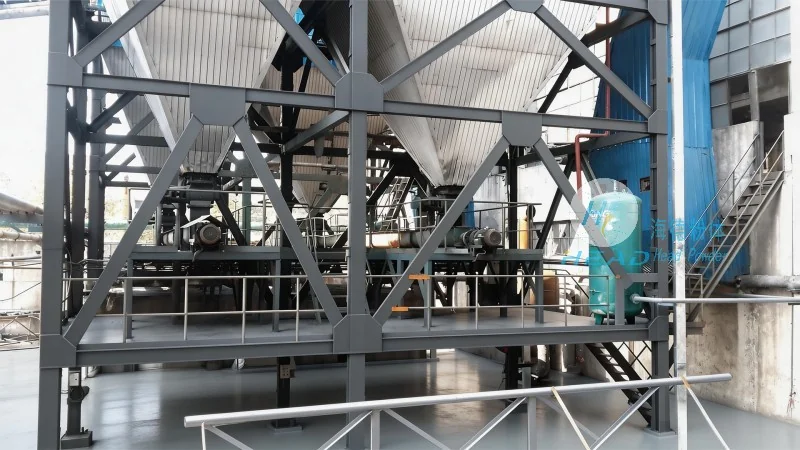
- Feeders and Hoppers: These devices are used to collect and feed red sugar from storage silos or bulk containers into the handling system. They are designed to handle bulk material and maintain a consistent flow rate.
- Conveyors: Conveyors, such as belt conveyors or screw conveyors, are used to transport red sugar horizontally or vertically. Belt conveyors are preferred for their ability to handle granular materials without causing excessive breakage, while screw conveyors are suitable for vertical transport and can also be used for mixing or dosing.
- Chutes and Baffles: Chutes are used to direct the flow of red sugar from one component to another, while baffles help to control the flow and prevent clogging. These components are often lined with non-stick materials to reduce friction and prevent product buildup.
- Storage Tanks and Silos: After processing, red sugar may be stored in large tanks or silos. These storage vessels are designed to maintain the product's quality and are equipped with aeration systems to prevent caking and maintain consistent moisture levels.
- Control Systems: Modern material handling systems often include automated control systems that monitor and regulate the flow of red sugar. These systems use sensors to detect levels, flow rates, and potential blockages, and can adjust the operation of the equipment in real-time to maintain optimal performance.
Applications and Benefits of Red Sugar Material Handling
Red sugar material handling systems are widely used in various industries, including food processing, pharmaceuticals, and chemical manufacturing. The benefits of implementing an efficient material handling system include:
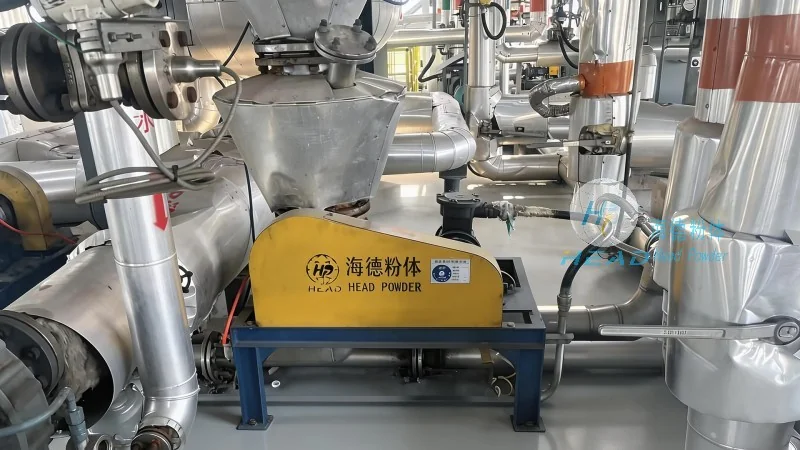
- Increased Productivity: By streamlining the movement of red sugar, these systems reduce downtime and increase the overall throughput of the processing facility.
- Improved Product Quality: Proper handling minimizes damage to the sugar crystals, preserving their natural color, flavor, and nutritional properties.
- Enhanced Safety: Enclosed systems and automated controls reduce the risk of accidents and exposure to the material, improving workplace safety.
- Cost Savings: Efficient handling reduces waste and lowers operational costs associated with material handling, such as labor and equipment maintenance.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of engineering solutions for material handling and processing, specializes in designing and manufacturing customized systems for various bulk materials, including red sugar. With a focus on innovation and quality, the company has built a reputation for delivering reliable and efficient solutions that meet the unique needs of its clients. HeadPowder Engineering is committed to providing sustainable and cost-effective solutions that enhance operational performance and product quality in the sugar industry and beyond.
Location
Headquartered in Shandong, China, Shandong HeadPowder Engineering Co., Ltd. leverages its local expertise and resources to serve clients worldwide. The company's strategic location allows for efficient supply chain management and quick response to customer needs, ensuring timely delivery of high-quality products and services.