

What is a Barley Material Handling Conveyor? And What Are Its Design Principles?
Barley material handling conveyors are essential systems in agricultural and food processing industries, designed to efficiently transport barley grains and related materials from one processing stage to another. These conveyors play a critical role in ensuring smooth operations, especially in facilities that handle large volumes of barley for milling, malting, or storage. The design of such conveyors is tailored to meet the specific characteristics of barley, including its size, density, and moisture content, to optimize performance and minimize material loss.
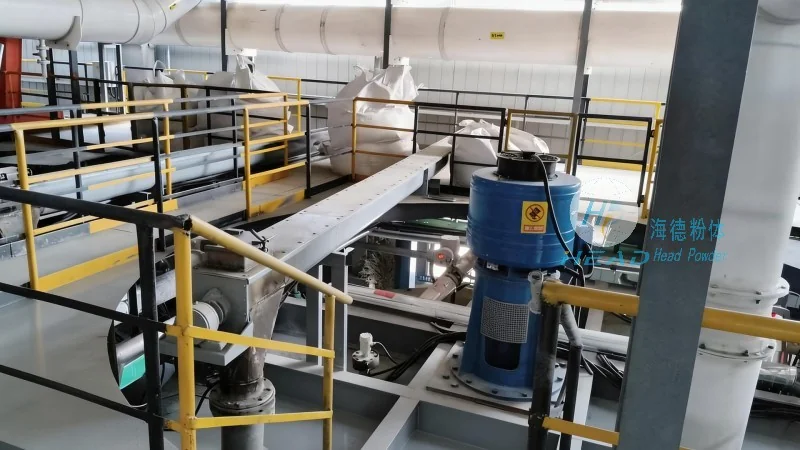
HeadPowder, a leading manufacturer based in Shandong, China, specializes in developing customized barley material handling solutions. With years of experience in the industry, the company understands the unique challenges associated with handling barley, such as its tendency to clump or stick, and designs conveyors that address these issues effectively. The company’s products are engineered to provide high reliability, durability, and efficiency, making them suitable for both small-scale and large-scale operations.
Core Design Principles for Barley Conveyors
The core design principle of a barley material handling conveyor involves the selection of appropriate conveyor types and components. For instance, belt conveyors are commonly used for horizontal or slight incline transport due to their ability to handle a wide range of material sizes and loads. The belt material is often chosen to prevent the barley from sticking, using materials like rubber or plastic with textured surfaces. Additionally, the conveyor’s speed and inclination angle are carefully calculated to maintain the flow of barley without causing excessive friction or breakage.
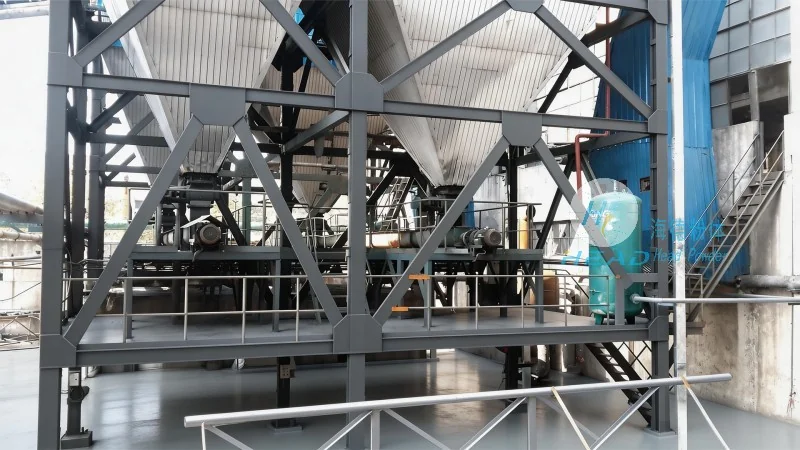
Another key design consideration is the integration of cleaning and maintenance features. Barley processing facilities require regular cleaning to prevent contamination and ensure product quality. The conveyor systems from HeadPowder are designed with easy-to-clean components, such as smooth surfaces and removable parts, which facilitate regular sanitation. This not only enhances hygiene but also reduces downtime for maintenance, contributing to overall operational efficiency.
Enhancing Safety and Operational Control
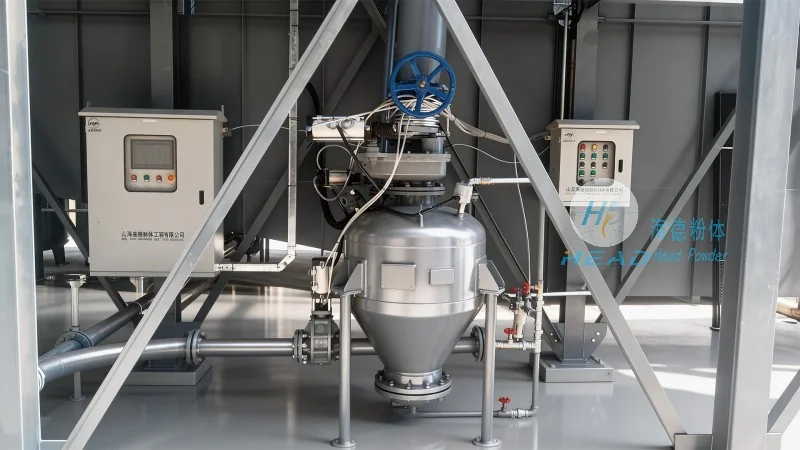
Material handling conveyors for barley also incorporate features that enhance safety and operational control. Sensors and control systems are integrated to monitor the flow of barley, detect blockages, and adjust the conveyor speed as needed. This ensures that the material is transported safely and efficiently, minimizing the risk of accidents or material damage. The control panels are typically user-friendly, allowing operators to easily adjust settings and monitor the system’s performance.
Quality and Innovation by HeadPowder
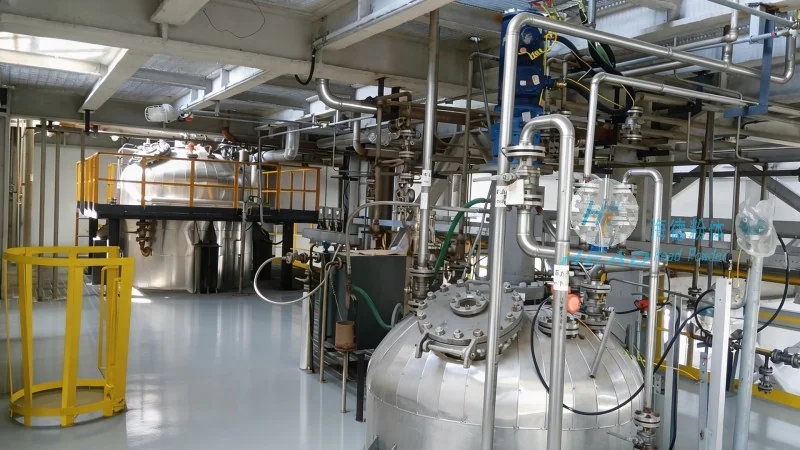
HeadPowder’s commitment to quality and innovation is reflected in the design and manufacturing of their barley material handling conveyors. The company adheres to strict quality control standards, ensuring that each component is tested for durability and performance. By using high-quality materials and advanced engineering techniques, HeadPowder’s conveyors are built to withstand the demands of continuous operation in barley processing facilities. This reliability is crucial for maintaining consistent production levels and reducing operational costs.
Furthermore, the design of these conveyors considers the environmental impact of barley processing. Energy-efficient motors and components are used to minimize power consumption, while the conveyor systems are designed to reduce noise and vibration, creating a more comfortable working environment. These considerations align with modern industry standards and help facilities meet environmental regulations.
Conclusion: Optimizing Barley Handling Operations
In conclusion, barley material handling conveyors are sophisticated systems that require careful design and engineering to meet the specific needs of barley processing. HeadPowder, with its expertise and commitment to quality, provides reliable and efficient solutions that enhance the productivity and safety of barley handling operations. By understanding the design principles and features of these conveyors, facilities can optimize their processing capabilities and ensure consistent product quality.