

Working Principle and Key Features of the Intelligent Centralized Powder Handling System
Efficient and reliable powder handling is a critical requirement in various industrial sectors, including pharmaceuticals, food processing, and chemical manufacturing. The intelligent centralized powder transport system, developed by Shandong HeadPowder Engineering Co., Ltd., addresses these needs by integrating advanced technology and robust design to ensure seamless material transfer. This article explores the working principle and key features of this innovative system, highlighting its benefits for modern industrial applications.
Company Background and Expertise
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in powder handling solutions. With years of experience in the industry, the company has built a strong reputation for delivering high-quality, customized systems that meet the specific demands of clients. HeadPowder's commitment to innovation and customer satisfaction has positioned it as a trusted partner for businesses seeking efficient powder transport solutions.
Overview of the Intelligent Centralized Powder Handling System
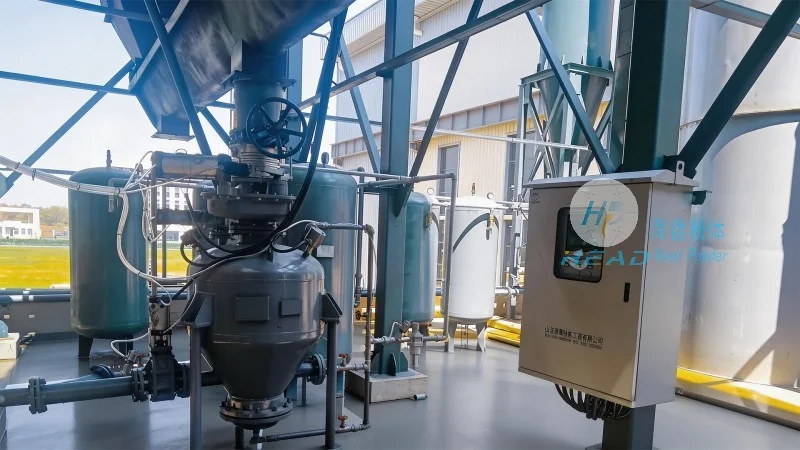
The intelligent centralized powder transport system is a comprehensive solution designed to manage the entire powder handling process from source to destination. It integrates various components such as feeders, conveyors, and control systems to ensure precise and controlled movement of powders. The system is engineered to handle a wide range of powder types, including fine powders, granules, and bulk materials, making it versatile for diverse industrial applications.
Working Principle of the System
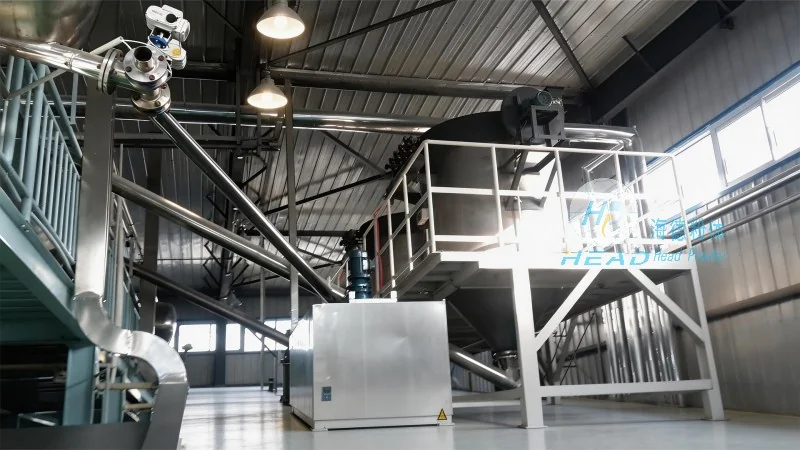
The core of the intelligent centralized powder handling system lies in its advanced control and automation mechanisms. The system operates based on a centralized control unit that coordinates the functions of all connected components. When a powder is to be transferred, the control unit sends signals to the appropriate feeder and conveyor, initiating the material flow. Sensors and monitoring devices are integrated throughout the system to provide real-time data on powder levels, flow rates, and system performance. This allows for immediate adjustments to maintain optimal operation and prevent issues such as clogging or overfilling.
Key Features and Advantages
The intelligent centralized powder handling system offers several key features that enhance its performance and reliability. One of the primary advantages is its automation capabilities, which reduce the need for manual intervention and minimize human error. The system is equipped with intelligent sensors that can detect changes in powder properties and adjust the handling process accordingly. This ensures consistent quality and reduces product waste. Additionally, the system features a user-friendly interface that allows operators to monitor and control the process easily, even from a remote location. The modular design of the system enables easy integration with existing facilities and allows for future expansion as business needs evolve.
Enhanced Safety and Environmental Compliance
Safety is a top priority in the design of the intelligent centralized powder handling system. The system incorporates various safety features, including dust extraction and containment measures, to prevent powder leakage and ensure a safe working environment. The enclosed design of the system minimizes the risk of dust exposure and complies with environmental regulations. Furthermore, the system is designed to be energy-efficient, reducing operational costs and minimizing the environmental impact. These features make the system suitable for industries where safety and environmental standards are stringent.
Application in Diverse Industries
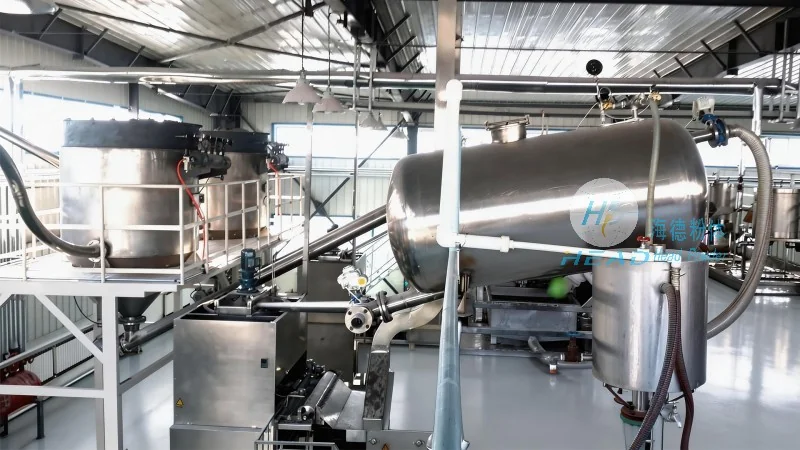
The intelligent centralized powder handling system is widely applicable across various industries due to its versatility and adaptability. In the pharmaceutical industry, it is used for handling active pharmaceutical ingredients (APIs) and excipients, ensuring precise dosing and maintaining product purity. In the food processing industry, the system is employed to handle ingredients such as flour, sugar, and spices, maintaining hygiene and quality standards. In the chemical manufacturing sector, it is used for transporting bulk chemicals, ensuring safe and efficient material transfer. The system's ability to handle different powder types and its customizable design make it a suitable solution for a wide range of applications.
Conclusion and Future Outlook
The intelligent centralized powder handling system by Shandong HeadPowder Engineering Co., Ltd. represents a significant advancement in powder transport technology. By combining advanced automation, robust design, and user-friendly features, the system offers enhanced efficiency, reliability, and safety for industrial applications. As industries continue to demand more efficient and sustainable solutions, this system is well-positioned to meet these needs and contribute to the growth and success of businesses in various sectors. With its commitment to innovation and customer satisfaction, HeadPowder remains at the forefront of developing cutting-edge powder handling solutions that drive industrial progress.