

Working Principle and Features of a Bin Pump Powder Handling System
Bin pump powder handling systems are advanced industrial solutions designed to efficiently transport bulk powders over long distances with precision and reliability. This article explores the core working principle and key features of such systems, providing insights into their operational mechanisms and advantages in various industrial applications.
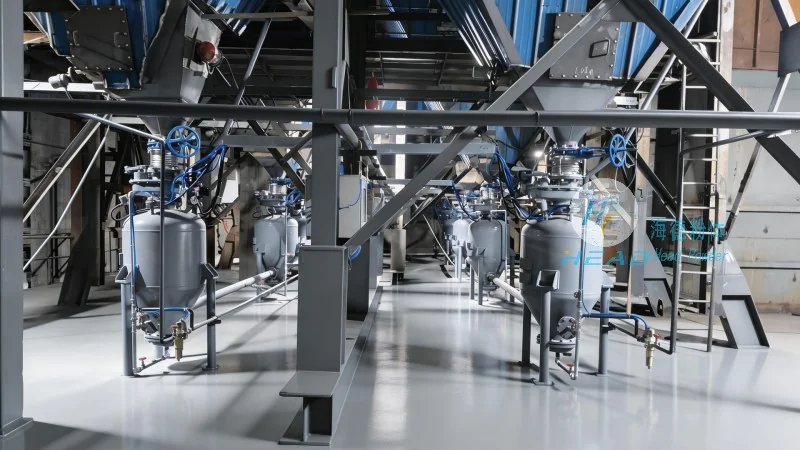
Company Introduction: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of powder handling technology, specializes in developing and supplying high-quality bin pump systems. With a strong commitment to innovation and customer satisfaction, the company has established itself as a trusted partner for industries requiring efficient bulk material transportation solutions. HeadPowder's systems are engineered to meet the diverse needs of sectors like mining, chemical processing, food processing, and more, ensuring optimal performance and durability in demanding environments.
Working Principle of a Bin Pump Powder Handling System
The working principle of a bin pump powder handling system is centered around the use of a hopper and a pump mechanism to create a pressure differential that propels the powder material. The system typically consists of a storage hopper where the bulk powder is stored, a pump chamber that houses the moving parts, and a discharge outlet for the material. When the system is activated, the pump creates a vacuum or pressure inside the chamber, drawing the powder from the hopper into the pump. The pump then uses a rotating or reciprocating action to push the powder through the discharge line to the destination point. This process is continuous and can be controlled to adjust the flow rate and pressure as needed, ensuring precise material delivery.
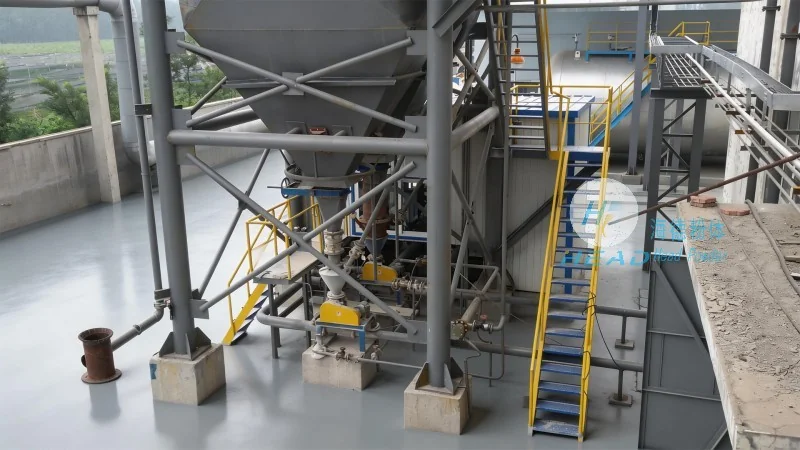
Key Features of Bin Pump Powder Handling Systems
Bin pump systems offer several distinct features that make them ideal for a wide range of industrial applications. One of the primary advantages is their ability to handle abrasive and corrosive powders without causing wear or damage to the system components. The robust construction of the pump and hopper ensures long-term durability, reducing maintenance costs and downtime. Additionally, these systems provide high efficiency in material transportation, with minimal material loss and consistent flow rates. The modular design allows for easy integration into existing production lines, and the adjustable flow control enables precise dosing, which is crucial for processes requiring exact material quantities. Another notable feature is the system's ability to operate in a closed loop, preventing dust emissions and maintaining a clean working environment. This is particularly important in industries where air quality and safety are paramount.
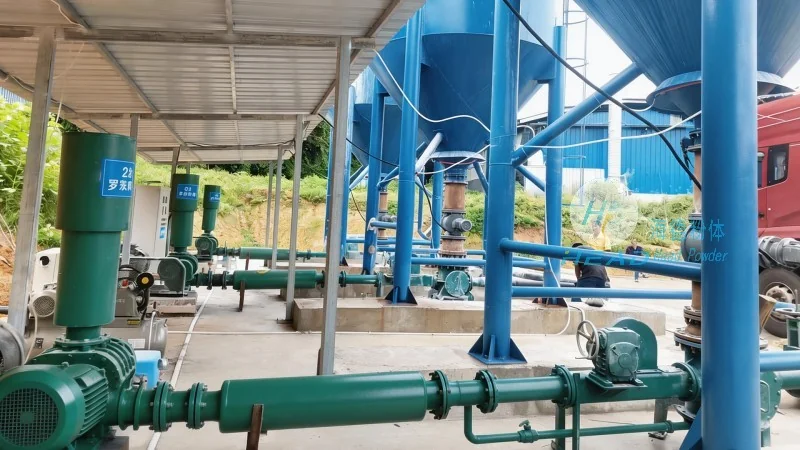
Applications and Benefits in Industrial Settings
Bin pump powder handling systems are widely used in various industries due to their versatility and effectiveness. In the mining industry, they are used to transport ore and other bulk materials from storage bins to processing plants. In chemical processing, these systems handle raw materials and finished products efficiently, ensuring smooth production workflows. The food processing industry benefits from the hygienic design of the systems, which prevents contamination and maintains product quality. The benefits of using bin pump systems include increased productivity, reduced labor costs, and improved safety in the workplace. By automating the powder handling process, industries can achieve higher throughput and lower operational costs, making these systems a valuable investment for long-term operational efficiency.
Conclusion
Bin pump powder handling systems are sophisticated industrial solutions that combine advanced engineering with practical design to meet the demands of modern bulk material transportation. With their reliable working principle and comprehensive features, these systems offer significant advantages over traditional methods, such as pneumatic conveying or belt conveyors. HeadPowder, as a leading manufacturer, continues to innovate and improve its products to provide customers with the best possible solutions for their powder handling needs. By understanding the working principle and features of these systems, industries can make informed decisions to enhance their operational efficiency and achieve their production goals.