

Working Principle and Features of Corn Material Handling System Equipment
At Shandong HeadPowder Engineering Co., Ltd., we specialize in the design, manufacturing, and supply of advanced corn material handling systems. These systems are engineered to efficiently transport, process, and manage corn and other bulk agricultural materials with precision and reliability. Understanding the working principle and key features of such equipment is crucial for optimizing agricultural operations and ensuring consistent performance in grain handling processes.
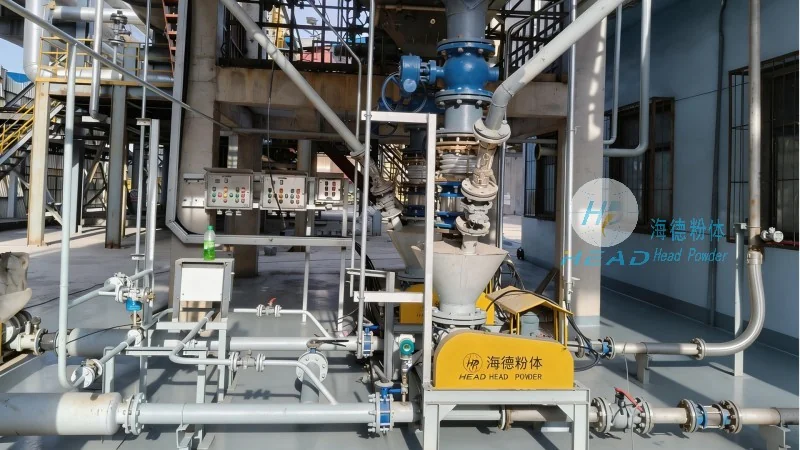
The core working principle of a corn material handling system revolves around the integration of various components, including conveyors, elevators, and storage solutions, to create a seamless material flow. The system typically starts with the reception of raw corn, which may involve unloading from trucks or storage silos. An initial stage of cleaning and sorting may be incorporated to remove impurities and ensure the quality of the material before it proceeds to the next processing step.
Conveyors, such as belt conveyors or screw conveyors, are commonly used to transport corn horizontally or at an incline. Belt conveyors utilize a continuous belt to move materials, offering high capacity and low maintenance. Screw conveyors, on the other hand, use a rotating screw to push materials forward, making them suitable for vertical or inclined transport. These conveyors are often equipped with adjustable speed controls and safety features to adapt to varying material loads and operational conditions.
Elevators, particularly bucket elevators, play a critical role in vertical transport within the system. These elevators consist of a series of buckets attached to a belt or chain that moves vertically, lifting corn from lower to higher levels. The bucket elevator's design allows for efficient vertical movement with minimal energy consumption, making it an essential component for elevating corn to silos or processing units.
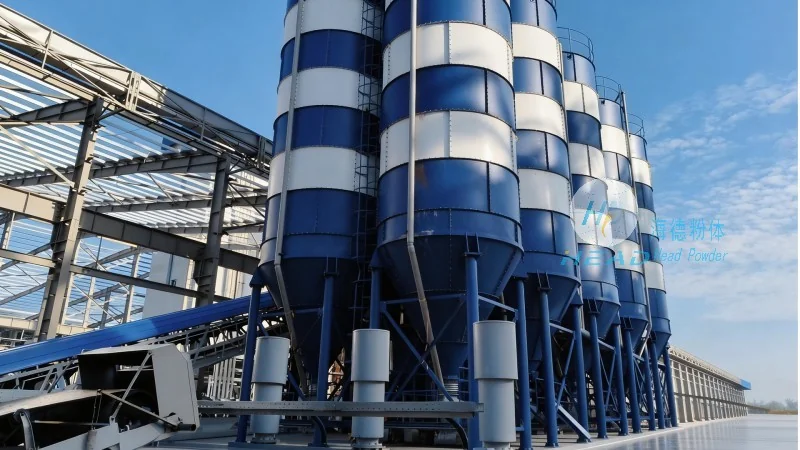
Storage solutions, including grain silos and hopper bins, are integrated into the system to store processed corn. These storage units are constructed with durable materials and equipped with aeration systems to maintain grain quality and prevent spoilage. The silos are typically designed with multiple compartments to facilitate organized storage and easy access for subsequent handling or distribution.
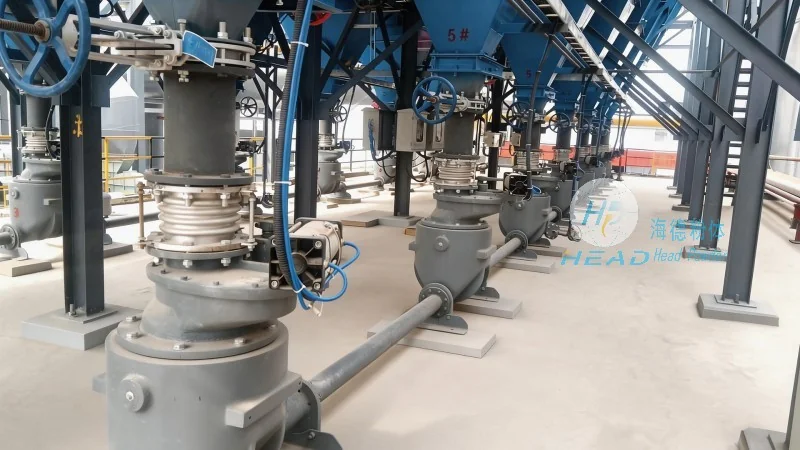
Key features of corn material handling systems include high efficiency, durability, and adaptability. The systems are engineered to handle large volumes of corn with minimal downtime, ensuring smooth operations in agricultural facilities. Advanced control systems, such as PLC (Programmable Logic Controllers), are often incorporated to automate the material flow, allowing for real-time monitoring and adjustment of conveyor speeds and elevator operations.
Another notable feature is the system's modular design, which allows for customization based on specific operational requirements. This modularity enables users to scale the system up or down as needed, accommodating changes in production volume or processing needs. The equipment is also designed with safety in mind, incorporating features like emergency stop buttons, overload protection, and protective guards to prevent accidents and ensure operator safety.
Energy efficiency is a significant consideration in modern corn material handling systems. Manufacturers, like Shandong HeadPowder Engineering Co., Ltd., focus on optimizing energy consumption through the use of efficient motors, variable frequency drives (VFDs), and optimized system layouts. These measures not only reduce operational costs but also contribute to environmental sustainability by minimizing energy waste.
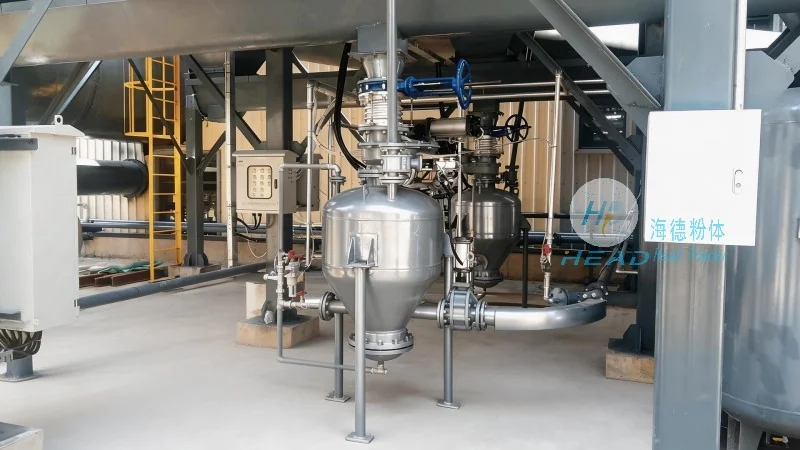
Reliability and maintenance are also critical aspects of the system's design. High-quality materials, such as stainless steel and corrosion-resistant components, are used to ensure long-term durability and resistance to wear and tear. Regular maintenance schedules and user-friendly maintenance procedures are provided to minimize breakdowns and extend the equipment's service life.
In summary, corn material handling systems from Shandong HeadPowder Engineering Co., Ltd. combine advanced technology and robust engineering to provide efficient and reliable solutions for corn processing and storage. The working principle, which integrates conveyors, elevators, and storage units, ensures seamless material flow, while key features like automation, modularity, and energy efficiency enhance operational performance and user experience. These systems are tailored to meet the diverse needs of agricultural operations, supporting the efficient handling of corn and contributing to overall productivity in the grain industry.