

Working Principle and Features of Chicken Essence Material Handling System Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced material handling solutions tailored for the production of chicken essence. Our company, with a strong foundation in engineering and manufacturing, has developed a comprehensive range of equipment designed to optimize the processing and transportation of chicken essence raw materials and finished products. This article will delve into the working principles and key features of our material handling systems, highlighting how they enhance efficiency and reliability in the production line.
Understanding the Working Principle of the Material Handling System
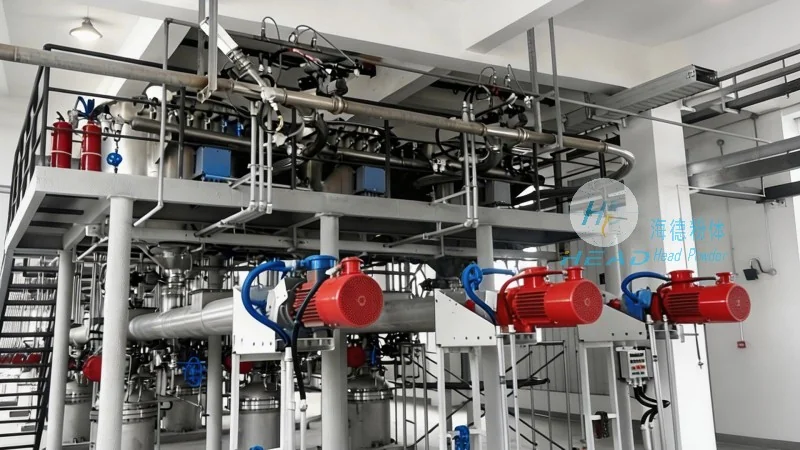
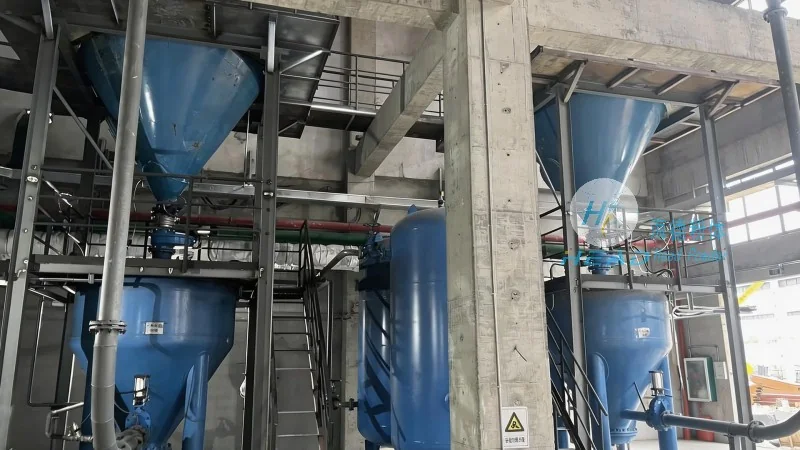
The material handling system for chicken essence production operates through a series of integrated components that work in harmony to ensure smooth material flow. At its core, the system typically includes conveyor belts, pneumatic or mechanical feeders, and control mechanisms that regulate the movement of raw ingredients and finished products. The working principle involves the following key steps: first, raw materials such as chicken extract, seasonings, and other additives are fed into the system via hoppers or bulk containers. Then, the material is transported through a network of conveyors, which may include belt conveyors, screw conveyors, or bucket elevators, depending on the specific application. The system uses sensors and control panels to monitor the flow rate, ensuring consistent and controlled movement. Finally, the processed chicken essence is discharged into storage tanks or packaging lines. This integrated approach minimizes downtime and maximizes throughput, making it an essential component in modern chicken essence production facilities.
Key Features of the Material Handling System Equipment
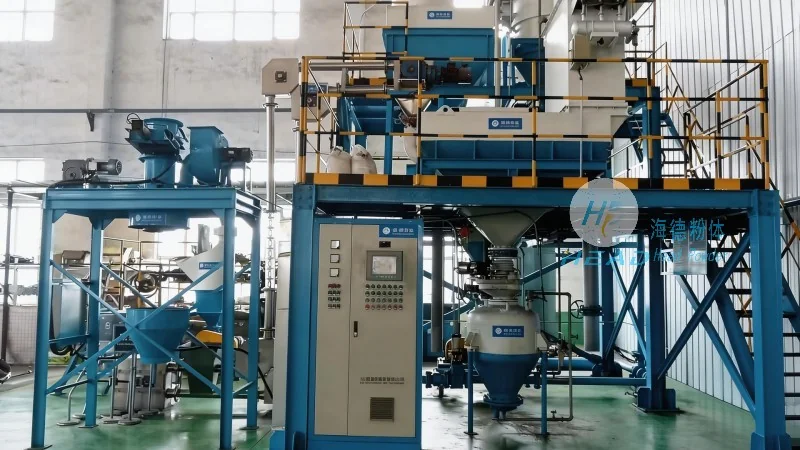
The material handling system equipment from HeadPowder is designed with several notable features that set it apart in the industry. Firstly, the system is built with high-quality materials, such as stainless steel and food-grade components, ensuring compliance with hygiene standards and durability in harsh production environments. Secondly, it offers customizable configurations to accommodate various production scales and product specifications, allowing clients to tailor the system to their specific needs. Thirdly, the system incorporates advanced control technology, including PLC (Programmable Logic Controller) systems and user-friendly interfaces, enabling precise operation and easy maintenance. Additionally, the equipment is equipped with safety features like emergency stop buttons and overload protection, ensuring the safety of operators and preventing equipment damage. These features collectively contribute to improved productivity, reduced operational costs, and enhanced product quality.
Benefits of Implementing the Material Handling System
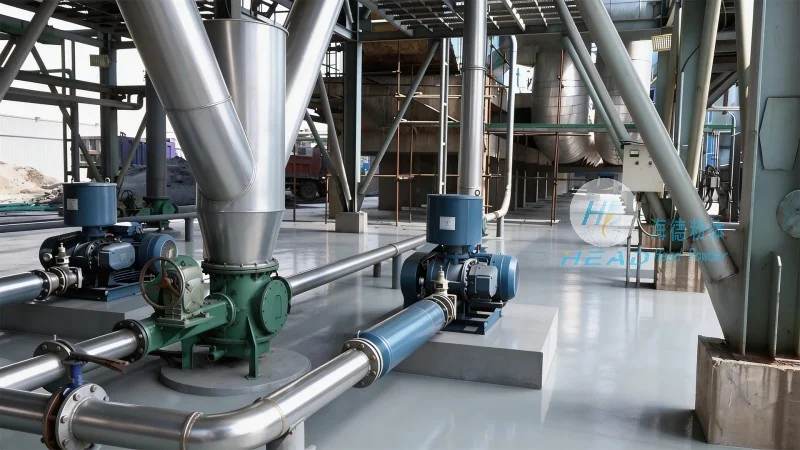
By integrating our material handling system into chicken essence production lines, manufacturers can achieve significant benefits. The system enhances operational efficiency by automating the material transport process, reducing the need for manual labor and minimizing the risk of human error. It also improves product consistency and quality by maintaining consistent flow rates and temperatures, which is crucial for maintaining the flavor and texture of chicken essence. Furthermore, the system reduces downtime and maintenance costs through its robust design and advanced monitoring capabilities. The compact and modular design of the equipment allows for easy installation and integration into existing production facilities, making it a cost-effective solution for both new and existing chicken essence producers. Overall, the implementation of our material handling system can lead to increased productivity, better product quality, and improved overall operational performance.