

Working Principle and Features of Desulfurization Fly Ash Material Handling System Equipment
Desulfurization fly ash, a byproduct of flue gas desulfurization processes in power plants and industrial facilities, requires efficient handling and transportation for disposal or reuse. The HeadPowder Engineering Co., Ltd., based in Shandong, China, has developed advanced material handling systems tailored to manage this challenging material. This article explores the working principle and key features of their desulfurization fly ash material handling system equipment, providing insights into how these systems enhance operational efficiency and safety in ash management.
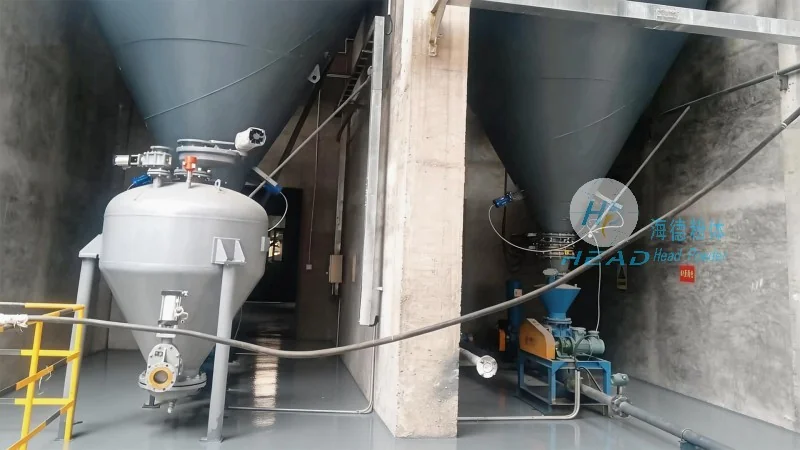
Working Principle of the Desulfurization Fly Ash Material Handling System
The desulfurization fly ash material handling system by HeadPowder Engineering Co., Ltd. operates on a comprehensive mechanism designed to handle the unique properties of fly ash, such as its fine particle size, moisture content, and potential for dust generation. The system typically comprises several integrated components, including feeders, conveyors, and control units, working in tandem to ensure seamless material flow from the ash collection point to the disposal or processing site. The working principle involves the following key steps:
First, the ash is collected from the desulfurization unit and delivered to the system's hopper or storage silo. A feeder, often a rotary or vibratory type, then regulates the ash flow into the conveyor system. The conveyor, which may be a belt or screw conveyor depending on the application, transports the ash through the system with minimal loss of material. Advanced control systems monitor the flow rate, pressure, and other parameters to maintain optimal operation. The entire process is designed to minimize dust emissions and ensure the safe handling of the material, adhering to environmental and safety standards.
Key Features of the Desulfurization Fly Ash Material Handling System
The desulfurization fly ash material handling system from HeadPowder Engineering Co., Ltd. is characterized by several features that set it apart in the industry. These features are tailored to address the specific challenges of fly ash handling, including high moisture content, abrasive properties, and the need for dust control. Some of the key features include:
1. Adaptive Feeding Technology: The system utilizes advanced feeding mechanisms, such as variable-speed feeders, to adjust the ash flow rate based on real-time conditions. This ensures consistent material handling and prevents overloading or underloading of the conveyor, which can lead to system inefficiencies or damage.
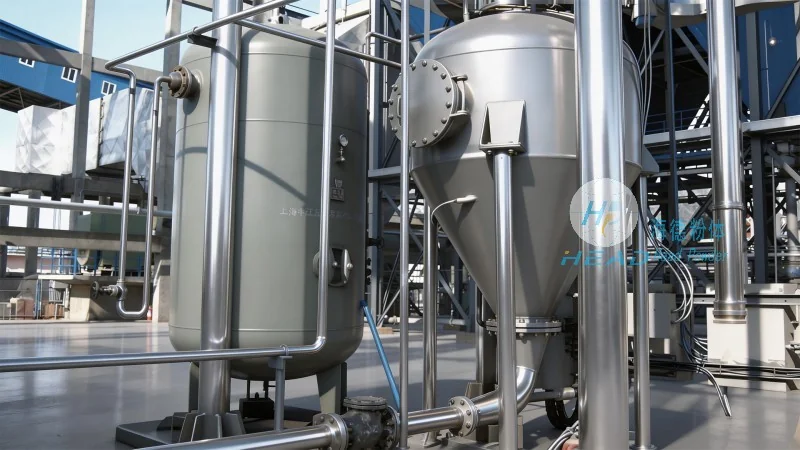
2. Dust Suppression and Collection: To comply with environmental regulations and maintain a safe working environment, the system incorporates effective dust suppression and collection measures. This may include enclosed conveyor sections, air filtration systems, and wet dust control methods, reducing airborne particulate matter and minimizing health risks for operators.
3. Corrosion-Resistant Construction: Given the chemical and abrasive nature of desulfurization fly ash, the system is constructed with corrosion-resistant materials, such as stainless steel or specialized coatings. This ensures long-term durability and reduces maintenance costs, as the equipment can withstand the harsh conditions of ash handling.
4. Modular Design for Flexibility: The system is designed with modular components, allowing for easy integration with existing infrastructure and scalability to accommodate varying ash volumes. This flexibility enables power plants and industrial facilities to adapt the system to their specific needs, whether for small-scale or large-scale ash management.
5. Advanced Monitoring and Control: Integrated sensors and control systems provide real-time monitoring of key parameters, including flow rate, temperature, and pressure. This allows for proactive maintenance and immediate response to any operational issues, enhancing system reliability and reducing downtime.
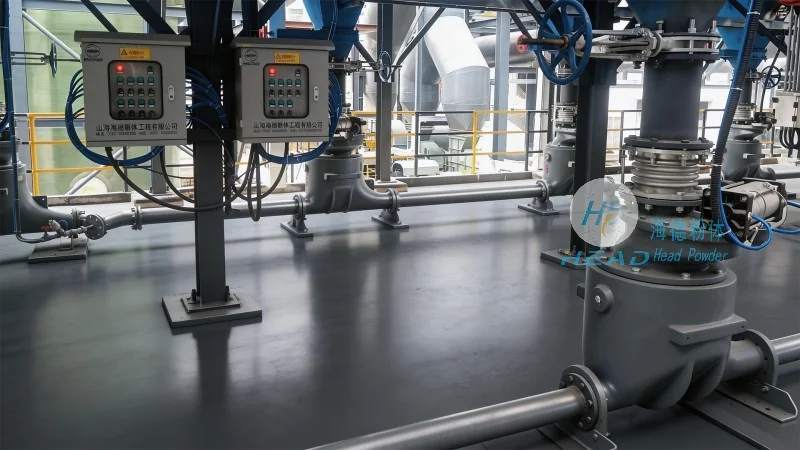
Benefits of Implementing the Desulfurization Fly Ash Material Handling System
The adoption of the desulfurization fly ash material handling system by HeadPowder Engineering Co., Ltd. offers numerous benefits to power plants and industrial facilities. These benefits extend beyond mere material transport and contribute to overall operational efficiency and environmental compliance. Some of the key advantages include:
1. Enhanced Safety and Environmental Compliance: By minimizing dust emissions and controlling the handling process, the system helps facilities meet environmental regulations and maintain a safe working environment. This reduces the risk of health hazards for operators and avoids potential fines or penalties for non-compliance.
2. Improved Operational Efficiency: The adaptive feeding and advanced control systems ensure consistent material flow, reducing downtime and increasing the overall throughput of the ash handling process. This leads to higher productivity and lower operational costs.
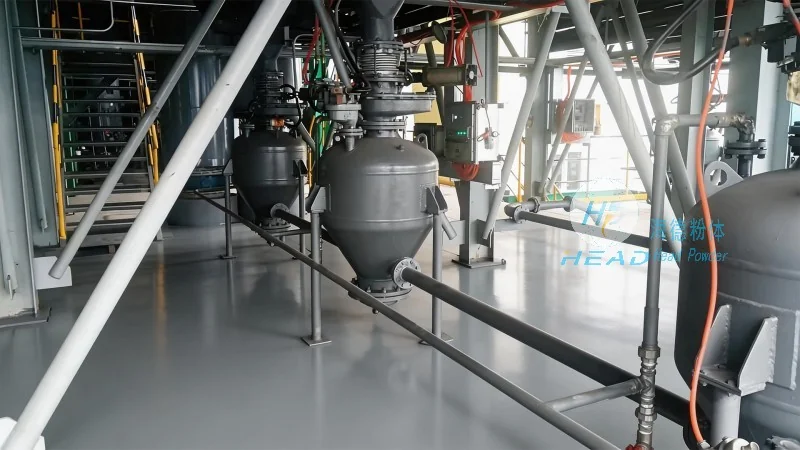
3. Long-Term Durability and Low Maintenance: The corrosion-resistant construction and modular design of the system contribute to its long service life and lower maintenance requirements. This results in significant cost savings over the system's operational lifespan.
4. Scalability and Adaptability: The modular nature of the system allows for easy expansion or modification to accommodate changes in ash volume or processing requirements. This flexibility ensures that the system remains effective as facilities grow or their needs evolve.
5. Reliability and Reduced Downtime: The advanced monitoring and control features enable proactive maintenance and quick resolution of any issues, minimizing system downtime and ensuring continuous operation. This reliability is crucial for maintaining the efficiency of the overall power plant or industrial facility.
Conclusion
The desulfurization fly ash material handling system from HeadPowder Engineering Co., Ltd. represents a sophisticated solution for the efficient and safe management of desulfurization fly ash. By integrating advanced technology and robust design, the system addresses the unique challenges of fly ash handling while offering numerous benefits to power plants and industrial facilities. With its focus on operational efficiency, environmental compliance, and long-term durability, this system is an essential component for modern ash management, helping facilities meet their environmental responsibilities and maintain optimal performance.